
Smart Insight, Smart Control
Delivering Intelligent Solutions for Water and Industrial Systems
From deep wells to pipelines and wastewater treatment, Norite delivers efficiency, durability, and trust in every drop.
- 5-Year Warranty
- ISO 9001 Certified
- 24/7 Support


Flowmeter
High Accuracy & Bi-directional Measurement
Utilizes advanced dual-frequency excitation technology with a measurement accuracy of ±0.2% ±0.3m/s, delivering outstanding performance even at low flow rates and supporting du
Underground Installation – No Measuring Well Required
Equipped with IP68 protection, the sensor can be installed underground without constructing a measuring well, significantly reducing civil engineering costs.
Compatible with Multiple Pipe Connection Standards
Supports various international flange standards including JIS 10K/20K, ANSI 150/300, and DIN PN10/PN16 for wide application compatibility.
Multi-functional Integration for Cold & Hot Water Measurement
Capable of measuring both cold and hot water, ideal for heating systems, HVAC return flow, and other mixed-temperature applications.
Smart Diagnostics & Built-in Ground Electrode
Features built-in grounding electrode (no need for grounding ring) and smart self-diagnosis for real-time operational monitoring and alerts.
Need custom specifications? Our engineers are ready to help.
Call: +86 15090163952 | Email: lisa@noritesolution.com
Proven Results That Drive Your Bottom Line
Real performance data from our Valve installations across critical industries worldwide

100% Pressure Tested
Tested under Class A sealing standard, across 10,000+ units.

20+ Years Lifespan
Proven performance in seawater, wastewater, and high-pressure pipelines.

8,000+ Valves Installed
Including power plants, municipal water systems, and industrial zones.

99.5% On-Time Delivery
Backed by lean production and strict QC.
Certifications & Standards


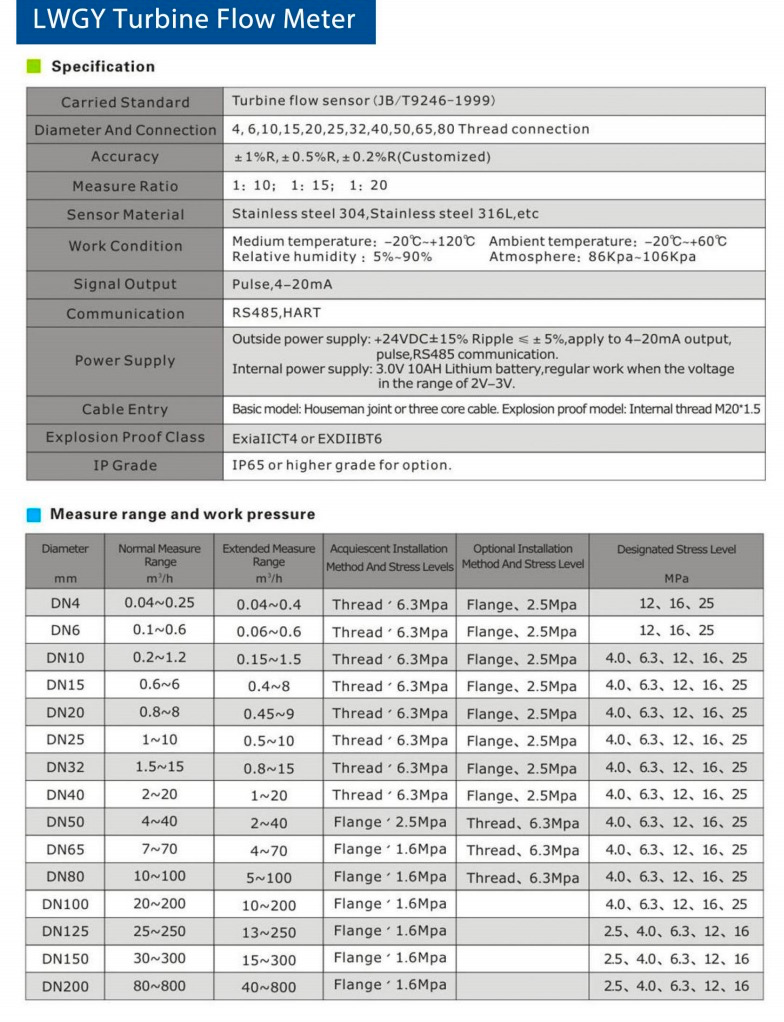
Technical Specifications
Engineered for optimal performance across a wide range of industrial applications
Product types:
Accuracy:
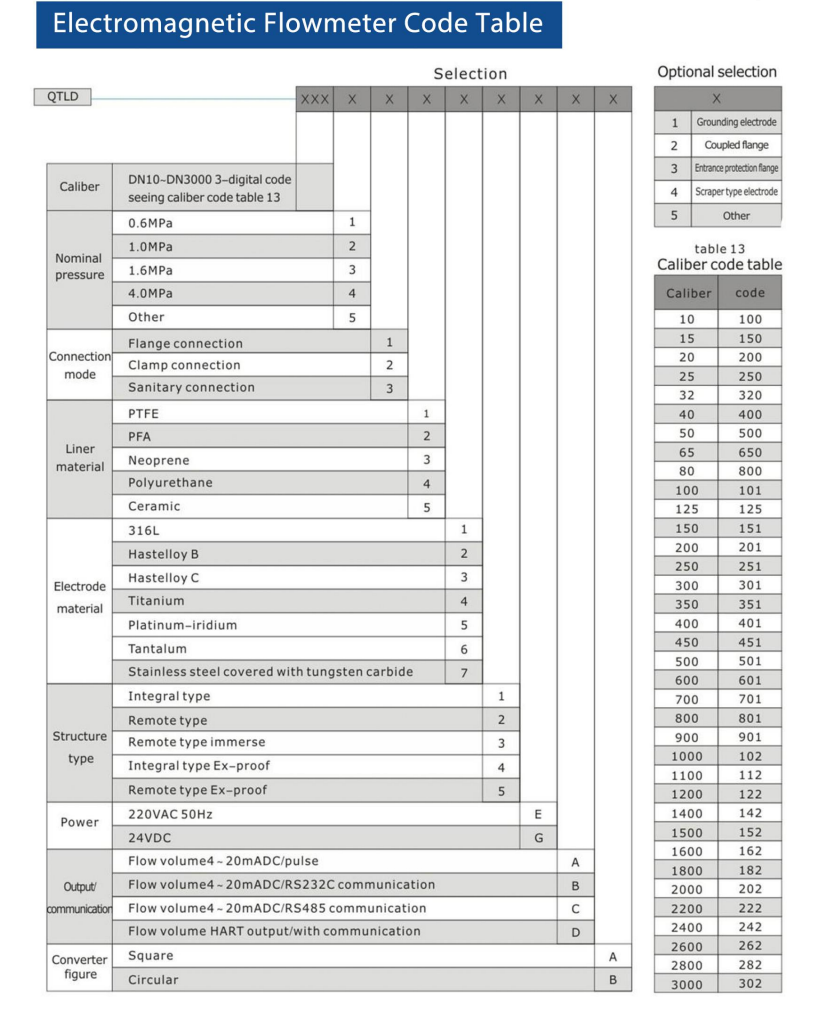
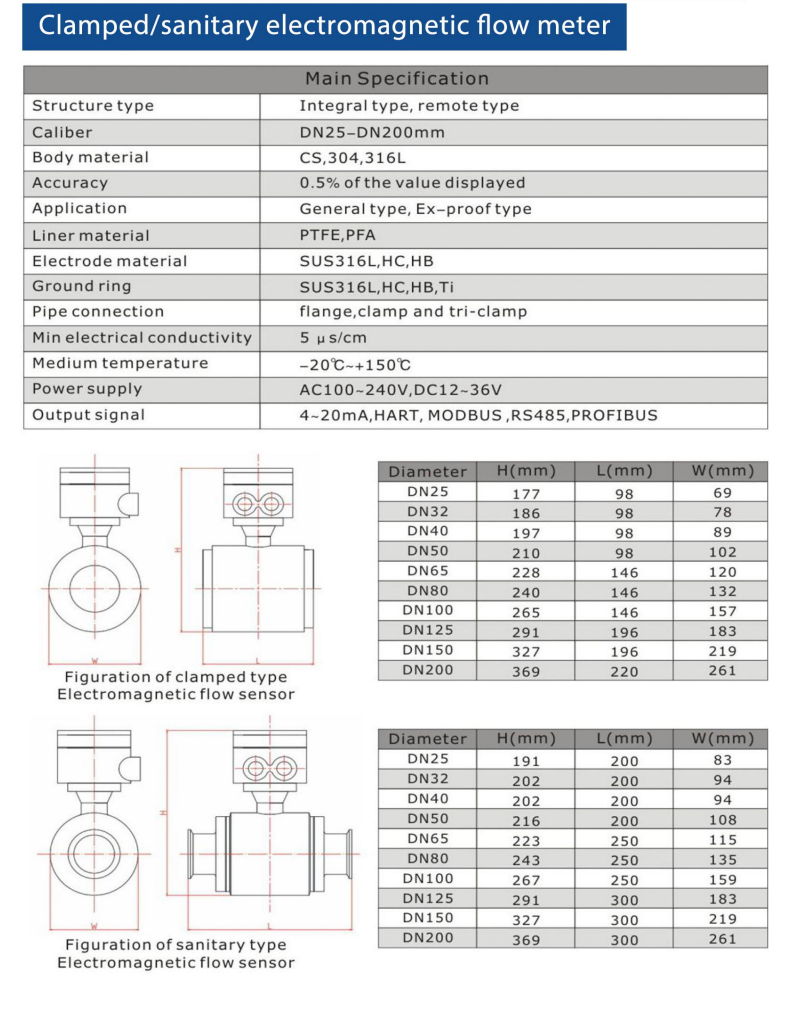
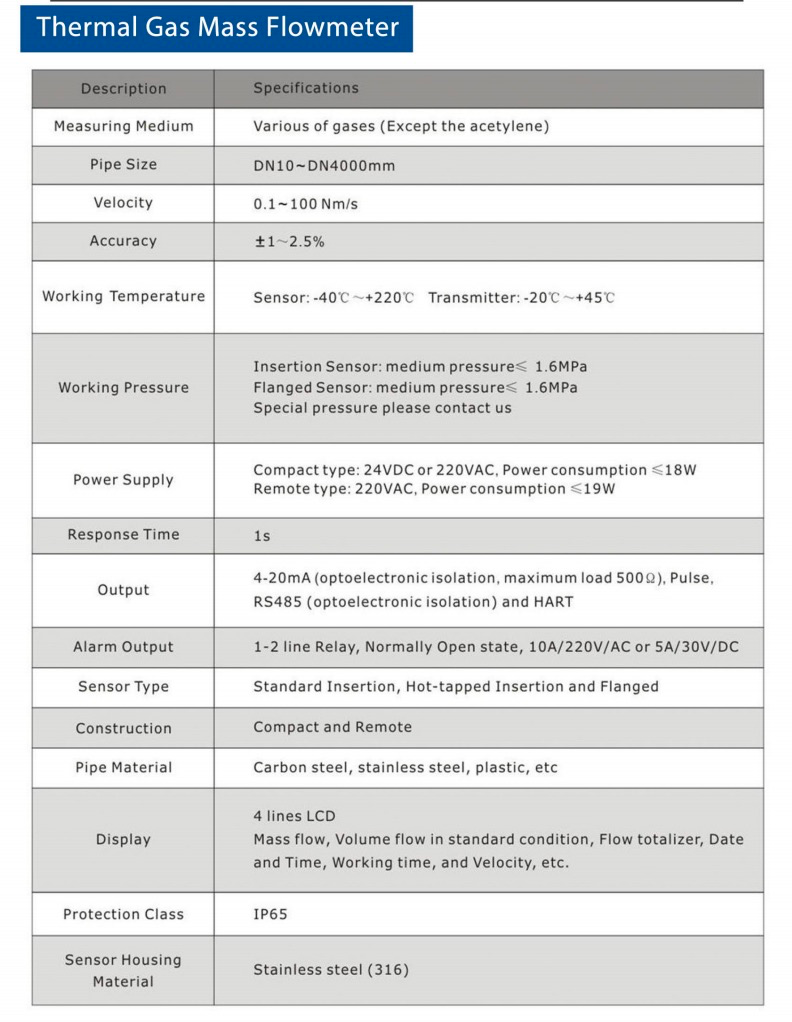
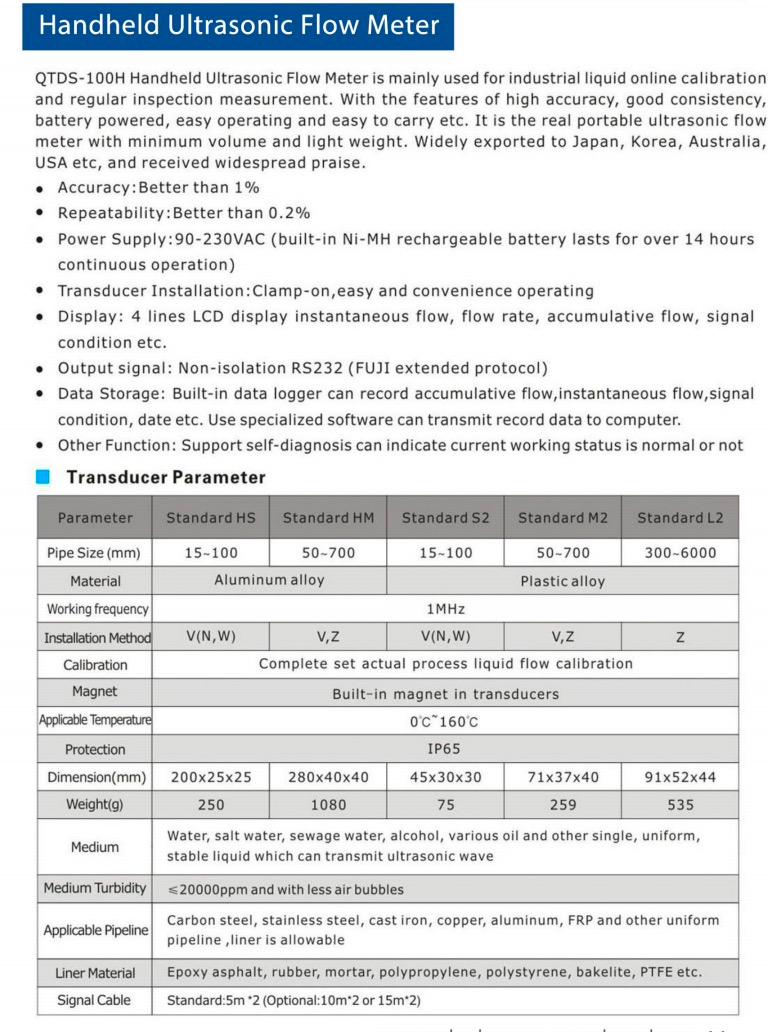
Electromagnetic, vortex, turbine, ultrasonic, elliptical gear, thermal gas
±0.2%,±0.5%
Size:
Applicable medium:
Water, gas, oil products, chemical media
Connection methods:
Temperature:
flange, threaded, quick-install, insert type, clamping type
Shell material:
Lining material:
Ductile iron,WCB,SS304,SS316
EPDM/PTFE
Color:
Communication interface:
Color can be change on body and cover.
4-20MA,Pulse input,RS485 modbus,Hart,GPRS
Power supply mode:
Certifications:
DC24V,AC110C,AC220V, Battery-powered
- Data sheets of various types of flowmeters

Testing Process
From raw materials to finished products, NORITE maintains 100% testing coverage, ensuring that every valve and pump you receive is built to last — safe, stable, and globally certified.

Pressure Testing
Each valve undergoes rigorous pressure and hydrostatic testing prior to shipment to verify body strength, sealing integrity, and pressure stability—ensuring zero leakage and long-term reliability in field operation.

Torque and Functional Testing
Confirming operating performance and precision.

Cycle Life Testing
Simulating long-term use under real working conditions.

Coating & Corrosion Resistance Testing
Validating surface protection and durability.
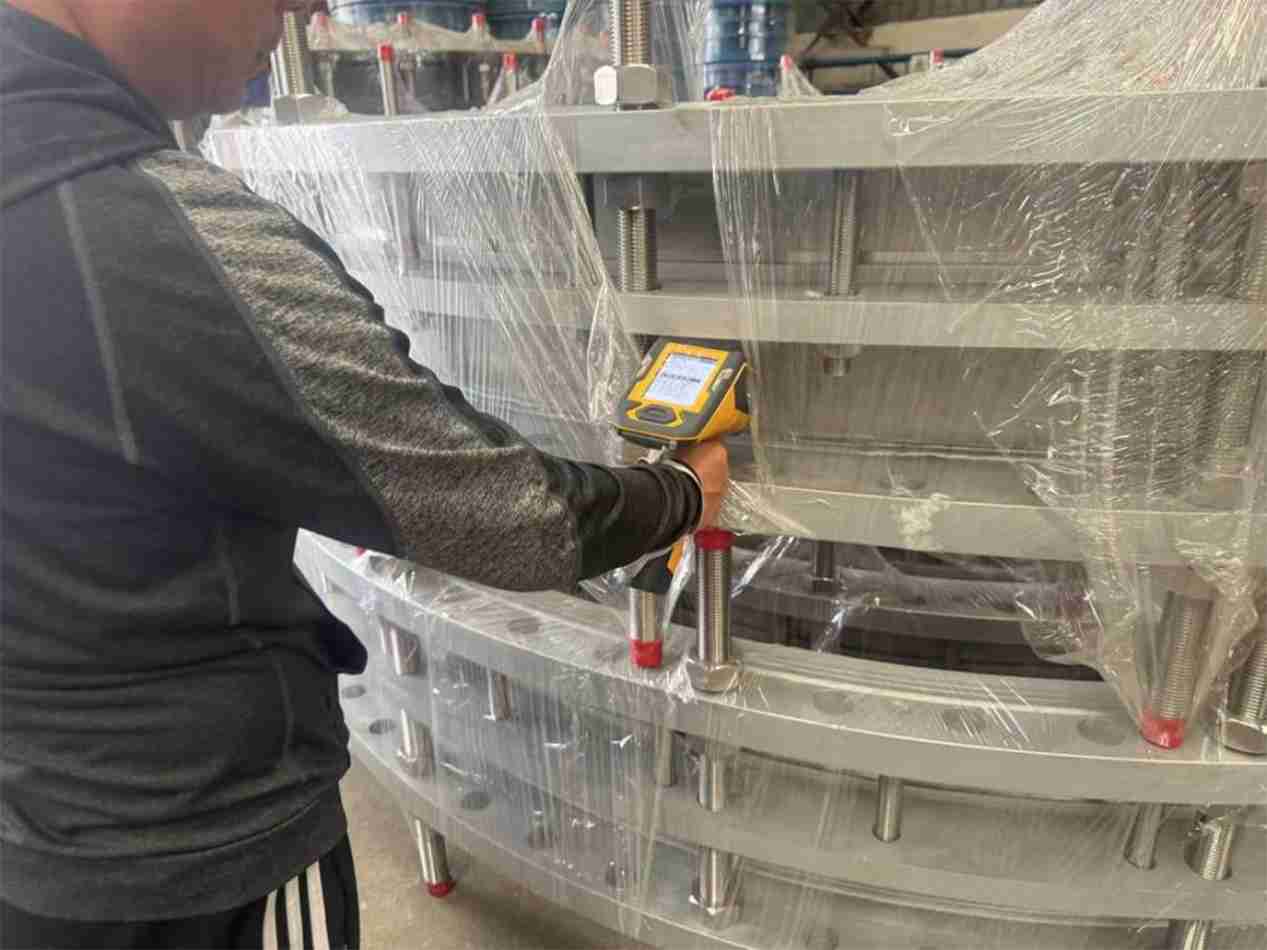
Dimensional & Material Analysis
Using spectrometers and coordinate measuring machines (CMM) for accuracy.
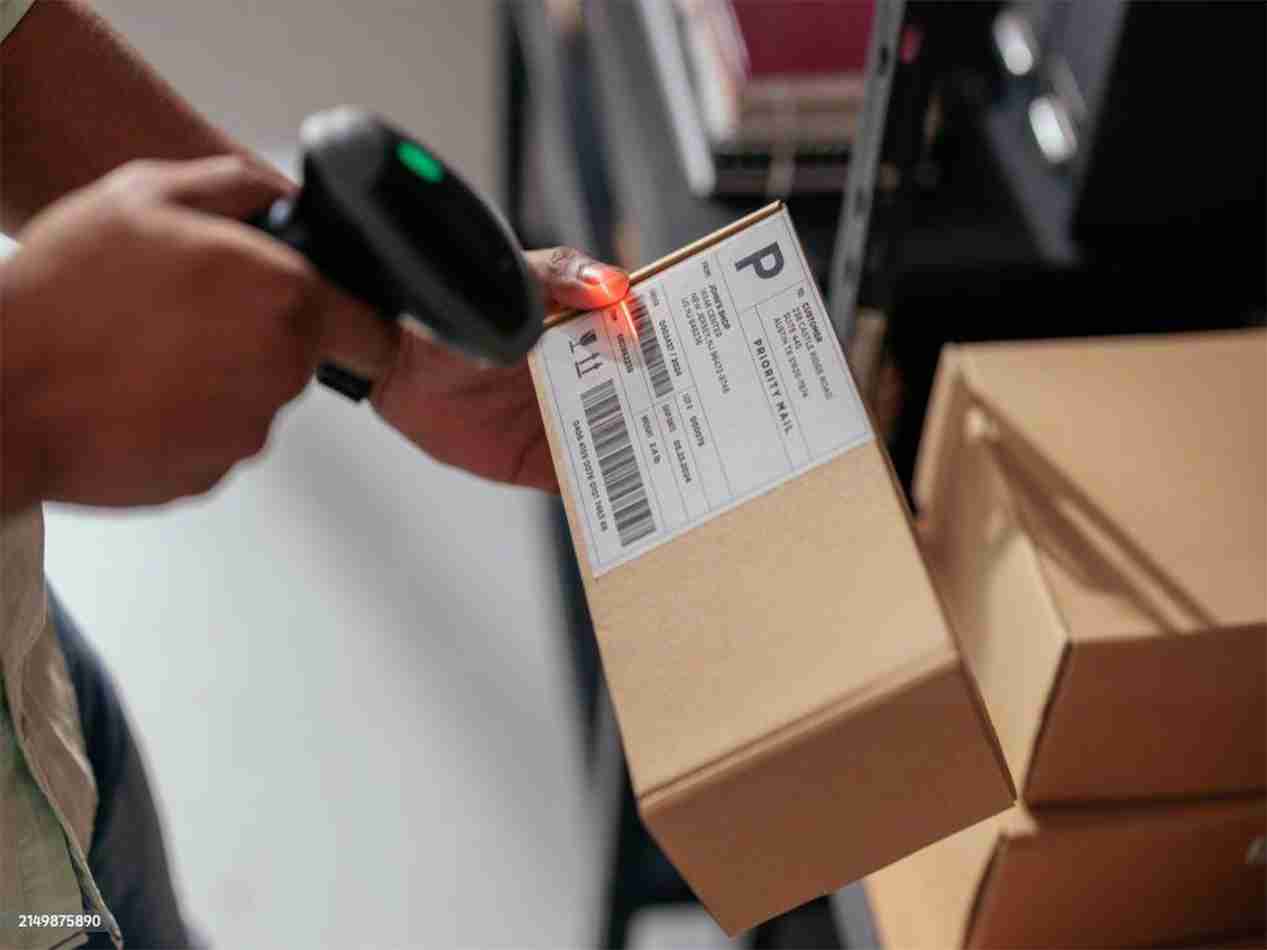
Traceability - Unique product code
Each product leaving our factory is accompanied by a full inspection report and a unique serial number, enabling full traceability and lifetime quality tracking.
Real Project Cases
Proven performance in critical applications worldwide – see our valves in action
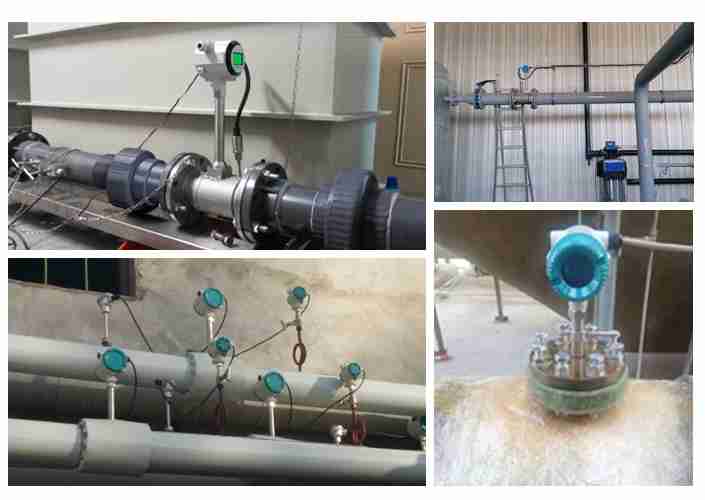
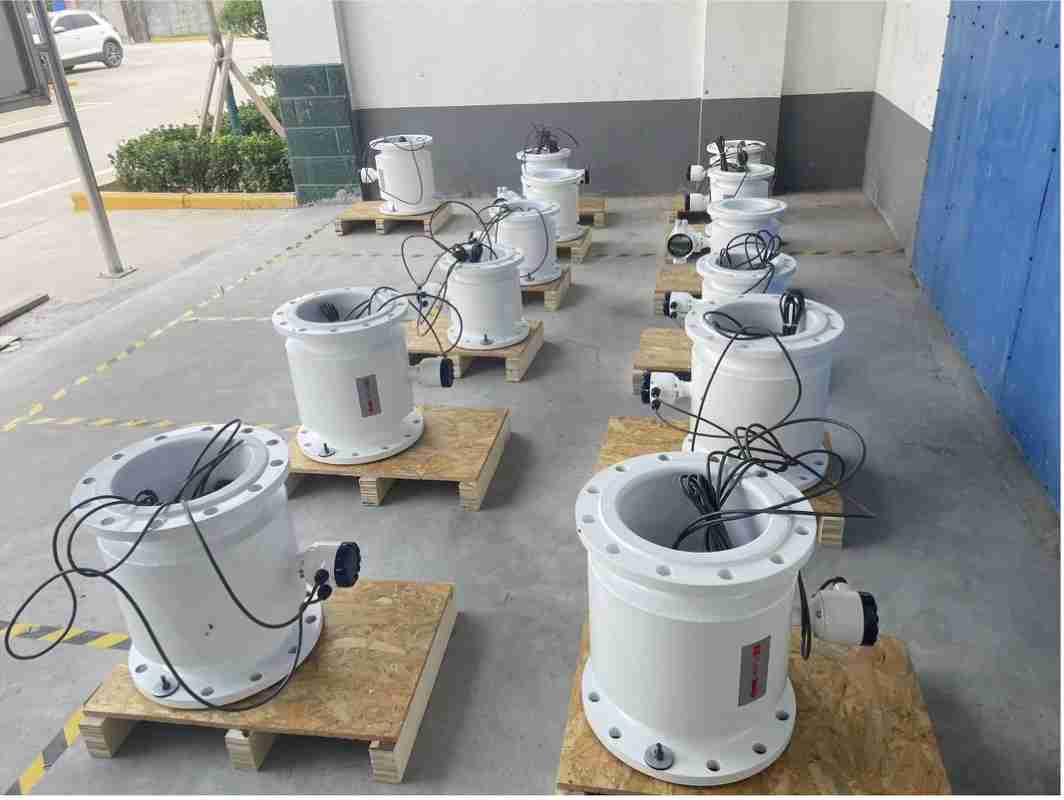
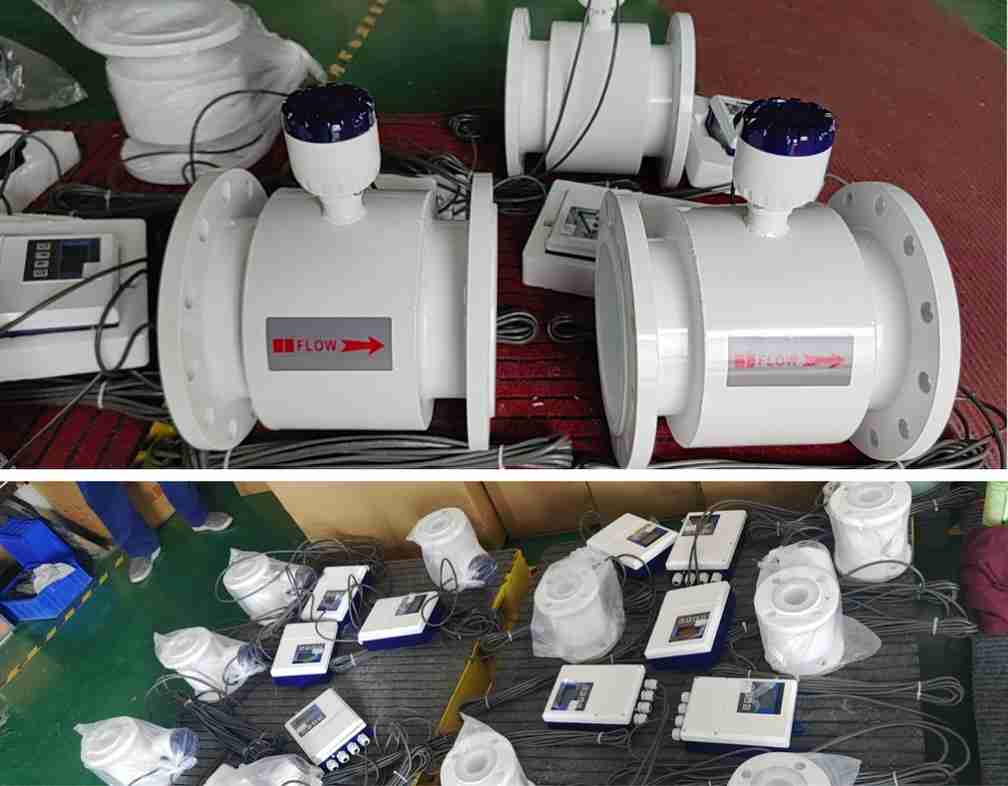
Samuda Chemical Complex Expansion
Project Owner: Samuda Chemical Complex Limited
- Working conditions/Challenges:
These products offer outstanding chemical resistance, tight sealing, and thermal stability—making them ideal for the demanding environments of chlor-alkali and hydrogen peroxide production. They ensure safe, efficient, and long-term operation under highly corrosive conditions.
- The type of equipment adopted:
We provided this factory with a complete set of fluorine-lined valves and flow meters
Achievements/advantages: During the selection phase, our engineering team worked closely with the client to analyze their process media and operating conditions. We delivered tailored, cost-effective flow control solutions backed by a robust supply chain—helping the customer achieve both cost efficiency and operational safety
Get Your Custom Quote
Our technical experts will analyze your requirements and provide a tailored solution with detailed specifications and competitive pricing.