
Flow Control, Zero Compromise
From municipal water to industrial flow systems — total reliability starts here.
From deep wells to pipelines and wastewater treatment, Norite delivers efficiency, durability, and trust in every drop.
- 5-Year Warranty
- ISO 9001 Certified
- 24/7 Support


F8020 Pressure Reducing Valve
Dual-Guided Stem for Extended Service Life
Top and seat ring guided stem and diaphragm design ensures precise operation and longer lifespan.
In-Line Maintenance Friendly
Designed for easy servicing without removing the valve from the main pipeline, saving time and effort.
Corrosion Resistance for Harsh Environments
All iron components are fusion epoxy coated; stainless steel seat and disc ring resist corrosion for reliable operation in varied water conditions.
Durable Materials with Drip-Tight Performance
Ductile iron body and nylon-reinforced diaphragm provide superior strength and long-term leak-free sealing.
Flexible Pilot Options for Versatile Applications
Compatible with various pilot controls and accessories, including optional V-port or double chamber configurations for tailored performance.
Need custom specifications? Our engineers are ready to help.
Call: +86 15090163952 | Email: lisa@noritesolution.com
Proven Results That Drive Your Bottom Line
Real performance data from our Valve installations across critical industries worldwide

100% Pressure Tested
Tested under Class A sealing standard, across 10,000+ units.

20+ Years Lifespan
Proven performance in seawater, wastewater, and high-pressure pipelines.

8,000+ Valves Installed
Including power plants, municipal water systems, and industrial zones.

99.5% On-Time Delivery
Backed by lean production and strict QC.
Certifications & Standards


Technical Specifications
Engineered for optimal performance across a wide range of industrial applications
Model:
Size Range:
F8020,200X
DN50 – DN1000,2”-40”
Pressure Rating:
Standards:
BS EN 1074-5, ISO 5208, BS EN 12266-1, BS EN 558-1
Media:
Max Temperature:
Water and neutral liquids
Body Material:
Wedge Material:
EN-GJS-500-7 (GGG-50)
Stem Material:
Sealing:
Stainless steel,Bronze, Brass
EPDM / NBR
Connection:
Certifications:
Flanged to EN1092-2,ANSI B16.5,BS4504
- Application Conditions
Municipal Water Supply & Network Pressure Control
In large-scale municipal water systems or secondary supply networks, where upstream pressures are high or fluctuating, this type of valve stabilizes downstream pressure and protects pipelines and downstream devices.
Steam / Hot-Water Systems Pressure Step-Down Control
In steam boilers or hot-water distribution systems, high-pressure steam is often reduced for downstream thermal equipment. The pilot-operated valve enables precise pressure control to ensure safe and efficient heat supply.
Industrial Process Water, Chemical & Oil Systems
Used in industrial process water, chemical or oil systems where high flow capacity and precise pressure regulation are required for system stability.
Fire-fighting Systems & High-Pressure Pipeline Protection
In fire-fighting networks or high-pressure water pipelines, excessive pressure can cause equipment damage or malfunctions. These valves provide pressure reduction to safeguard downstream systems.
Large-Diameter, Variable-Flow Systems
In systems with large diameters and highly variable flows, the pilot-operated design is preferred due to its higher capacity and precision control advantages.
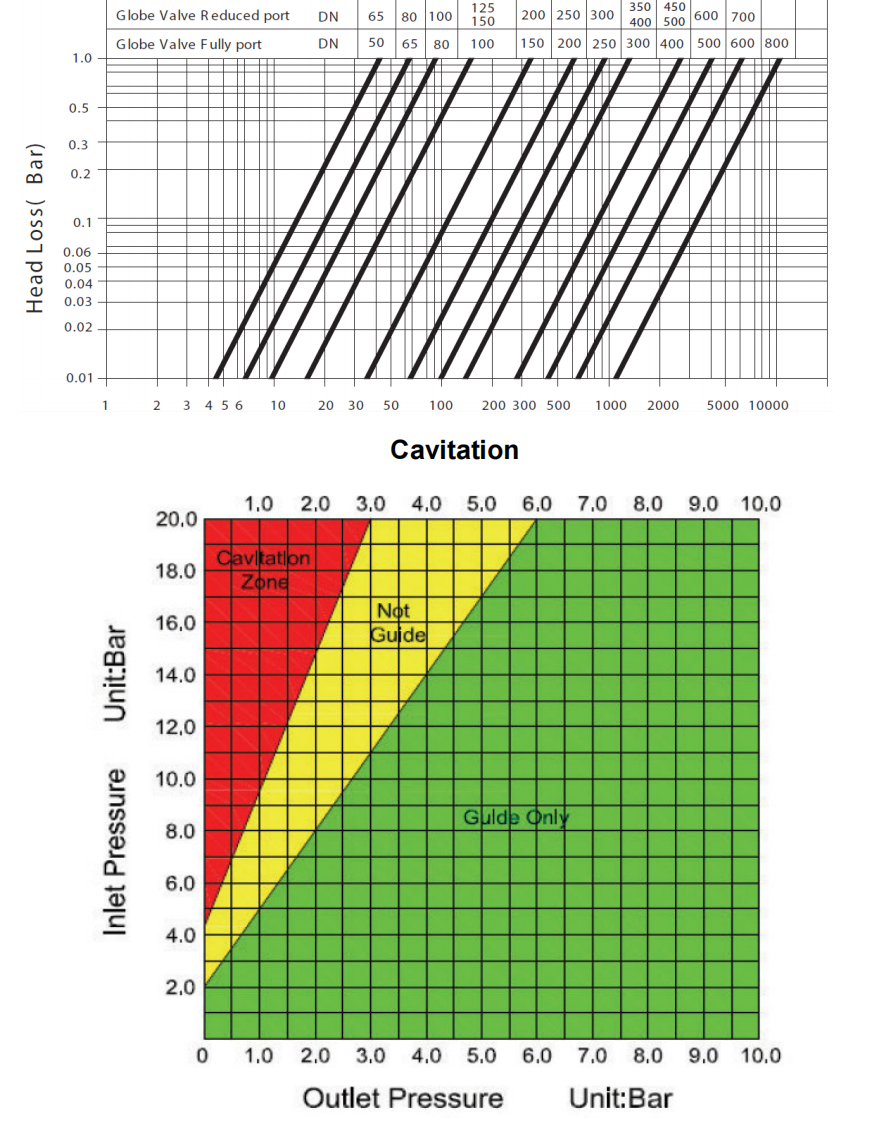
- Valve structure diagram


- Valve size data sheet
Testing Process
From raw materials to finished products, NORITE maintains 100% testing coverage, ensuring that every valve and pump you receive is built to last — safe, stable, and globally certified.

Pressure Testing
Each valve undergoes rigorous pressure and hydrostatic testing prior to shipment to verify body strength, sealing integrity, and pressure stability—ensuring zero leakage and long-term reliability in field operation.

Torque and Functional Testing
Confirming operating performance and precision.

Cycle Life Testing
Simulating long-term use under real working conditions.

Coating & Corrosion Resistance Testing
Validating surface protection and durability.
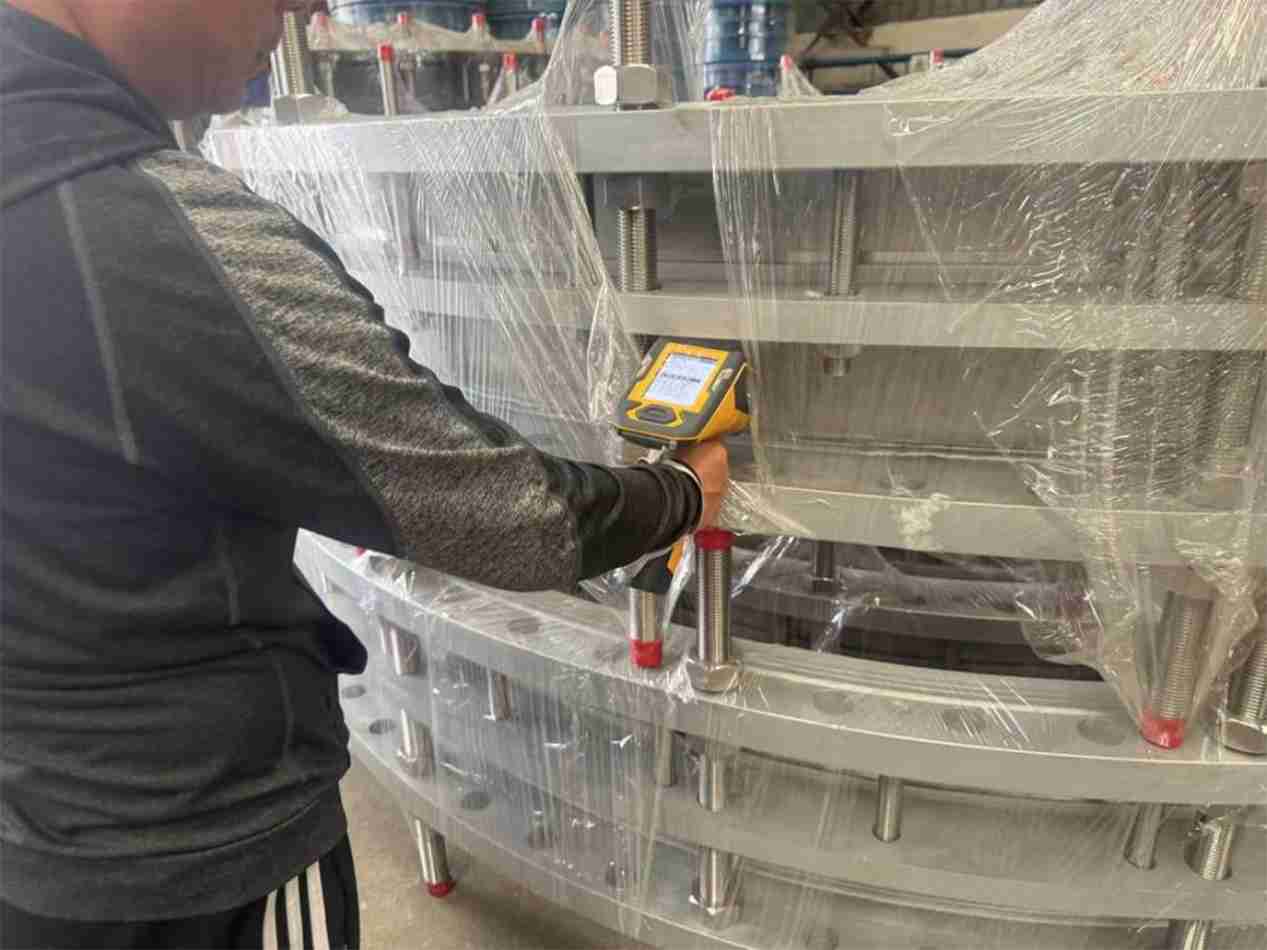
Dimensional & Material Analysis
Using spectrometers and coordinate measuring machines (CMM) for accuracy.
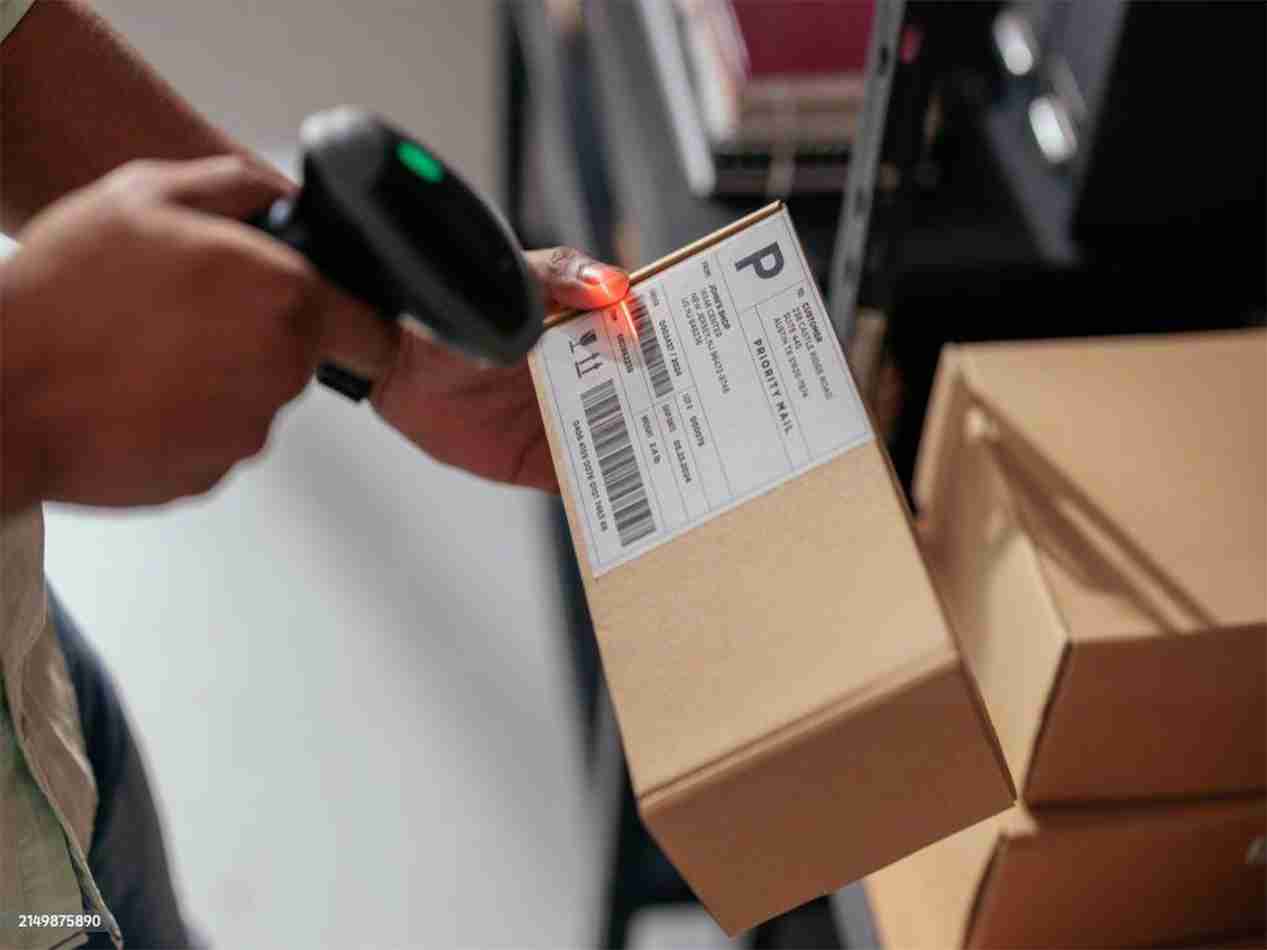
Traceability - Unique product code
Each product leaving our factory is accompanied by a full inspection report and a unique serial number, enabling full traceability and lifetime quality tracking.
Real Project Cases
Proven performance in critical applications worldwide – see our valves in action
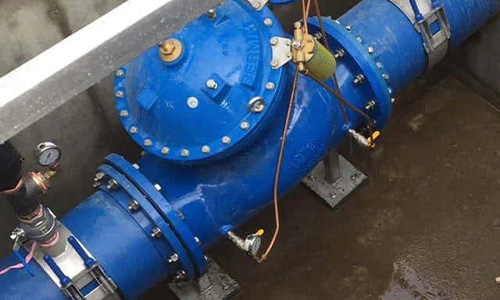
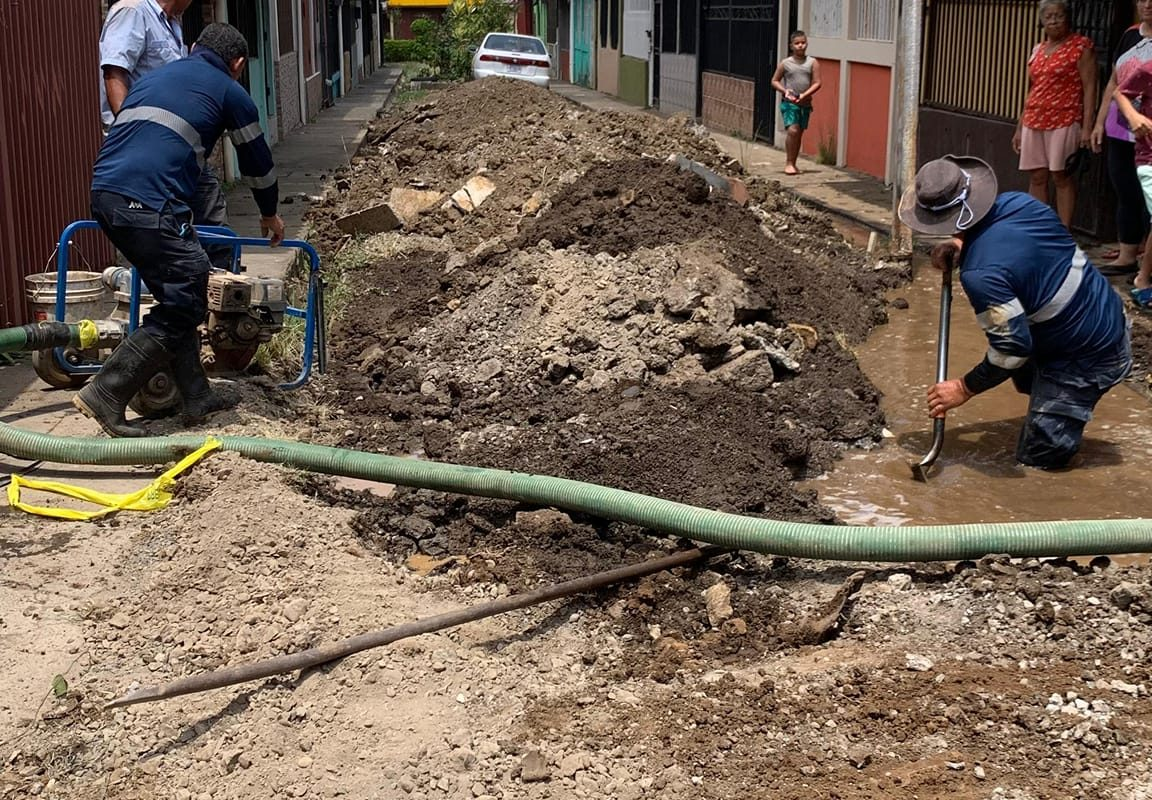
Hydraulically flow-modulated pressure reduction system – Costa Rica
- San Jose, the capital of Costa Rica, the Greater Metropolitan Area and Limon on the Atlantic coast and other places.
Customer/Owner: Costa Rica Water Supply Company
- Working conditions/Challenges:
The main water supply pipeline system in Costa Rica has severe leakage in the water network (long pipeline network, large difference in flow between day and night)
- The type of equipment adopted:
We supplied a 24″/600 mm pilot-operated pressure reducing valve, maintaining downstream pressure from roughly 50 psi at low flow to 60 psi at high flow, effectively reducing the risk of leakage and pipeline rupture.
Key indicators: The installation of the pressure reducing valve can significantly reduce the overflow pressure and leakage in the downstream pipeline network.
Get Your Custom Quote
Our technical experts will analyze your requirements and provide a tailored solution with detailed specifications and competitive pricing.