
Flow Control, Zero Compromise
From municipal water to industrial flow systems — total reliability starts here.
From deep wells to pipelines and wastewater treatment, Norite delivers efficiency, durability, and trust in every drop.
- 5-Year Warranty
- ISO 9001 Certified
- 24/7 Support


Float valve
Automatic Level Control, No External Power Required
The float valve uses a buoyant float to automatically open or close the valve based on liquid level, maintaining stable water level in tanks, reservoirs or water storage systems — without external power or manual intervention.
Simple, Reliable & Compact Design
With minimal moving parts, float valves offer reliable, lowmaintenance service. Their compact design makes them easy to install in various tanks and storage systems.
High Compatibility — Multiple Materials & Media Adaptation
Float valves are available in brass, stainless steel, or plastic materials, allowing adaptation to different water qualities, corrosive media or varying temperature conditions.
Overflow Prevention & Backflow Protection for Safe Operation
By automatically shutting off inflow when the liquid reaches preset level, float valves prevent overflow and backflow — ensuring safety of water storage or supply systems.
Wide Application Range: from Household to Industrial Use
Float valves are versatile — used in domestic water tanks, building supply systems, agricultural irrigation, industrial cooling towers, water treatment storage tanks, rainwater harvesting & more.
Need custom specifications? Our engineers are ready to help.
Call: +86 15090163952 | Email: lisa@noritesolution.com
Proven Results That Drive Your Bottom Line
Real performance data from our Valve installations across critical industries worldwide

100% Pressure Tested
Tested under Class A sealing standard, across 10,000+ units.

20+ Years Lifespan
Proven performance in seawater, wastewater, and high-pressure pipelines.

8,000+ Valves Installed
Including power plants, municipal water systems, and industrial zones.

99.5% On-Time Delivery
Backed by lean production and strict QC.
Certifications & Standards


Technical Specifications
Engineered for optimal performance across a wide range of industrial applications
Model:
Size Range:
100X
DN50 – DN1000,2”-40”
Pressure Rating:
Standards:
BS EN 1074-5, ISO 5208, BS EN 12266-1, BS EN 558-1
Media:
Max Temperature:
Water and neutral liquids
Body Material:
Wedge Material:
EN-GJS-500-7 (GGG-50)
Stem Material:
Sealing:
Stainless steel,Bronze, Brass
EPDM / NBR
Connection:
Certifications:
Flanged to EN1092-2,ANSI B16.5,BS4504
WRAS /ACS Approved for drinking water
- Application Conditions
Residential/commercial building water supply storage/water tank water tower/rainwater collection system
Used for water supply/storage tanks, rooftop reservoirs, or rainwater harvesting systems — auto filling on demand, auto shutoff at set level, preventing overflow or water waste.
Municipal & Agricultural irrigation/rural water conservancy facilities
Suitable for municipal water supply, agricultural irrigation, rural water storage facilities — maintains consistent water level and supply without manual control.
Industrial water storage/cooling/circulation systems/water supply and drainage systems
Used in industrial water storage, cooling towers, circulation systems, water treatment facilities and fire water tanks — ensures stable water level and safe operation.
Sewage treatment/wastewater tank/chemical water tank
Applicable to wastewater treatment tanks, effluent storage, or chemical water storage tanks (with proper material selection) — controls liquid level, prevents overflow and backflow.
Rainwater collection/reclaimed water/environmental protection water conservancy projects
Used in rainwater harvesting systems, recycled water tanks, environmental water management projects — automatically regulates water volume and level, reduces manual operation, enhances automation.
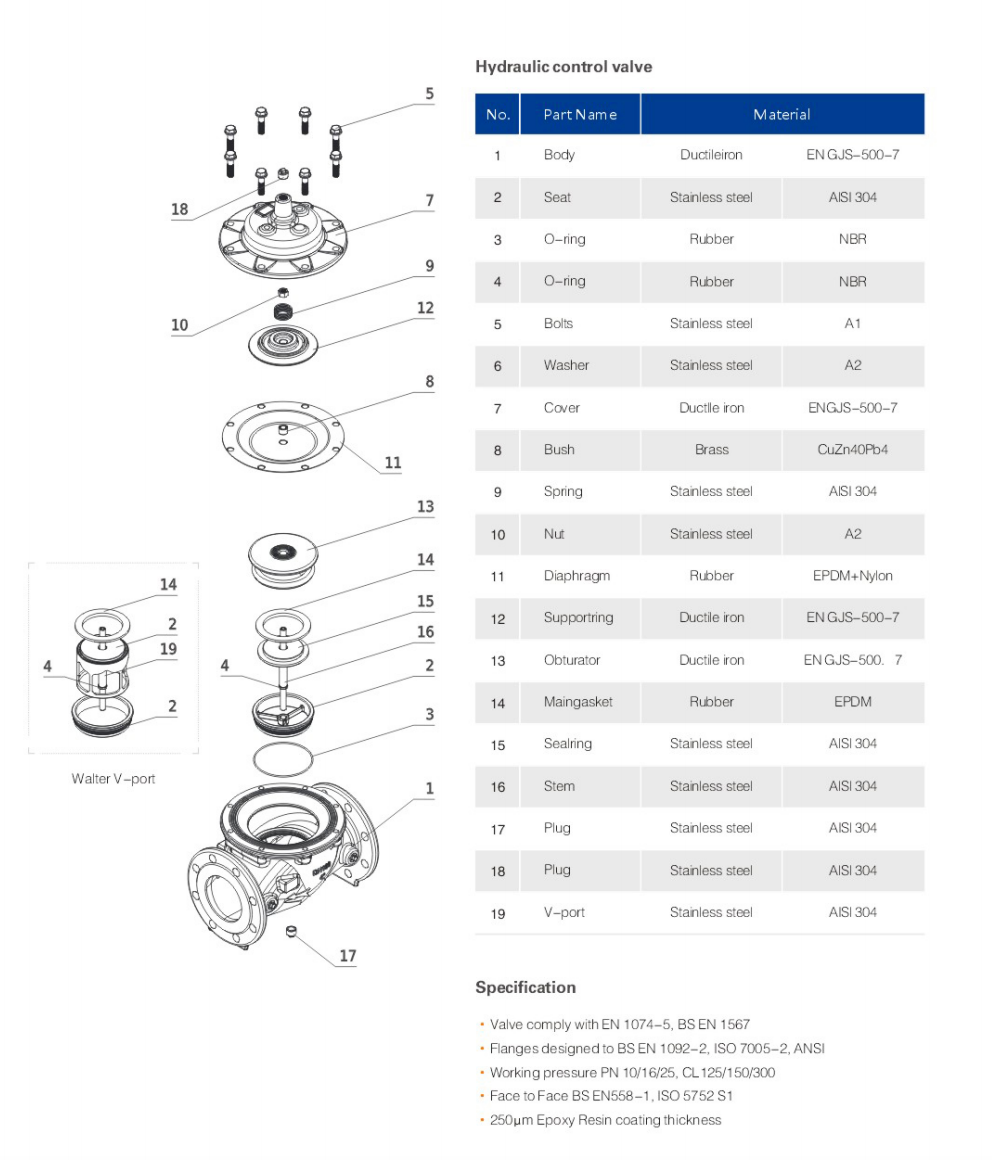
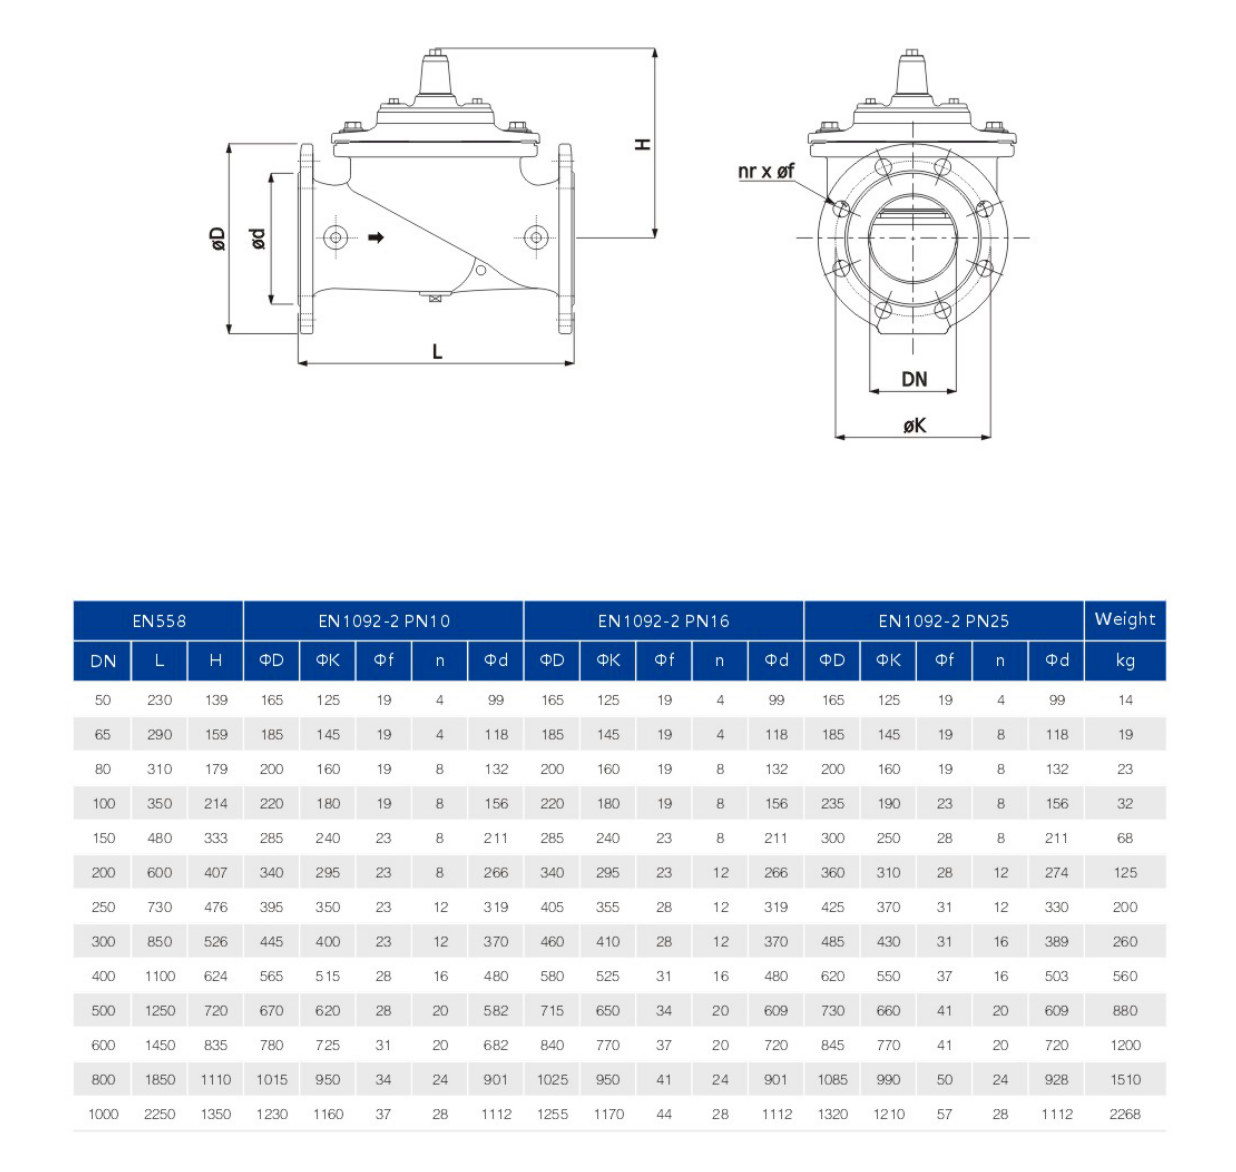
- Valve structure diagram
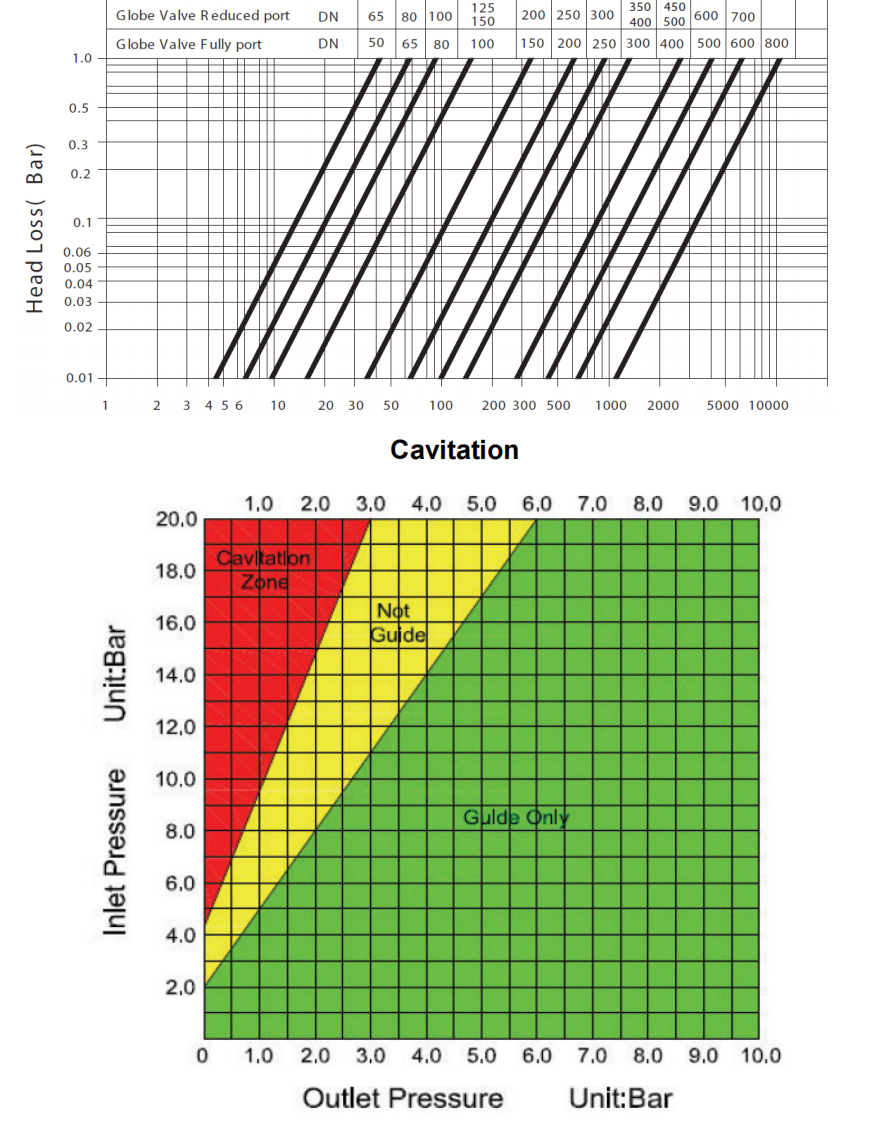
- Valve size data sheet
Testing Process
From raw materials to finished products, NORITE maintains 100% testing coverage, ensuring that every valve and pump you receive is built to last — safe, stable, and globally certified.

Pressure Testing
Each valve undergoes rigorous pressure and hydrostatic testing prior to shipment to verify body strength, sealing integrity, and pressure stability—ensuring zero leakage and long-term reliability in field operation.

Torque and Functional Testing
Confirming operating performance and precision.

Cycle Life Testing
Simulating long-term use under real working conditions.

Coating & Corrosion Resistance Testing
Validating surface protection and durability.
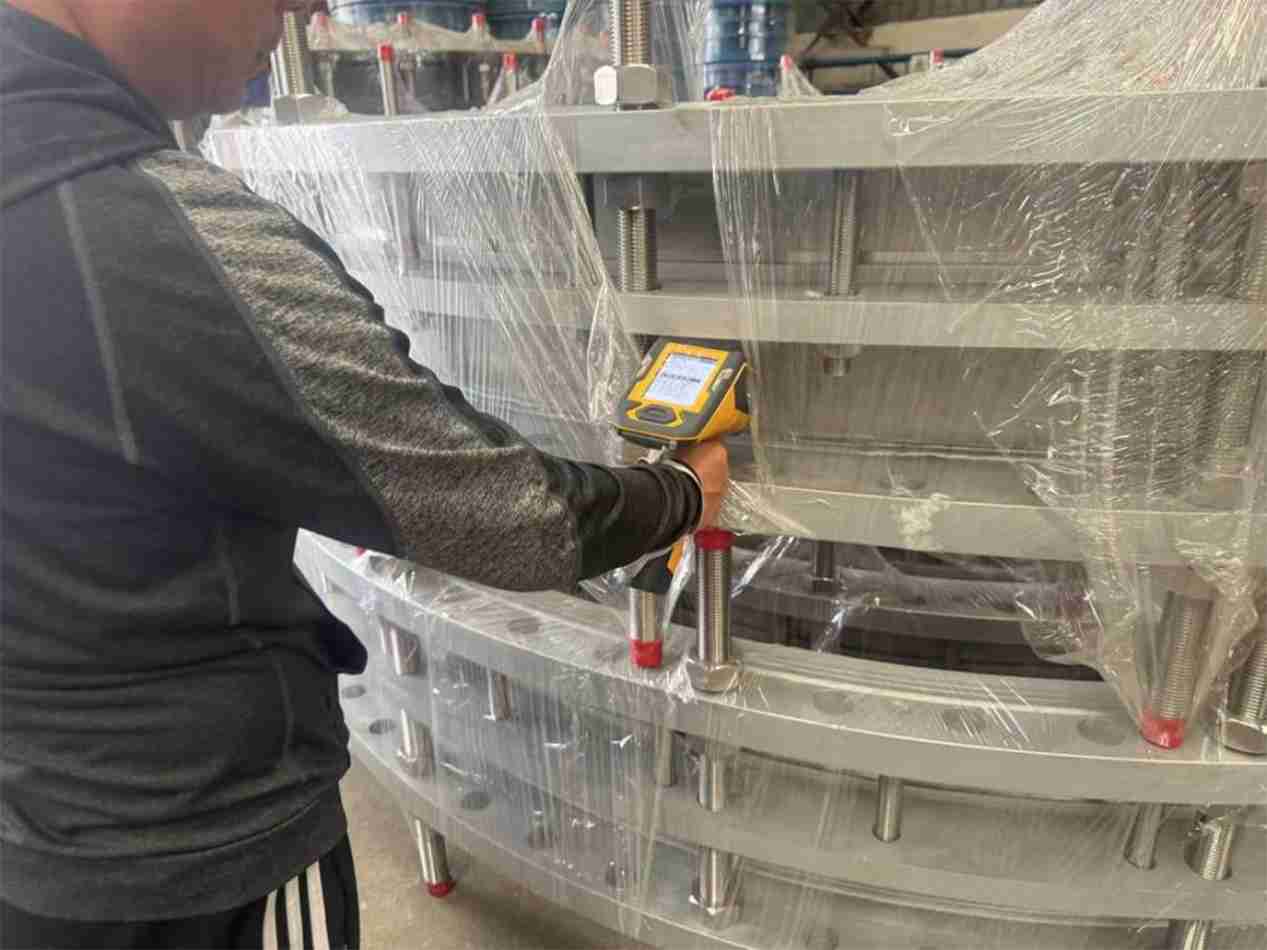
Dimensional & Material Analysis
Using spectrometers and coordinate measuring machines (CMM) for accuracy.
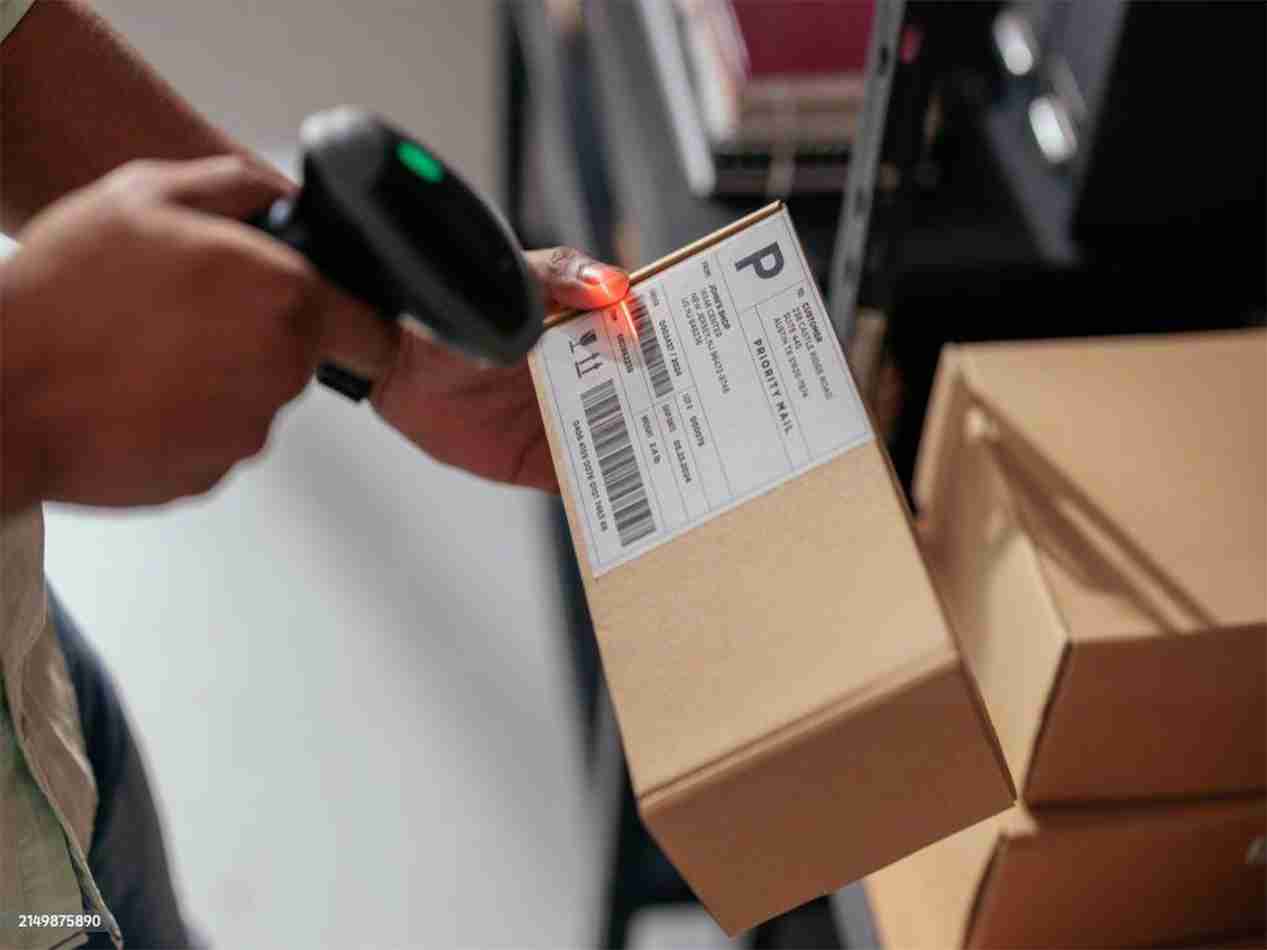
Traceability - Unique product code
Each product leaving our factory is accompanied by a full inspection report and a unique serial number, enabling full traceability and lifetime quality tracking.
Real Project Cases
Proven performance in critical applications worldwide – see our valves in action
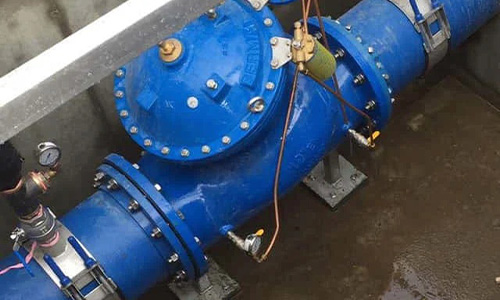
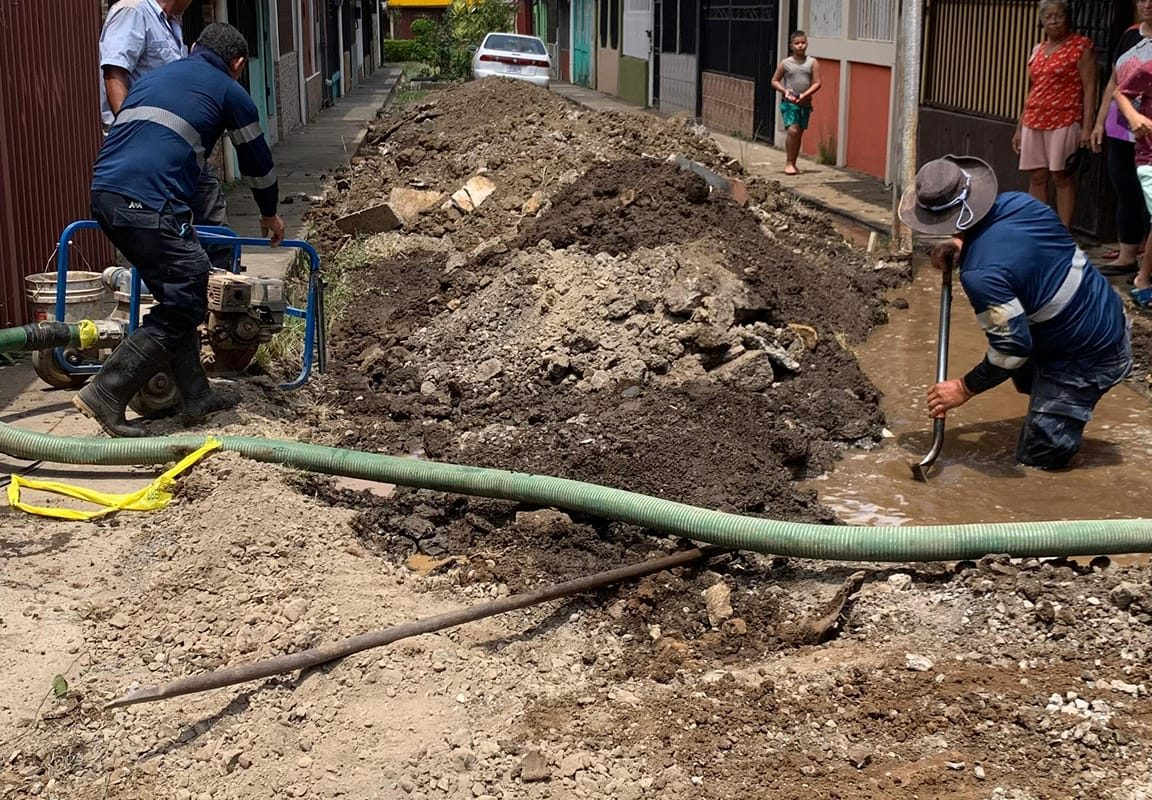
Hydraulically flowmodulated pressure reduction system – Costa Rica
- San Jose, the capital of Costa Rica, the Greater Metropolitan Area and Limon on the Atlantic coast and other places.
Customer/Owner: Costa Rica Water Supply Company
- Working conditions/Challenges:
The main water supply pipeline system in Costa Rica has severe leakage in the water network (long pipeline network, large difference in flow between day and night)
- The type of equipment adopted:
We provided the project party with a 24 “/600 mm pilot-operated pressure reducing valve for pressure management: downstream pressure ranged from approximately 50 psi at low flow rates to approximately 60 psi at high flow rates. To reduce the risk of leakage and pipeline rupture.
Key indicators: The installation of the pressure reducing valve can significantly reduce the overflow pressure and leakage in the downstream pipeline network.
Get Your Custom Quote
Our technical experts will analyze your requirements and provide a tailored solution with detailed specifications and competitive pricing.