
Flow Control, Zero Compromise
From municipal water to industrial flow systems — total reliability starts here.
From deep wells to pipelines and wastewater treatment, Norite delivers efficiency, durability, and trust in every drop.
- 5-Year Warranty
- ISO 9001 Certified
- 24/7 Support


Double Orifice Air Release Valve
High-Capacity Air Discharge & Intake
Rapidly discharges large volumes of air during filling and admits air during emptying or vacuum conditions to prevent pipeline collapse.
Continuous Micro-Air Release
Automatically releases entrapped air under pressure during operation, enhancing flow efficiency and preventing air pockets.
Stable Float Guidance & Reliable Sealing
Float operates smoothly within guide rails, ensuring precise movement and tight sealing. Optional stainless steel float available for harsh conditions.
Corrosion Resistance & Long-Term Durability
All wetted iron components are fusion bonded epoxy coated. No moving parts contact internal coating, ensuring long-term protection and coating integrity.
Full-Bore Body Design for High Flow
Full-bore internal design minimizes flow resistance and supports high-capacity flow requirements in water transmission systems.
Need custom specifications? Our engineers are ready to help.
Call: +86 15090163952 | Email: lisa@noritesolution.com
Proven Results That Drive Your Bottom Line
Real performance data from our Valve installations across critical industries worldwide

100% Pressure Tested
Tested under Class A sealing standard, across 10,000+ units.

20+ Years Lifespan
Proven performance in seawater, wastewater, and high-pressure pipelines.

8,000+ Valves Installed
Including power plants, municipal water systems, and industrial zones.

99.5% On-Time Delivery
Backed by lean production and strict QC.
Certifications & Standards


Technical Specifications
Engineered for optimal performance across a wide range of industrial applications
Model:
Size Range:
DORV
DN50 – DN150,2”-6”
Pressure Rating:
Standards:
EN 1074-4,AWWA C512
Media:
Max Temperature:
ater and neutral liquids
Body Material:
Stem Material:
EN-GJS-500-7 (GGG-50),Carbon steel, stainless steel
Stainless steel,Bronze, Brass
Float Ball:
Sealing:
EPDM / NBR
Connection:
Certifications:
Flanged to EN1092-2,ANSI B16.5,BS4504
- Application Conditions
Municipal Water Supply Systems
Installed on long-distance transmission mains, elevation change zones, and pump station outlets to release or admit air, preventing vacuum damage and water hammer.
Wastewater Treatment & Reclaimed Water Systems
Used in systems prone to gas accumulation, ensuring continuous operation and system stability under low or fluctuating flow conditions.
Agricultural Irrigation & Water Conveyance Projects
Ensures air evacuation in gravity-fed irrigation or canal systems, preventing air lock and maintaining system efficiency.
Desalination & Industrial Water Pipelines
Installed in seawater or corrosive liquid pipelines with anti-corrosion materials for reliable air management.
Hydropower & Water Regulation Projects
Mitigates surge and vibration risks caused by air accumulation in pressure pipelines and surge shafts.
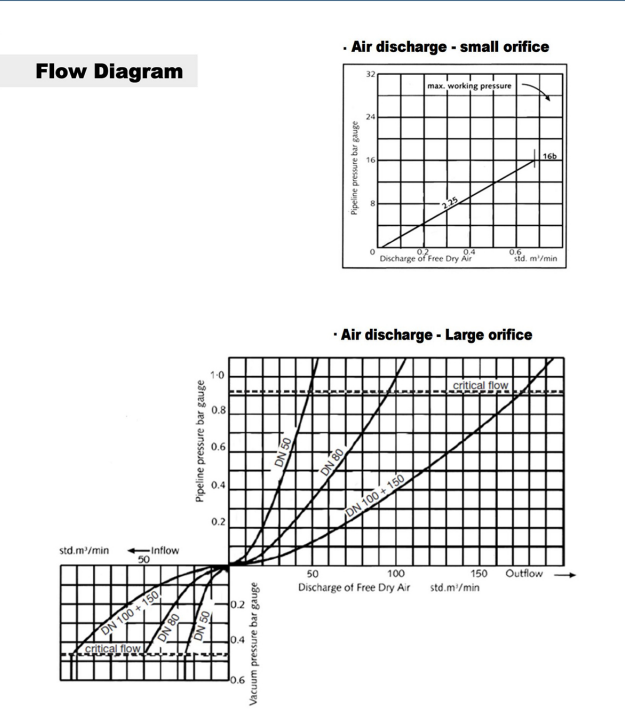
- Size data sheet

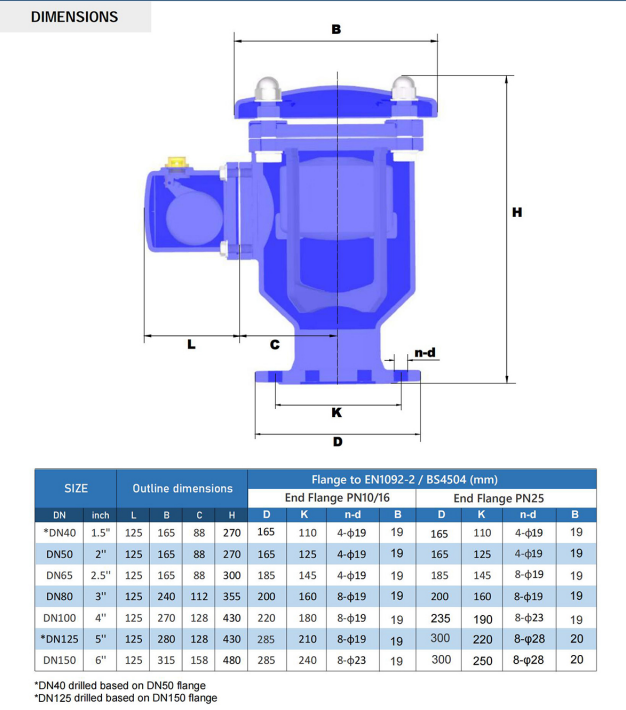
- Size data sheet
Testing Process
From raw materials to finished products, NORITE maintains 100% testing coverage, ensuring that every valve and pump you receive is built to last — safe, stable, and globally certified.

Pressure Testing
Each valve undergoes rigorous pressure and hydrostatic testing prior to shipment to verify body strength, sealing integrity, and pressure stability—ensuring zero leakage and long-term reliability in field operation.

Torque and Functional Testing
Confirming operating performance and precision.

Cycle Life Testing
Simulating long-term use under real working conditions.

Coating & Corrosion Resistance Testing
Validating surface protection and durability.
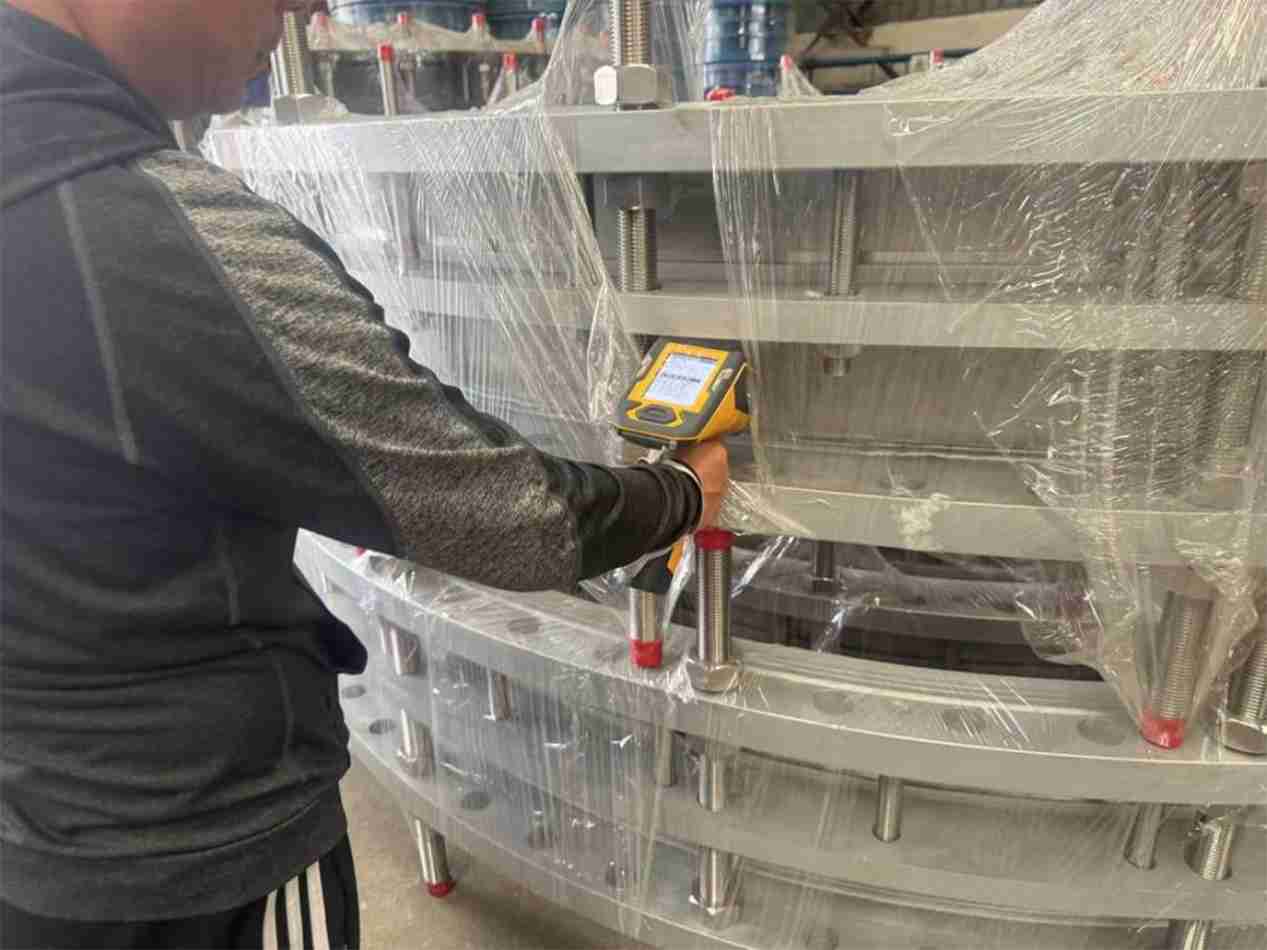
Dimensional & Material Analysis
Using spectrometers and coordinate measuring machines (CMM) for accuracy.
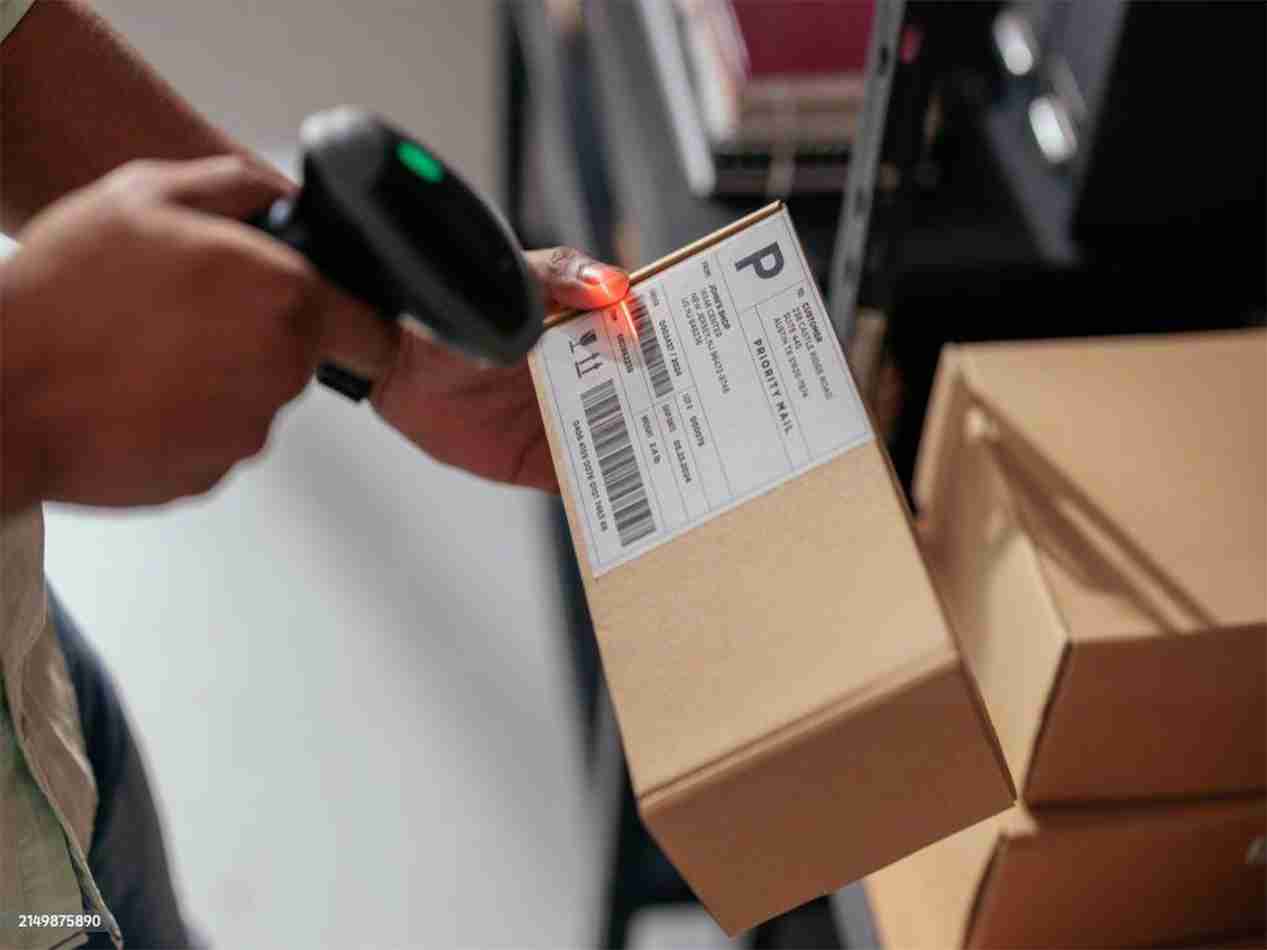
Traceability - Unique product code
Each product leaving our factory is accompanied by a full inspection report and a unique serial number, enabling full traceability and lifetime quality tracking.
Real Project Cases
Proven performance in critical applications worldwide – see our valves in action
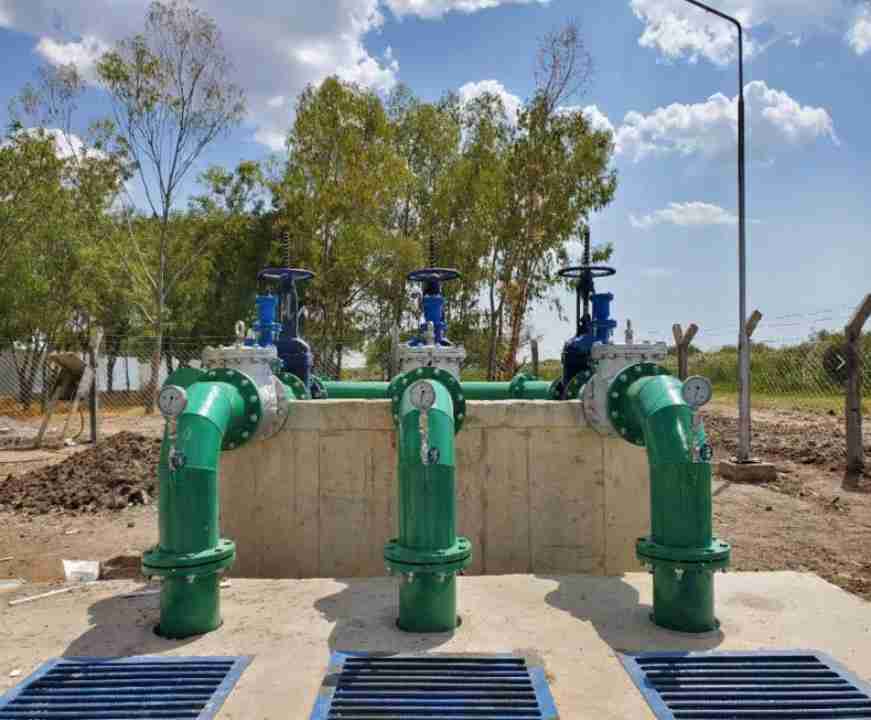
Ecuador Municipal Water Transmission Project
- Quito, Ecuador
- Working conditions/Challenges:
Multiple sets of double orifice air release valves were installed in long-distance pipelines across mountainous regions to ensure stable air management during elevation changes.
- The type of equipment adopted:
Automatic air release valves such as Double Orifice Air Valves are critical in maintaining efficient pipeline operation — releasing entrapped air at high points and admitting air during vacuum conditions, preventing water hammer and ensuring continuous flow.
Get Your Custom Quote
Our technical experts will analyze your requirements and provide a tailored solution with detailed specifications and competitive pricing.