
Flow Control, Zero Compromise
From municipal water to industrial flow systems — total reliability starts here.
From deep wells to pipelines and wastewater treatment, Norite delivers efficiency, durability, and trust in every drop.
- 5-Year Warranty
- ISO 9001 Certified
- 24/7 Support


API Ball Valve
Exceptional Sealing Performance with Anti-Leakage Design
Floating or trunnion-mounted ball with soft or metal seats ensures zero-leakage sealing, even under high-pressure conditions. Fully compliant with API 6D sealing standards.
Low Operating Torque, Ideal for Automation
Compact and responsive design enables low-torque operation, making it highly compatible with electric, pneumatic, or hydraulic actuators.
Fire-Safe and Anti-Static Design
Tested to API 607/API 6FA fire-safe standards and equipped with anti-static devices to prevent ignition from static electricity in flammable systems.
Versatile Seat Options for Diverse Working Conditions
Available with soft-seated and metal-seated options to suit high-temperature, high-pressure, corrosive, or particulate-laden fluids.
API Compliant, Globally Recognized Quality
Fully compliant with API 6D, ASME B16.34, ISO 5211 and other global standards, trusted in oil & gas pipelines, refineries, and power plants worldwide.
Need custom specifications? Our engineers are ready to help.
Call: +86 15090163952 | Email: lisa@noritesolution.com
Proven Results That Drive Your Bottom Line
Real performance data from our Valve installations across critical industries worldwide

100% Pressure Tested
Tested under Class A sealing standard, across 10,000+ units.

20+ Years Lifespan
Proven performance in seawater, wastewater, and high-pressure pipelines.

8,000+ Valves Installed
Including power plants, municipal water systems, and industrial zones.

99.5% On-Time Delivery
Backed by lean production and strict QC.
Certifications & Standards


Technical Specifications
Engineered for optimal performance across a wide range of industrial applications
Model:
Size Range:
Q41F,Q47F,Q341F,
Q347F,Q941F.Q947F
DN15 – DN1200,1/2”-48”
Pressure Rating:
Standards:
150LB- 2500LB
API6D,API608
Media:
Max Temperature:
Water, Oil, Gas
Body Material:
Wedge Material:
A216 GR.WCB, Alloy steel, SS304, SS316
A216 GR.WCB, Alloy steel, SS304, SS316
Stem Material:
Sealing:
Stainless steel
PTFE,PPR,PEEK
Connection:
Certifications:
Flanged to ASME B16.5,ASME B16.47
- Application Conditions
Oil and gas transportation systems
Used in onshore/offshore oil & gas pipelines for flow control, ensuring safe shutoff under high pressure, high temperature, and corrosive environments.
Refinery and chemical process pipeline networks
Ideal for handling aggressive or flammable fluids in refining and chemical plants, where fast shutoff and fire-safe capability are essential.
Steam/cooling water system of power plant
Widely used in thermal and nuclear power plants for controlling steam or cooling water systems.
Municipal and industrial water supply systems
Employed in large-scale water supply and industrial fluid systems for precise and durable flow control.
LNG and Cryogenic medium systems
Designed with cryogenic materials and extended bonnets for safe use in LNG storage and transportation systems.
- Valve structure diagram

600LB/900LB
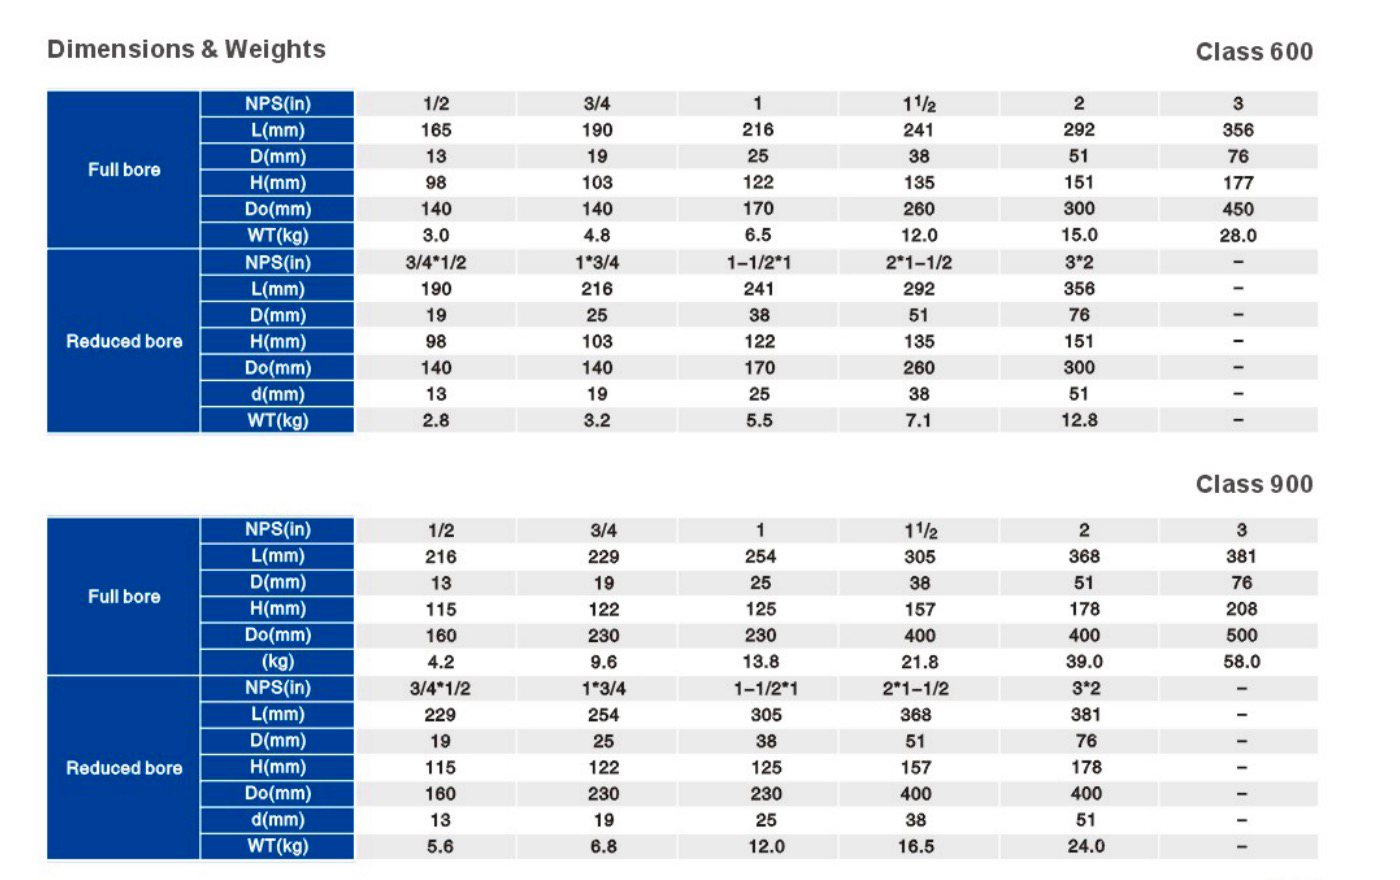
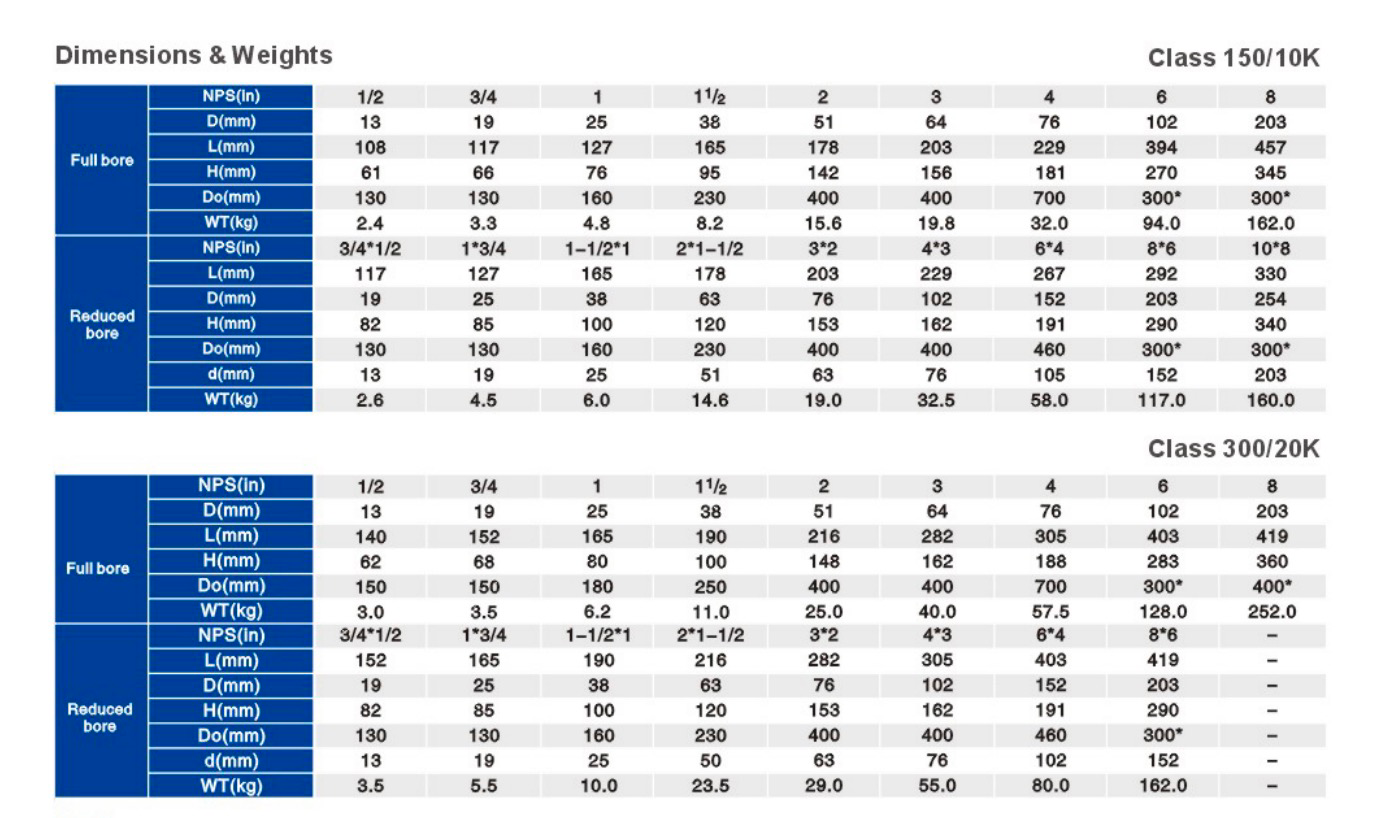
- Valve size data sheet
150LB/300LB
Testing Process
From raw materials to finished products, NORITE maintains 100% testing coverage, ensuring that every valve and pump you receive is built to last — safe, stable, and globally certified.

Pressure Testing
Each valve undergoes rigorous pressure and hydrostatic testing prior to shipment to verify body strength, sealing integrity, and pressure stability—ensuring zero leakage and long-term reliability in field operation.

Torque and Functional Testing
Confirming operating performance and precision.

Cycle Life Testing
Simulating long-term use under real working conditions.

Coating & Corrosion Resistance Testing
Validating surface protection and durability.
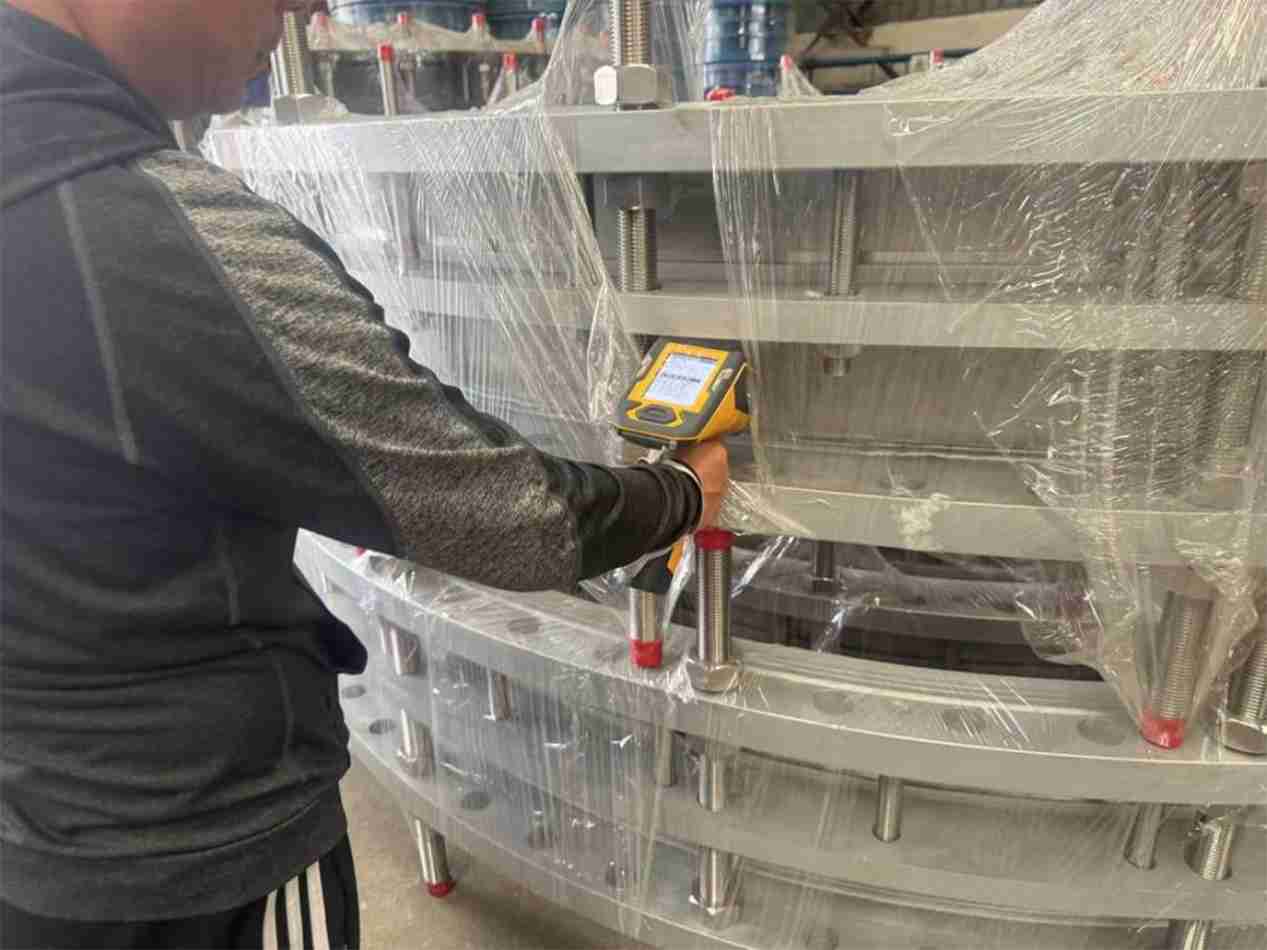
Dimensional & Material Analysis
Using spectrometers and coordinate measuring machines (CMM) for accuracy.
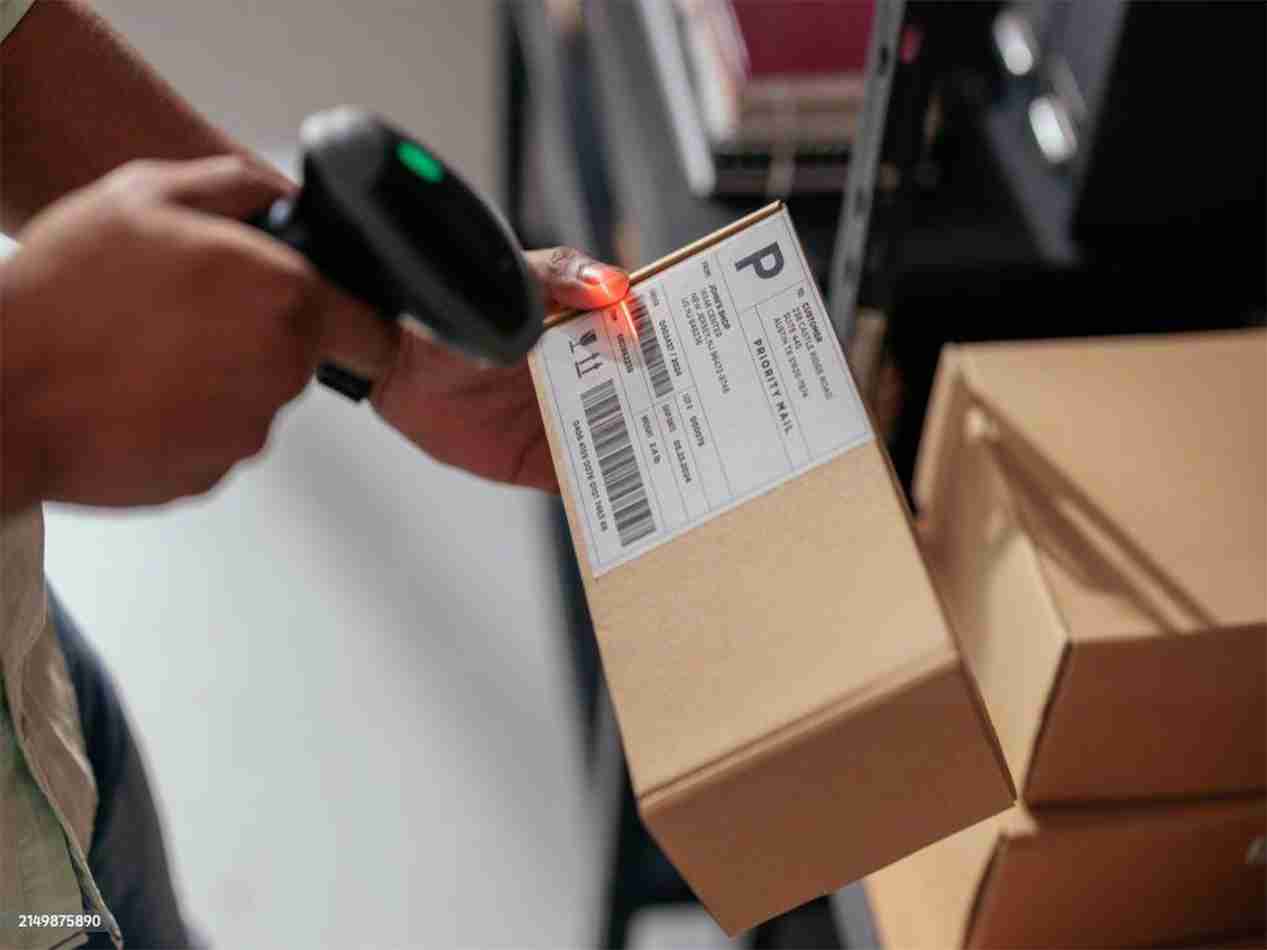
Traceability - Unique product code
Each product leaving our factory is accompanied by a full inspection report and a unique serial number, enabling full traceability and lifetime quality tracking.
Real Project Cases
Proven performance in critical applications worldwide – see our valves in action
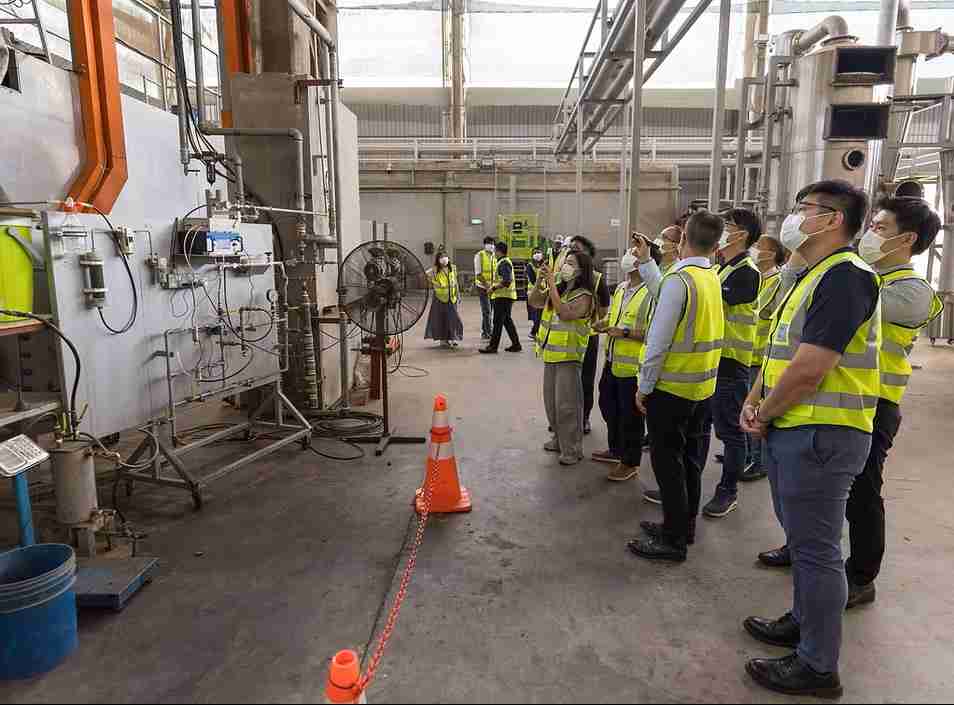


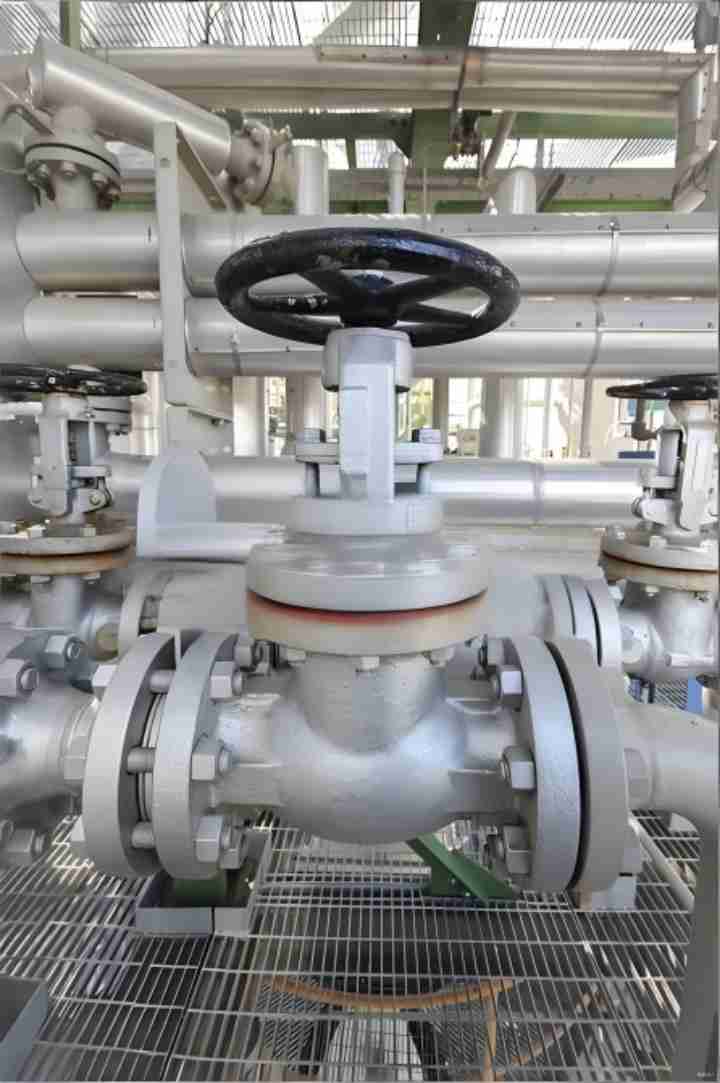

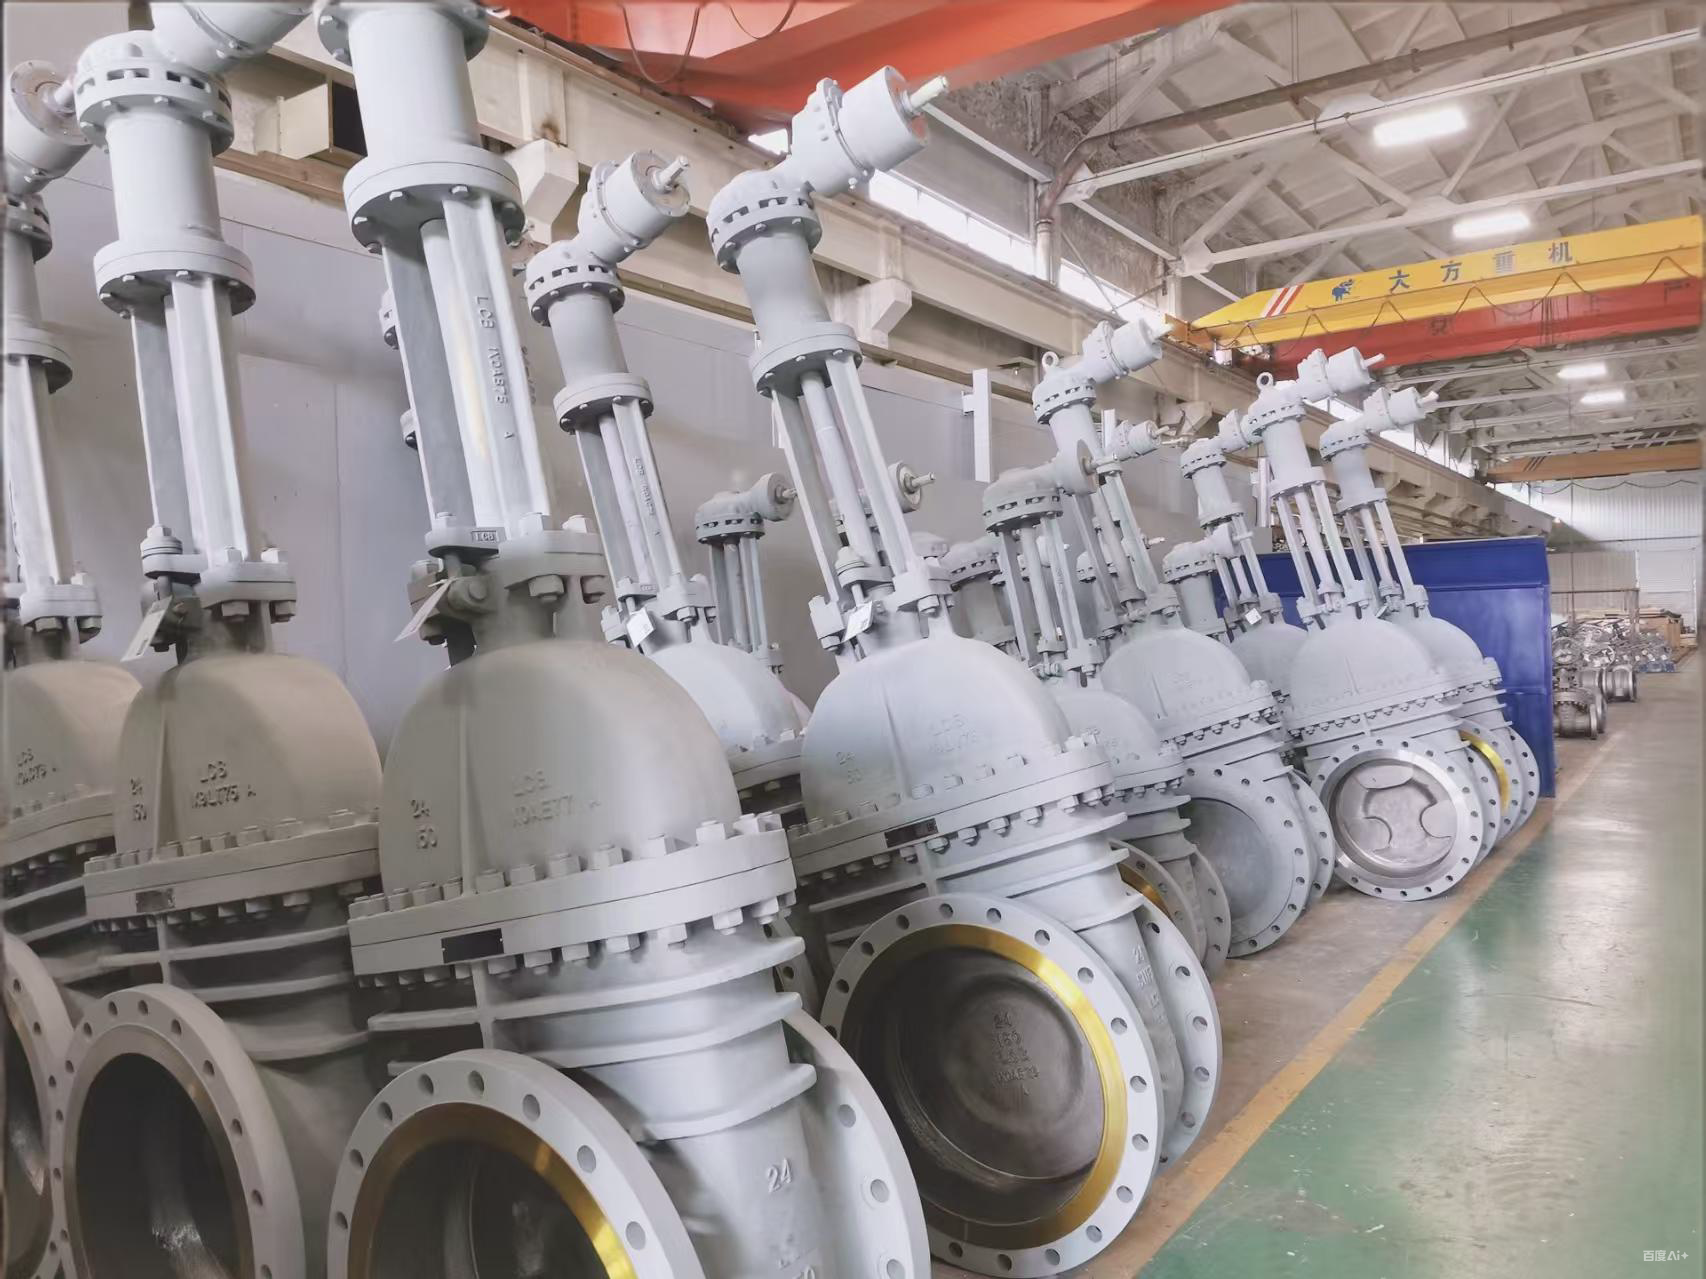
Valve Solution for Carbon Black Plant in Singapore
- Singapore
Customer/Owner: Carbon Black Plant in Singapore
- Working conditions/Challenges:
GEIH is a company dedicated to efficient energy and chemical material production. Their carbon black production line operates at extremely high temperatures, with some sections exceeding 425°C. The client needed a reliable valve control solution to ensure process stability and precise automated feeding in such harsh conditions.
- The type of equipment adopted:
We provide customers with stainless steel valves that can operate stably under high-temperature conditions, including gate valves, knife gate valves, ball valves and other products. We have also optimized the design of high-temperature pipeline valves. For process pipelines with operating temperatures exceeding 425°C, we have optimized the valve structure and selected sealing materials to ensure that the valves still have stable performance and long service life under high-temperature and high-frequency opening and closing conditions.
Key indicators: We also provide customers with intelligent electric actuators to achieve precise feeding control, assist customers’ production lines in realizing intelligent management, and improve system response speed and production line efficiency. Currently, we are cooperating with the GEIH engineering team to provide full-process valve design and selection services for its new production line, including technical parameter confirmation, selection suggestions, layout guidance, etc.
Achievements/advantages: The first batch of high-temperature valves has been supplied and put into operation.Customer feedback indicates good stability, and the operational efficiency of the production line has significantly improved. We are currently in the in-depth advancement stage of the new production line project and plan to introduce more intelligent control valves into the core sections.
Get Your Custom Quote
Our technical experts will analyze your requirements and provide a tailored solution with detailed specifications and competitive pricing.