
Flow Control, Zero Compromise
From municipal water to industrial flow systems — total reliability starts here.
From deep wells to pipelines and wastewater treatment, Norite delivers efficiency, durability, and trust in every drop.
- 5-Year Warranty
- ISO 9001 Certified
- 24/7 Support


Rubber joint
Vibration & Noise Absorption for Enhanced System Stability
Designed with excellent elasticity and damping performance, it effectively absorbs vibration and noise from pumps or piping systems, protecting connected equipment.
Compensates for Displacement and Thermal Expansion
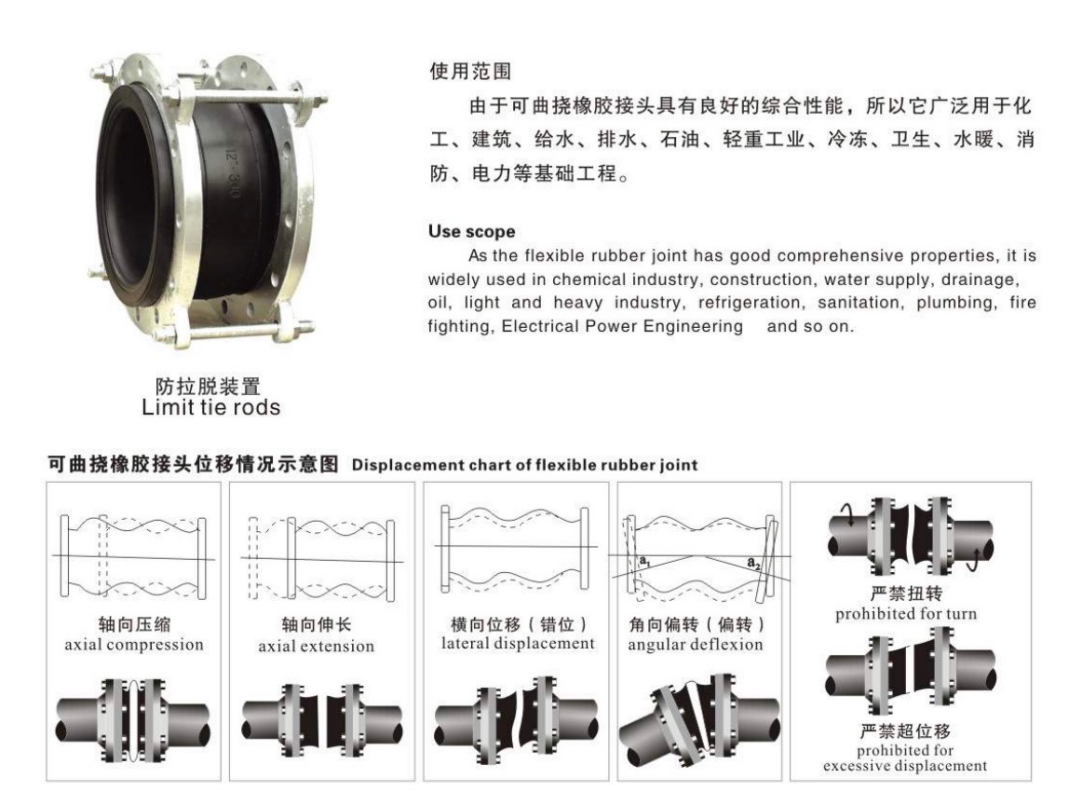
Allows multi-directional movement (axial, lateral, and angular), accommodating displacement from thermal expansion, ground settling, or misalignment.
Excellent Sealing and Easy Installation
Formed in one piece with high-elasticity rubber, the joint ensures tight sealing and simple flange connection for quick and easy installation or replacement.
Resistant to Corrosive Media with Wide Compatibility
Available in EPDM, NBR, and Viton to suit a wide range of media such as clean water, wastewater, chemicals, oil, and mild acids/alkalis.
Multiple Structural Options to Meet Project Requirements
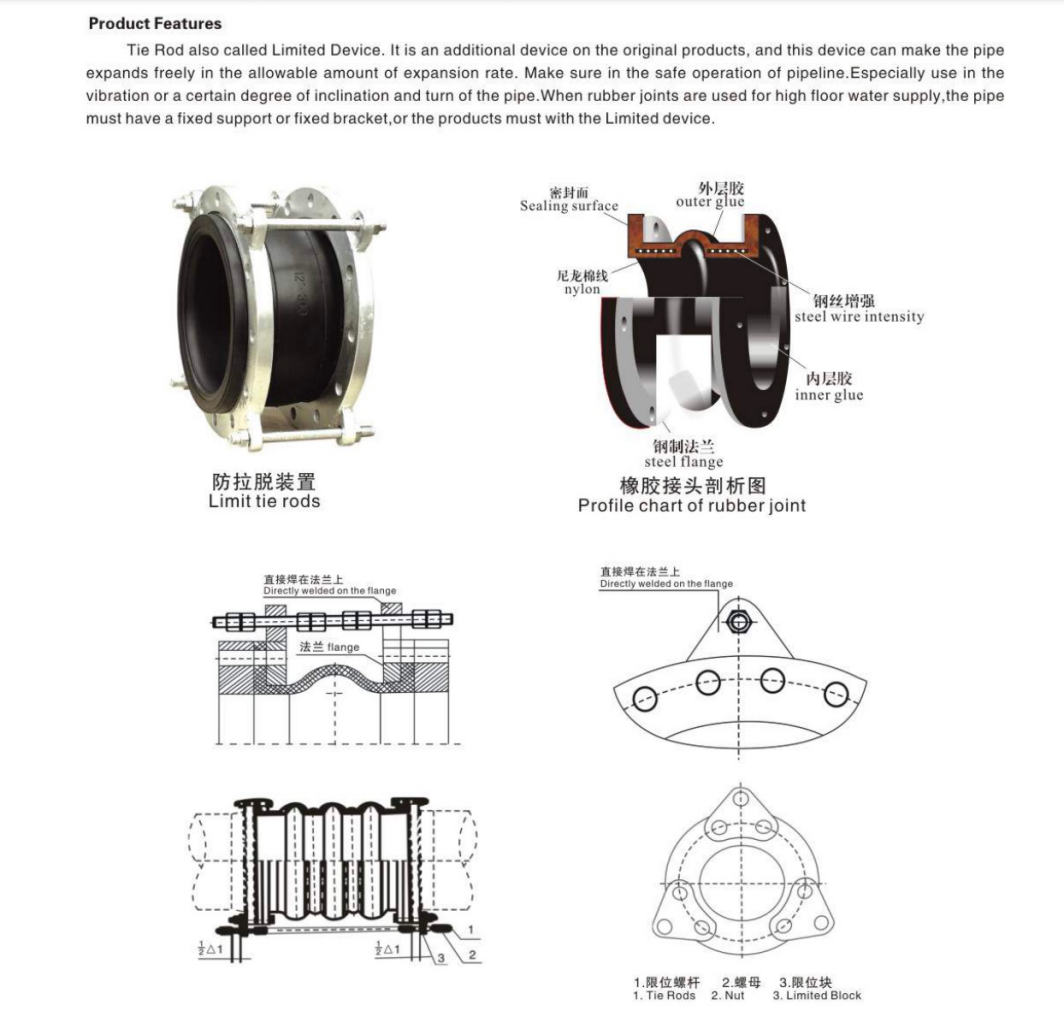
Offers various configurations—single/double sphere, eccentric, threaded, and limit rod types—to meet the diverse installation requirements of engineering projects.
Need custom specifications? Our engineers are ready to help.
Call: +86 15090163952 | Email: lisa@noritesolution.com
Proven Results That Drive Your Bottom Line
Real performance data from our Valve installations across critical industries worldwide

100% Pressure Tested
Tested under Class A sealing standard, across 10,000+ units.

20+ Years Lifespan
Proven performance in seawater, wastewater, and high-pressure pipelines.

8,000+ Valves Installed
Including power plants, municipal water systems, and industrial zones.

99.5% On-Time Delivery
Backed by lean production and strict QC.
Certifications & Standards


Technical Specifications
Engineered for optimal performance across a wide range of industrial applications
Model:
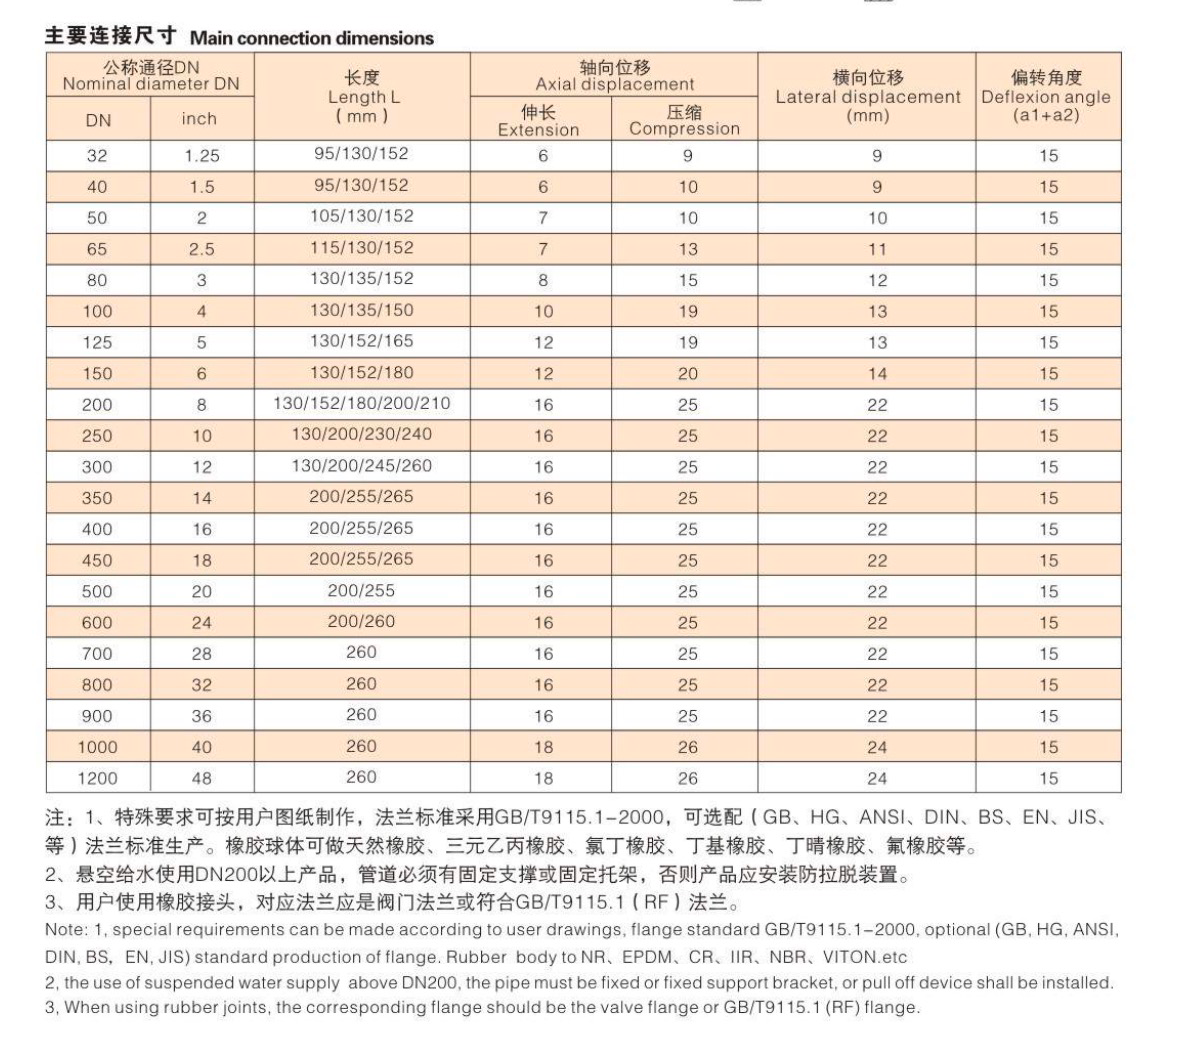
Size Range:
KXT,KST,KDF,JDX,JGD,WTX
DN50 – DN1200,2”-48”
Pressure Rating:
Standards:
PN10 / PN16/PN25/PN40;125LB/
150LB/300LB
EN545,ISO2531
Media:
Max Temperature:
Water and neutral liquids
Ball Material:
Flange:
NR,NBR,EPDM,SR,CR
Carbon steel, stainless steel, duplex stainless steel
Connection:
Certifications:
Flanged to EN1092-2,ANSI B16.5,BS4504
- Application Conditions
Urban water supply and building water systems
Used in water supply systems, booster stations, and high-rise HVAC pipelines to isolate vibration and reduce noise in pump connections.
Sewage treatment plants and drainage projects
Ideal for wastewater plants and drainage systems, improving operational stability and protecting pipeline components from fatigue and displacement.
Industrial fluid pipe network system
Widely used in pipelines of power plants, petrochemical, and metallurgy industries to transfer liquids and gases under varying pressures and media.
Farmland irrigation is matched with pumping stations
Commonly installed in fire protection systems to mitigate water hammer and ensure flexible, secure piping connections.
Seawater systems and desalination engineering
Special rubber materials or anti-corrosion lining make it suitable for seawater transport and desalination applications.
- Product Description
- Product specification and size
Testing Process
From raw materials to finished products, NORITE maintains 100% testing coverage, ensuring that every valve and pump you receive is built to last — safe, stable, and globally certified.

Pressure Testing
Each valve undergoes rigorous pressure and hydrostatic testing prior to shipment to verify body strength, sealing integrity, and pressure stability—ensuring zero leakage and long-term reliability in field operation.

Torque and Functional Testing
Confirming operating performance and precision.

Cycle Life Testing
Simulating long-term use under real working conditions.

Coating & Corrosion Resistance Testing
Validating surface protection and durability.
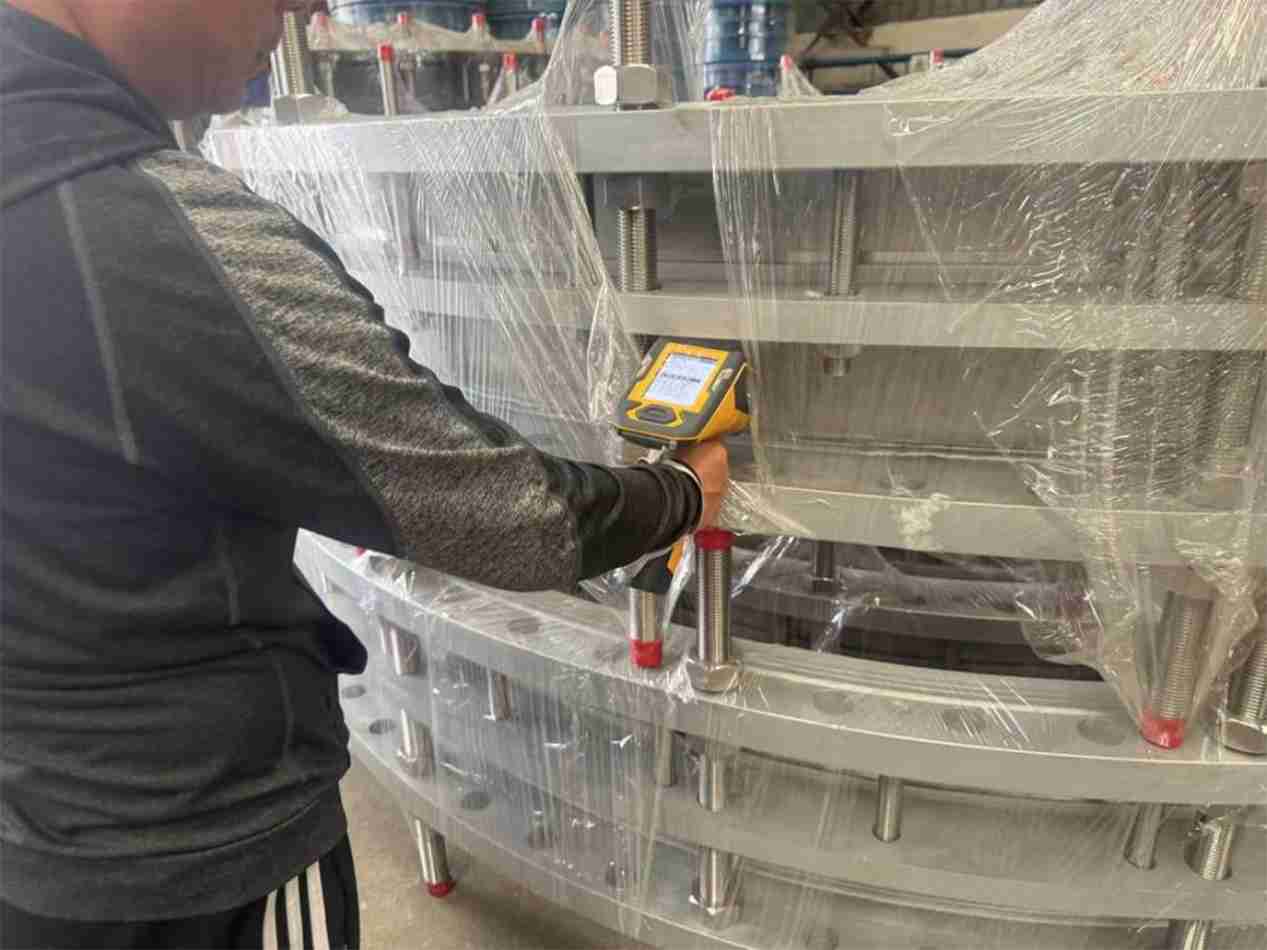
Dimensional & Material Analysis
Using spectrometers and coordinate measuring machines (CMM) for accuracy.
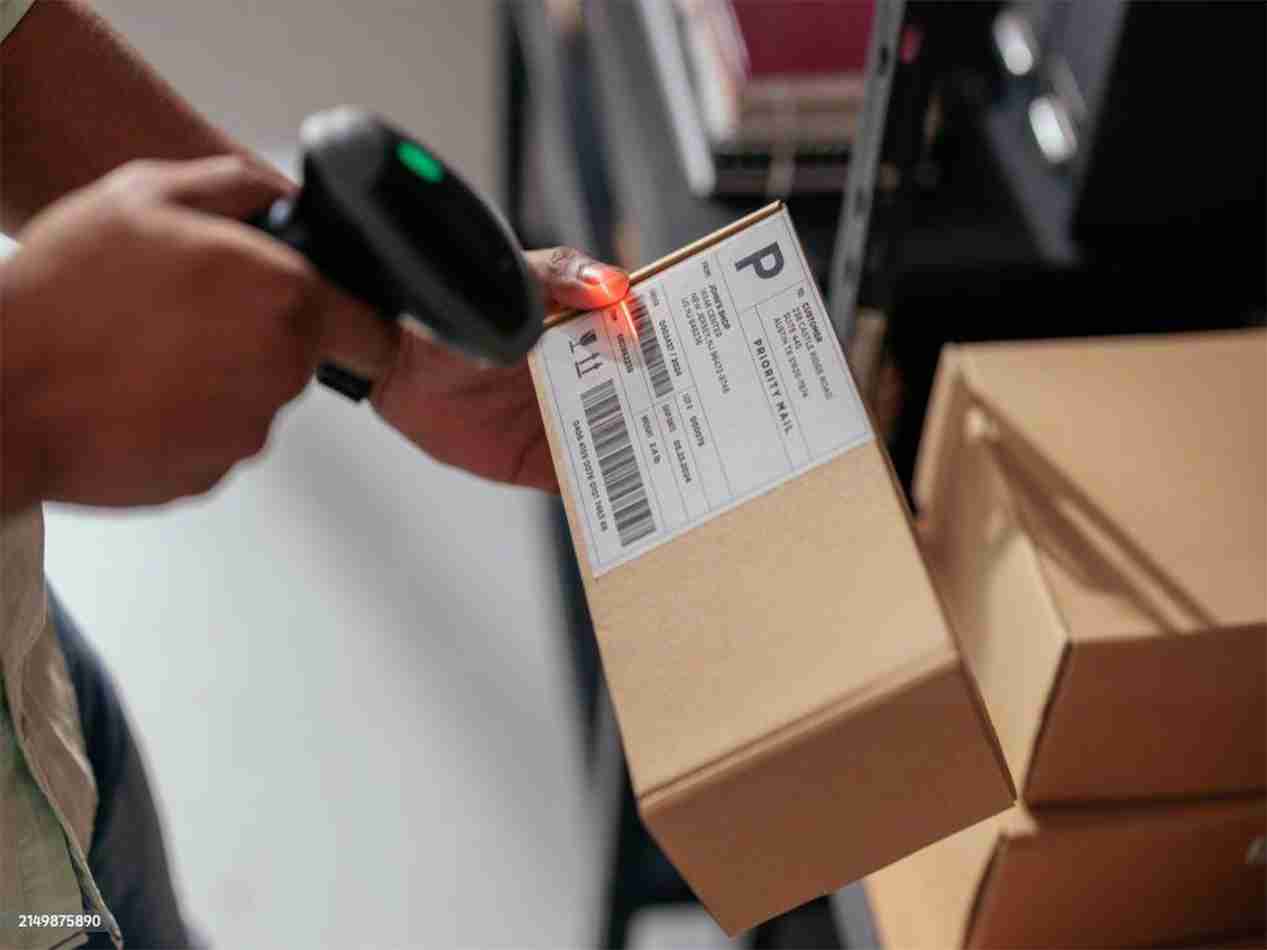
Traceability - Unique product code
Each product leaving our factory is accompanied by a full inspection report and a unique serial number, enabling full traceability and lifetime quality tracking.
Real Project Cases
Proven performance in critical applications worldwide – see our valves in action
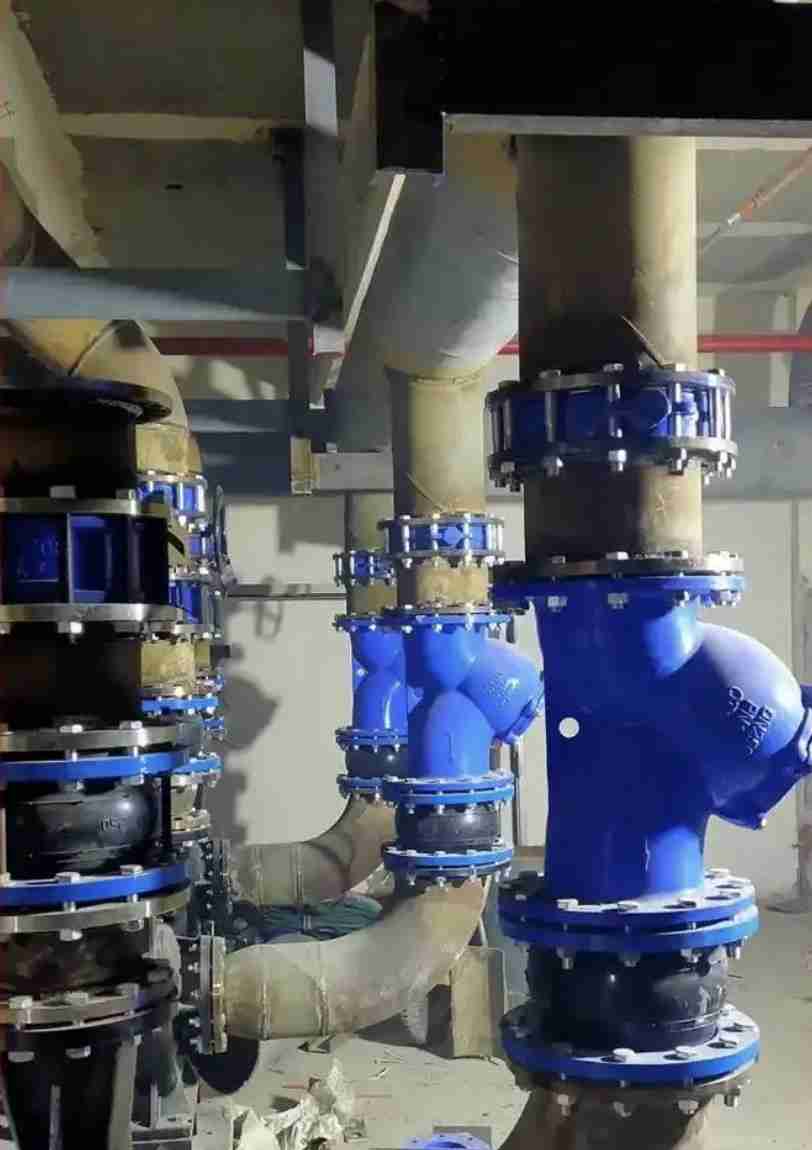
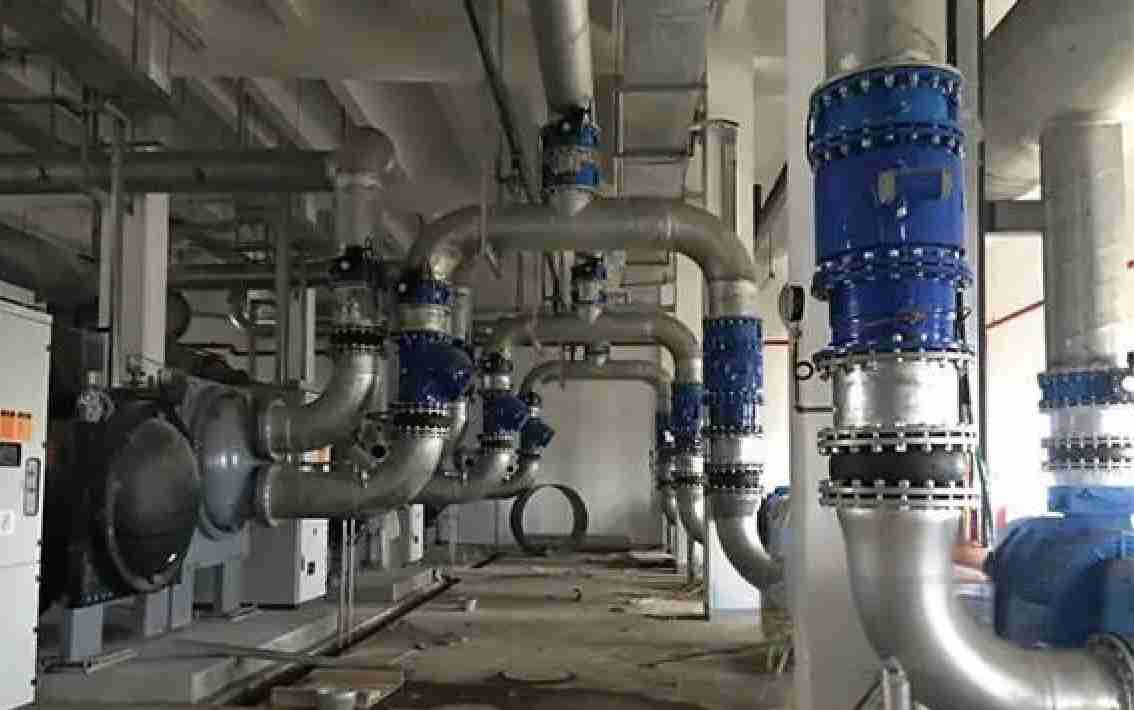
Bugolobi Wastewater Treatment & Pump Station (Uganda)
- Kampala, Uganda
Customer/Owner: Carbon Black Plant in Singapore
- Working conditions/Challenges:
The Bugolobi Wastewater Treatment Plant is one of the largest wastewater treatment facilities in East Africa, with a treatment capacity of approximately 45,000,000 L/ day (about 45 ML/day).
The project includes major sewage pretreatment stations, pumping stations and a sewer network of nearly 31 km.
The treatment plant has improved the discharge quality of the inner lake basin and plans to further expand its processing capacity.
Key indicators:We provided a complete set of valves and pipe fittings for this pumping station,The project has been delivered on schedule and is currently operating well.
Get Your Custom Quote
Our technical experts will analyze your requirements and provide a tailored solution with detailed specifications and competitive pricing.