
Smart Insight, Smart Control
Delivering Intelligent Solutions for Water and Industrial Systems
From deep wells to pipelines and wastewater treatment, Norite delivers efficiency, durability, and trust in every drop.
- 5-Year Warranty
- ISO 9001 Certified
- 24/7 Support


Gate
Excellent corrosion resistance for harsh environments
The valve is highly resistant to corrosion, making it suitable for use in acidic, alkaline, seawater, and sewage environments. It is adaptable to a wide range of applications, including municipal, chemical, and hydraulic projects, ensuring a longer service life.
Reliable sealing with adjustable compression
The valve features a rubber-metal hybrid sealing structure, which can be adjusted using the wedge block to ensure a tight seal. Even after years of use, slight leakage can be easily repaired and maintained.
Low operating torque with multiple actuation options
The valve is designed with a lightweight gate and minimal friction, ensuring that the manual operation torque does not exceed 100N. Multiple actuation options are available, including manual, electric, pneumatic, and electro-hydraulic drives, to meet the needs of different projects.
Lightweight structure for easy transport and installation
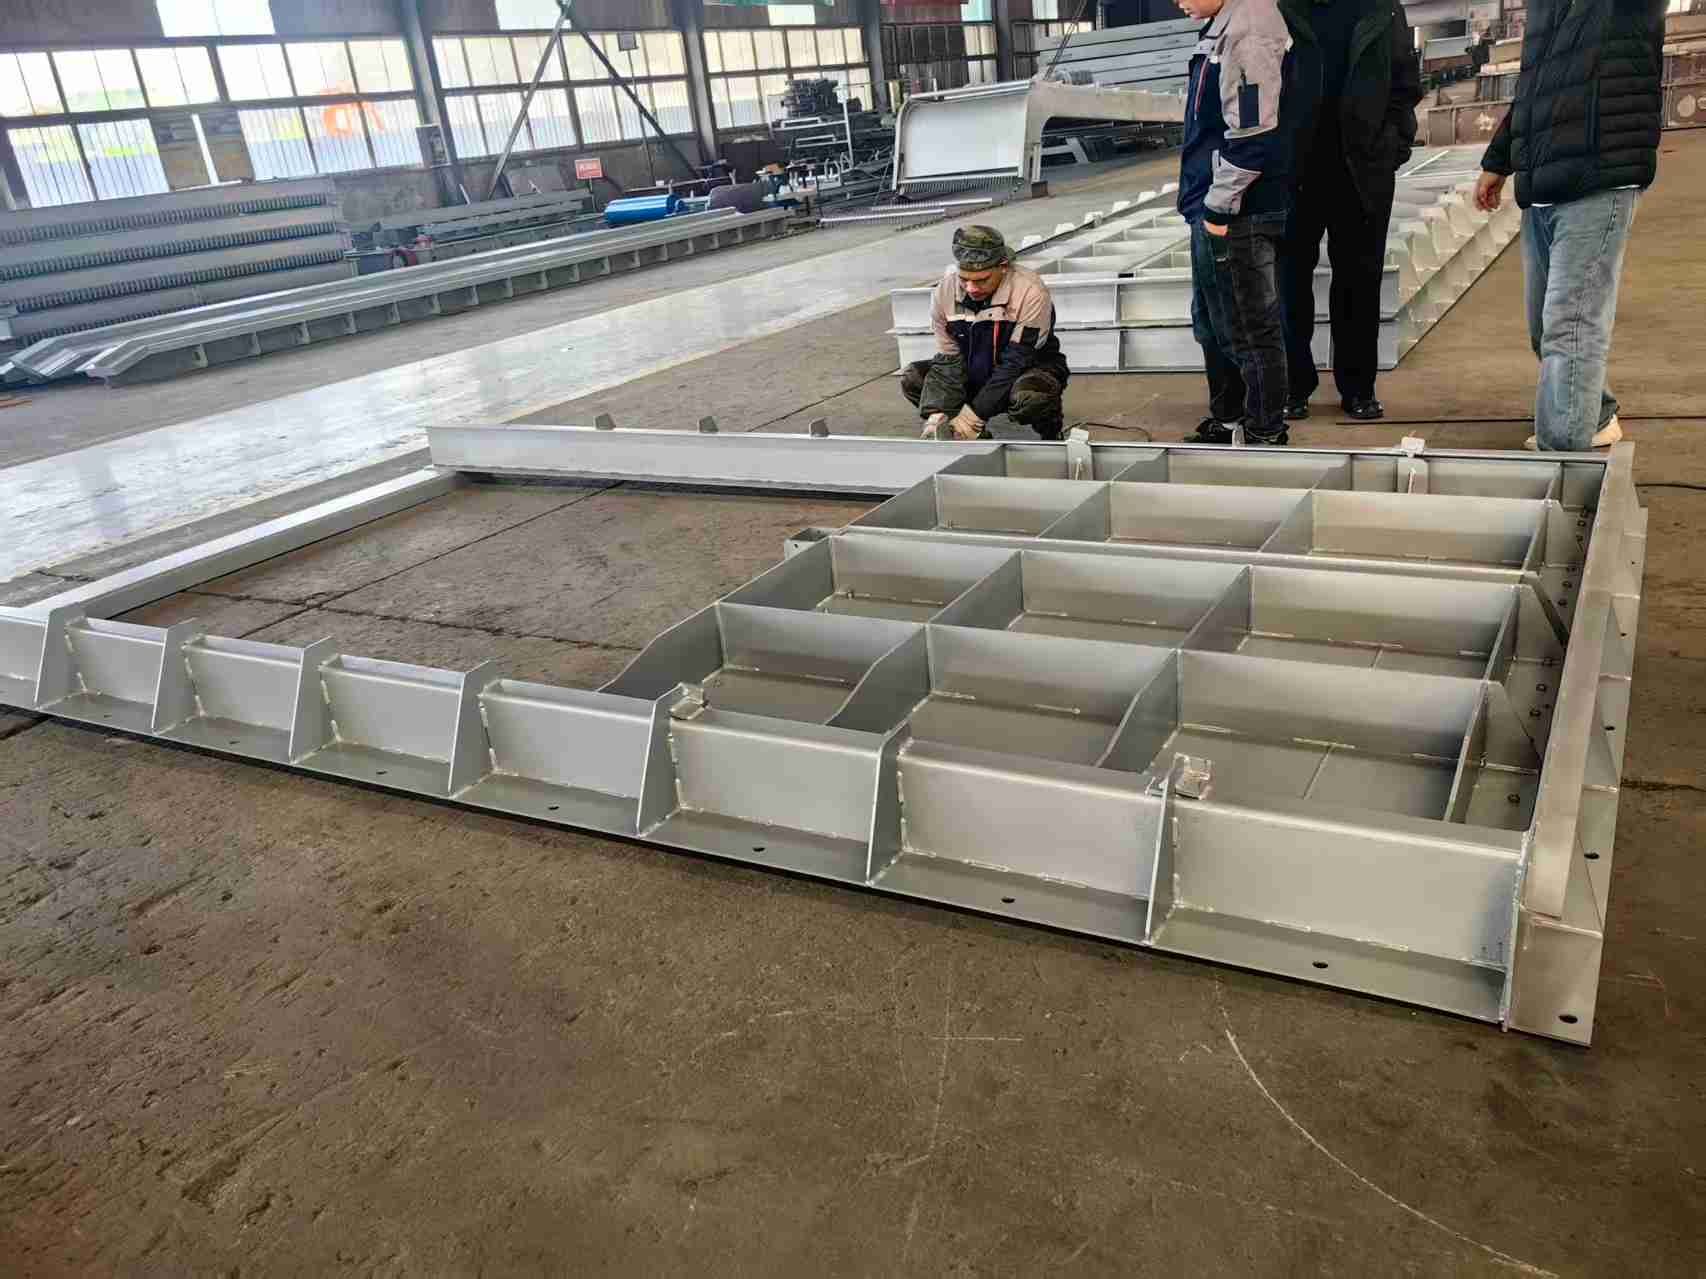
The valve body is constructed using stainless steel or carbon steel welding, with a weight that is about one-third of that of a cast iron gate valve. This significantly reduces transportation and installation costs, making it suitable for projects with complex on-site construction conditions.
Long service life and easy maintenance
The gate and guide rail contact area is minimal, reducing friction and wear. Stainless steel gates can last for over 15 years, and carbon steel versions last over 10 years. The valve is easy to maintain, with low operational costs and simple repair processes.
Need custom specifications? Our engineers are ready to help.
Call: +86 15090163952 | Email: lisa@noritesolution.com
Proven Results That Drive Your Bottom Line
Real performance data from our Valve installations across critical industries worldwide

100% Pressure Tested
Tested under Class A sealing standard, across 10,000+ units.

20+ Years Lifespan
Proven performance in seawater, wastewater, and high-pressure pipelines.

8,000+ Valves Installed
Including power plants, municipal water systems, and industrial zones.

99.5% On-Time Delivery
Backed by lean production and strict QC.
Certifications & Standards


Technical Specifications
Engineered for optimal performance across a wide range of industrial applications
Types:
Size:
Cast iron gates, web-wall gates, electric gates
300-3000mm
Media:
Material:
Water and neutral liquids
Carbon steel, stainless steel
Sealing strips:
Working head:
Rubber /EPDM/NBR
Temperature:
Drive mode:
≦80℃
Manual, Hoist, Electric
Certifications:
ISO,CE Approved
- Application Conditions
Municipal Water Supply and Drainage
Used in urban water supply networks, water treatment plant inlets and outlets, and reservoir water level control. Offers excellent sealing and corrosion resistance for reliable municipal operations.
Wastewater Treatment Plants and Pump Stations
Installed at sewage inlets, sedimentation tanks, and lift stations to control flow direction and prevent backflow. A critical component in environmental protection systems.
Water Conservancy and Hydropower Projects
Widely used in sluice gates, diversion channels, and hydropower station inlets for flow regulation, water cut-off, and flood discharge coordination.
Industrial Fluid Control Systems
Used in fluid isolation and control across industries such as chemical, paper-making, steel, and power generation. Withstands a wide range of corrosive media.
Seawater Desalination and Offshore Platforms
Ideal for seawater intake systems and pipeline control in desalination plants and offshore platforms. Corrosion-resistant materials ensure long-term durability.
- Product Data Sheet
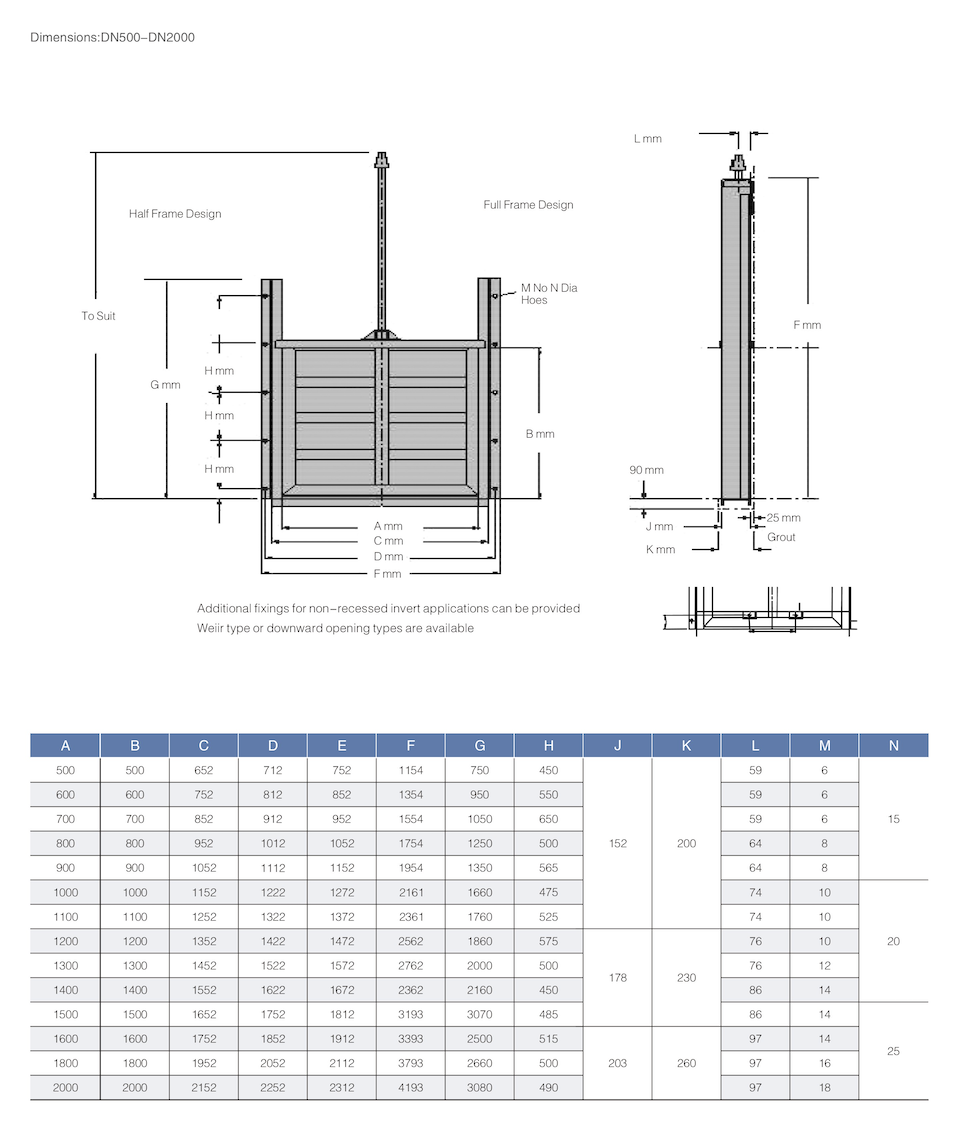

- Hoist parameter table

Testing Process
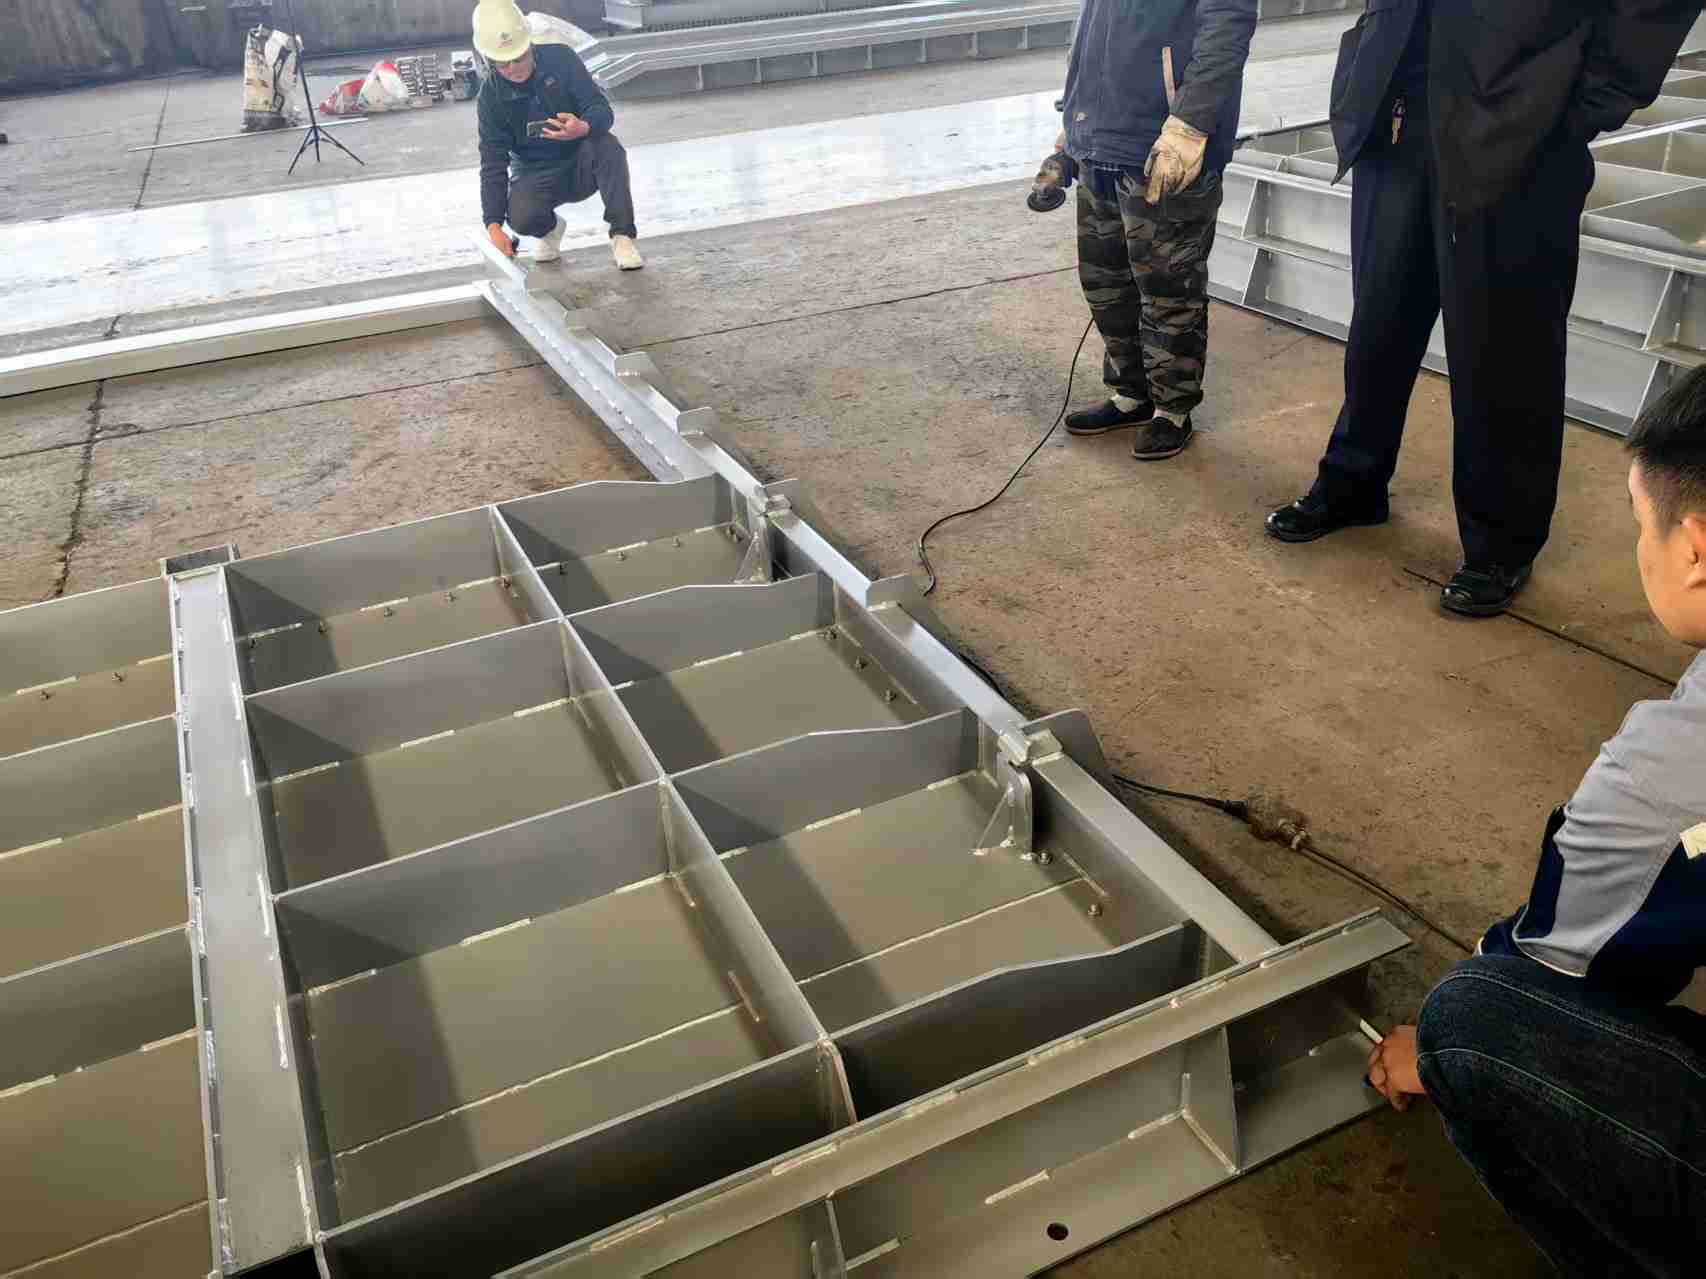
From raw materials to finished products, NORITE maintains 100% testing coverage, ensuring that every valve and pump you receive is built to last — safe, stable, and globally certified.

Pressure Testing
Each valve undergoes rigorous pressure and hydrostatic testing prior to shipment to verify body strength, sealing integrity, and pressure stability—ensuring zero leakage and long-term reliability in field operation.

Torque and Functional Testing
Confirming operating performance and precision.

Cycle Life Testing
Simulating long-term use under real working conditions.

Coating & Corrosion Resistance Testing
Validating surface protection and durability.
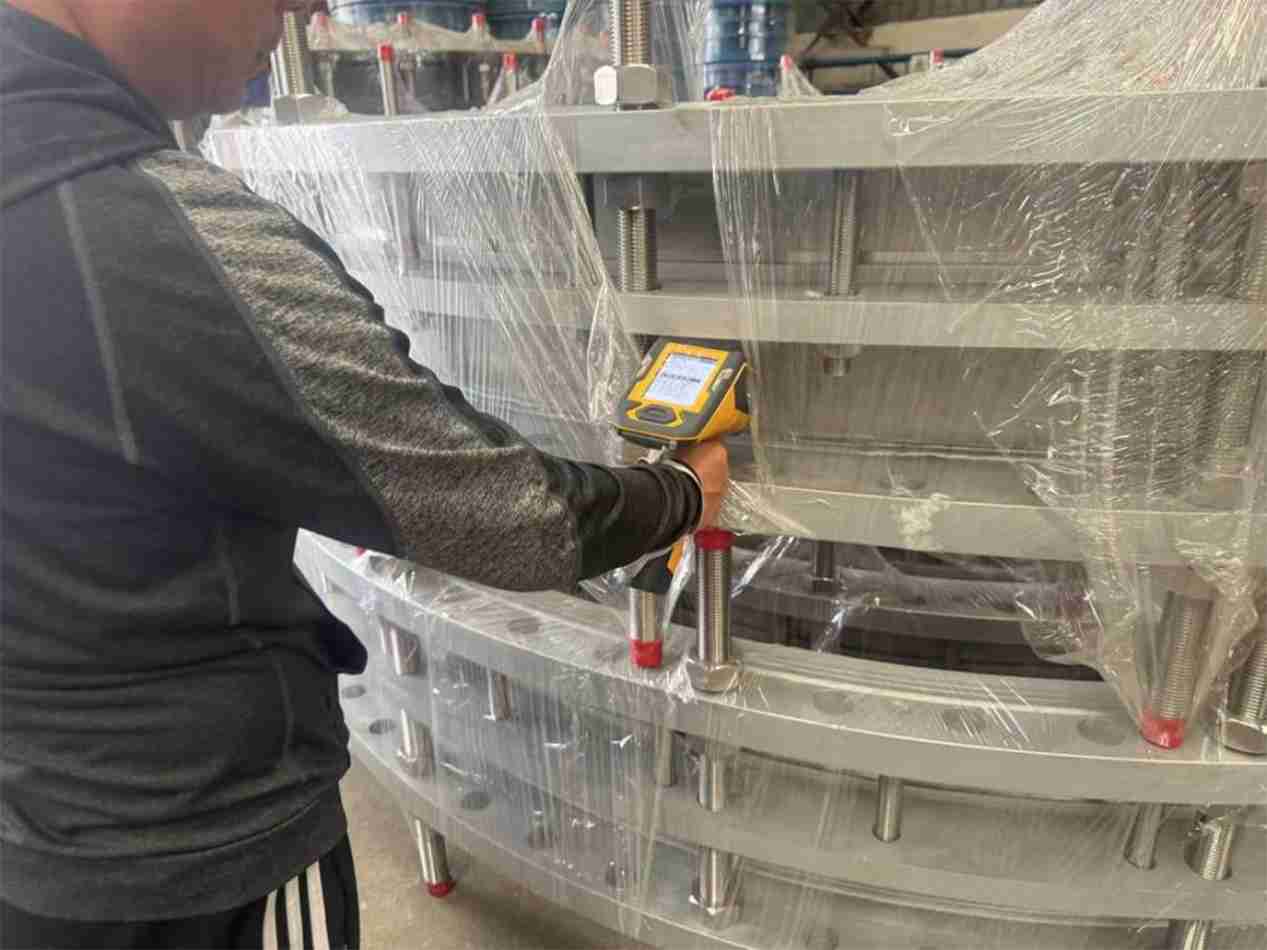
Dimensional & Material Analysis
Using spectrometers and coordinate measuring machines (CMM) for accuracy.
Traceability - Unique product code
Each product leaving our factory is accompanied by a full inspection report and a unique serial number, enabling full traceability and lifetime quality tracking.
Real Project Cases
Proven performance in critical applications worldwide – see our valves in action
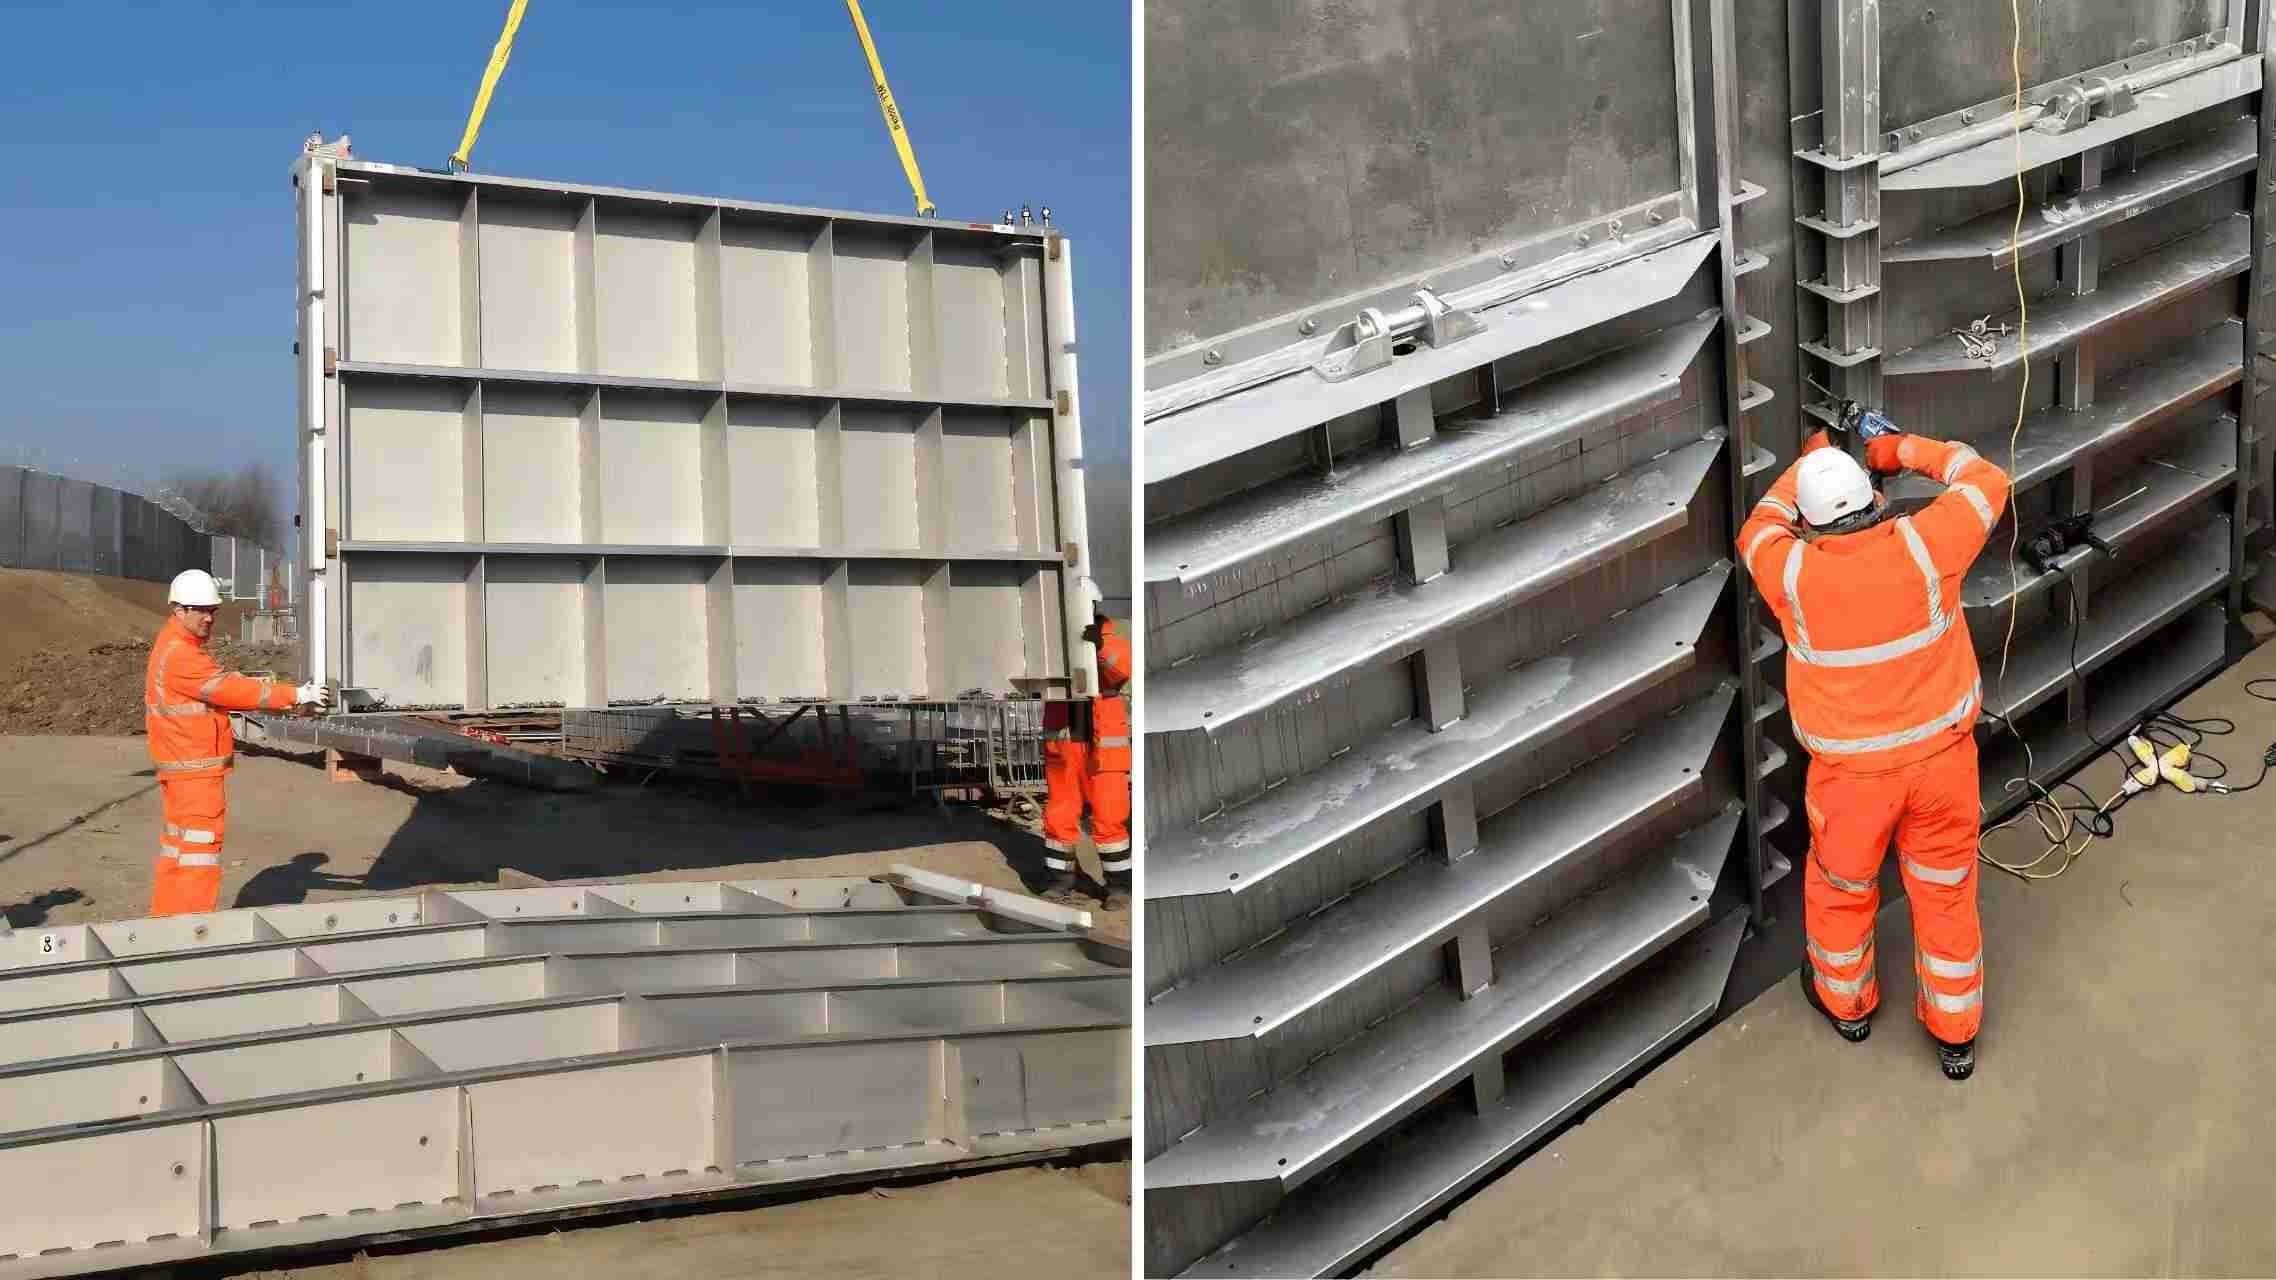
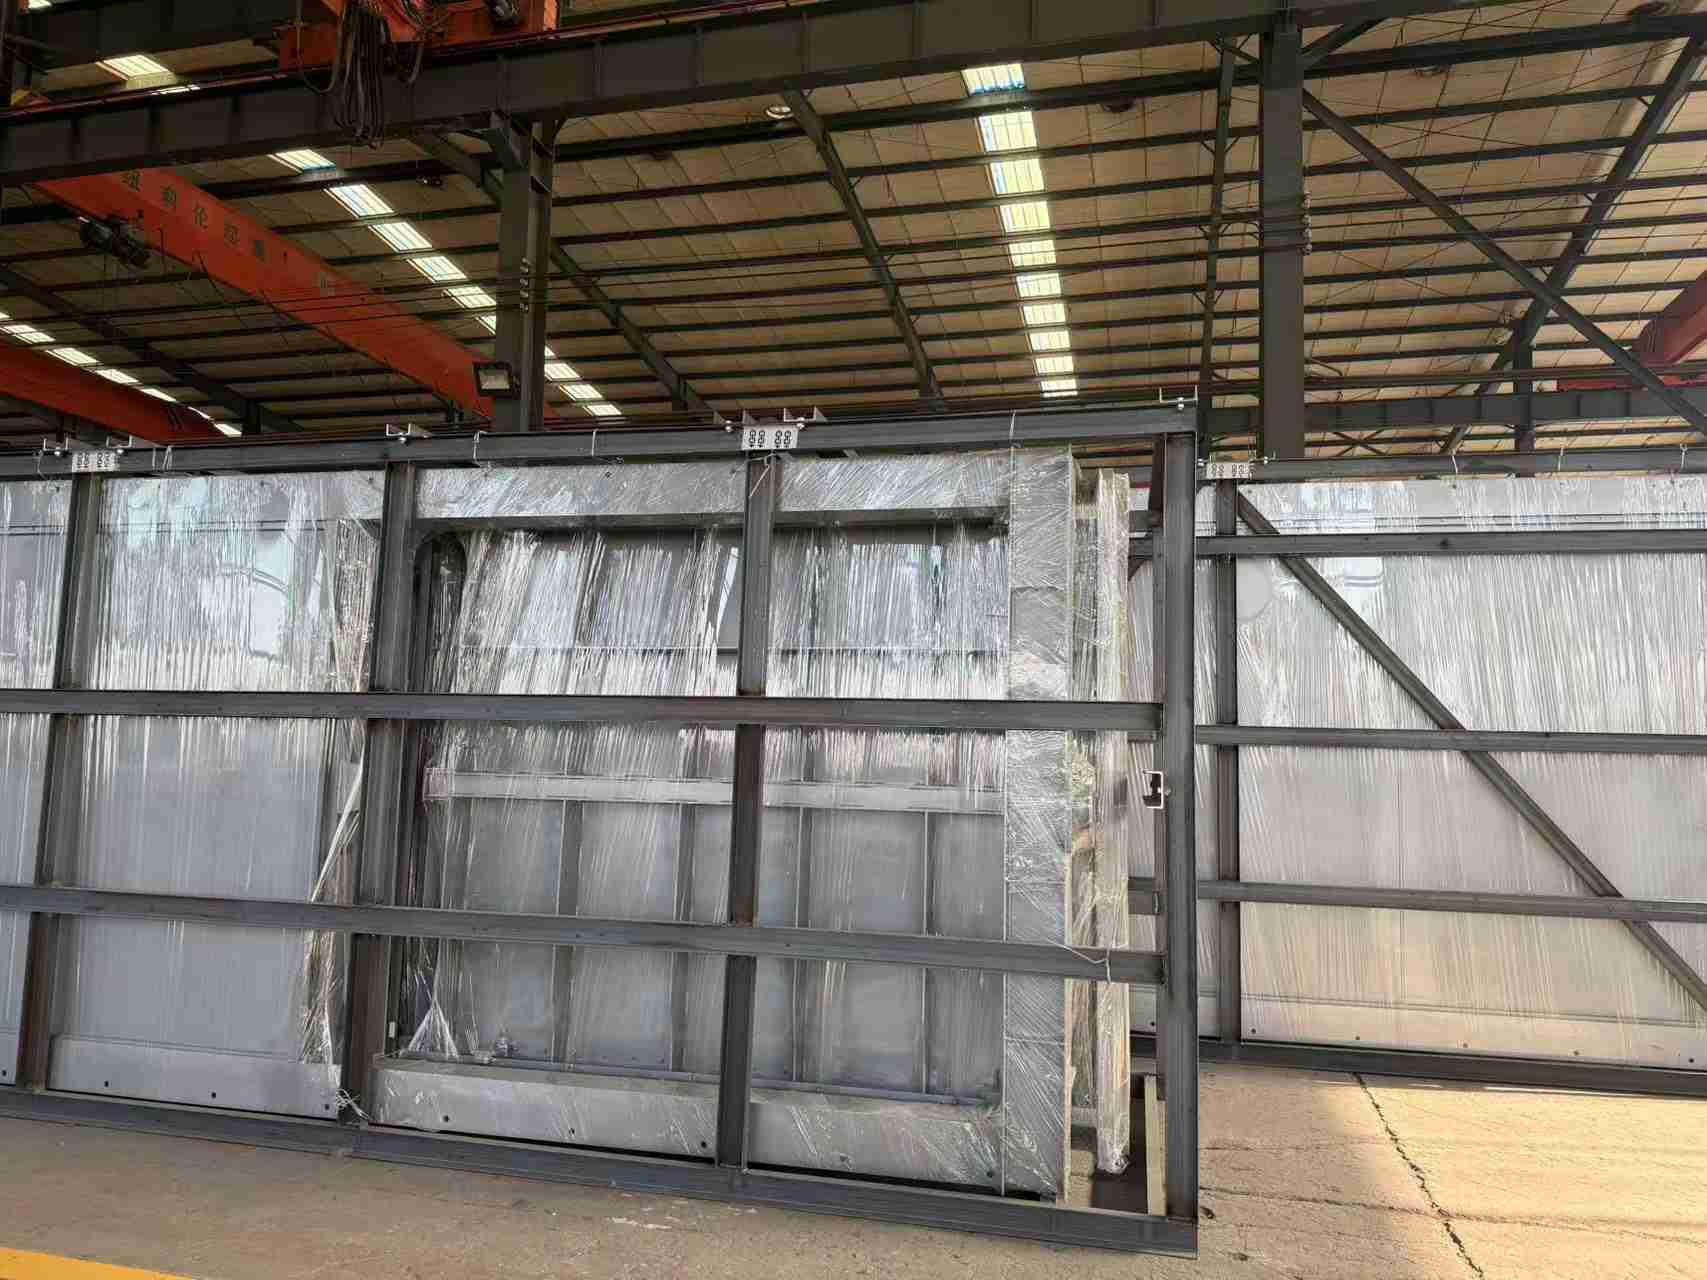
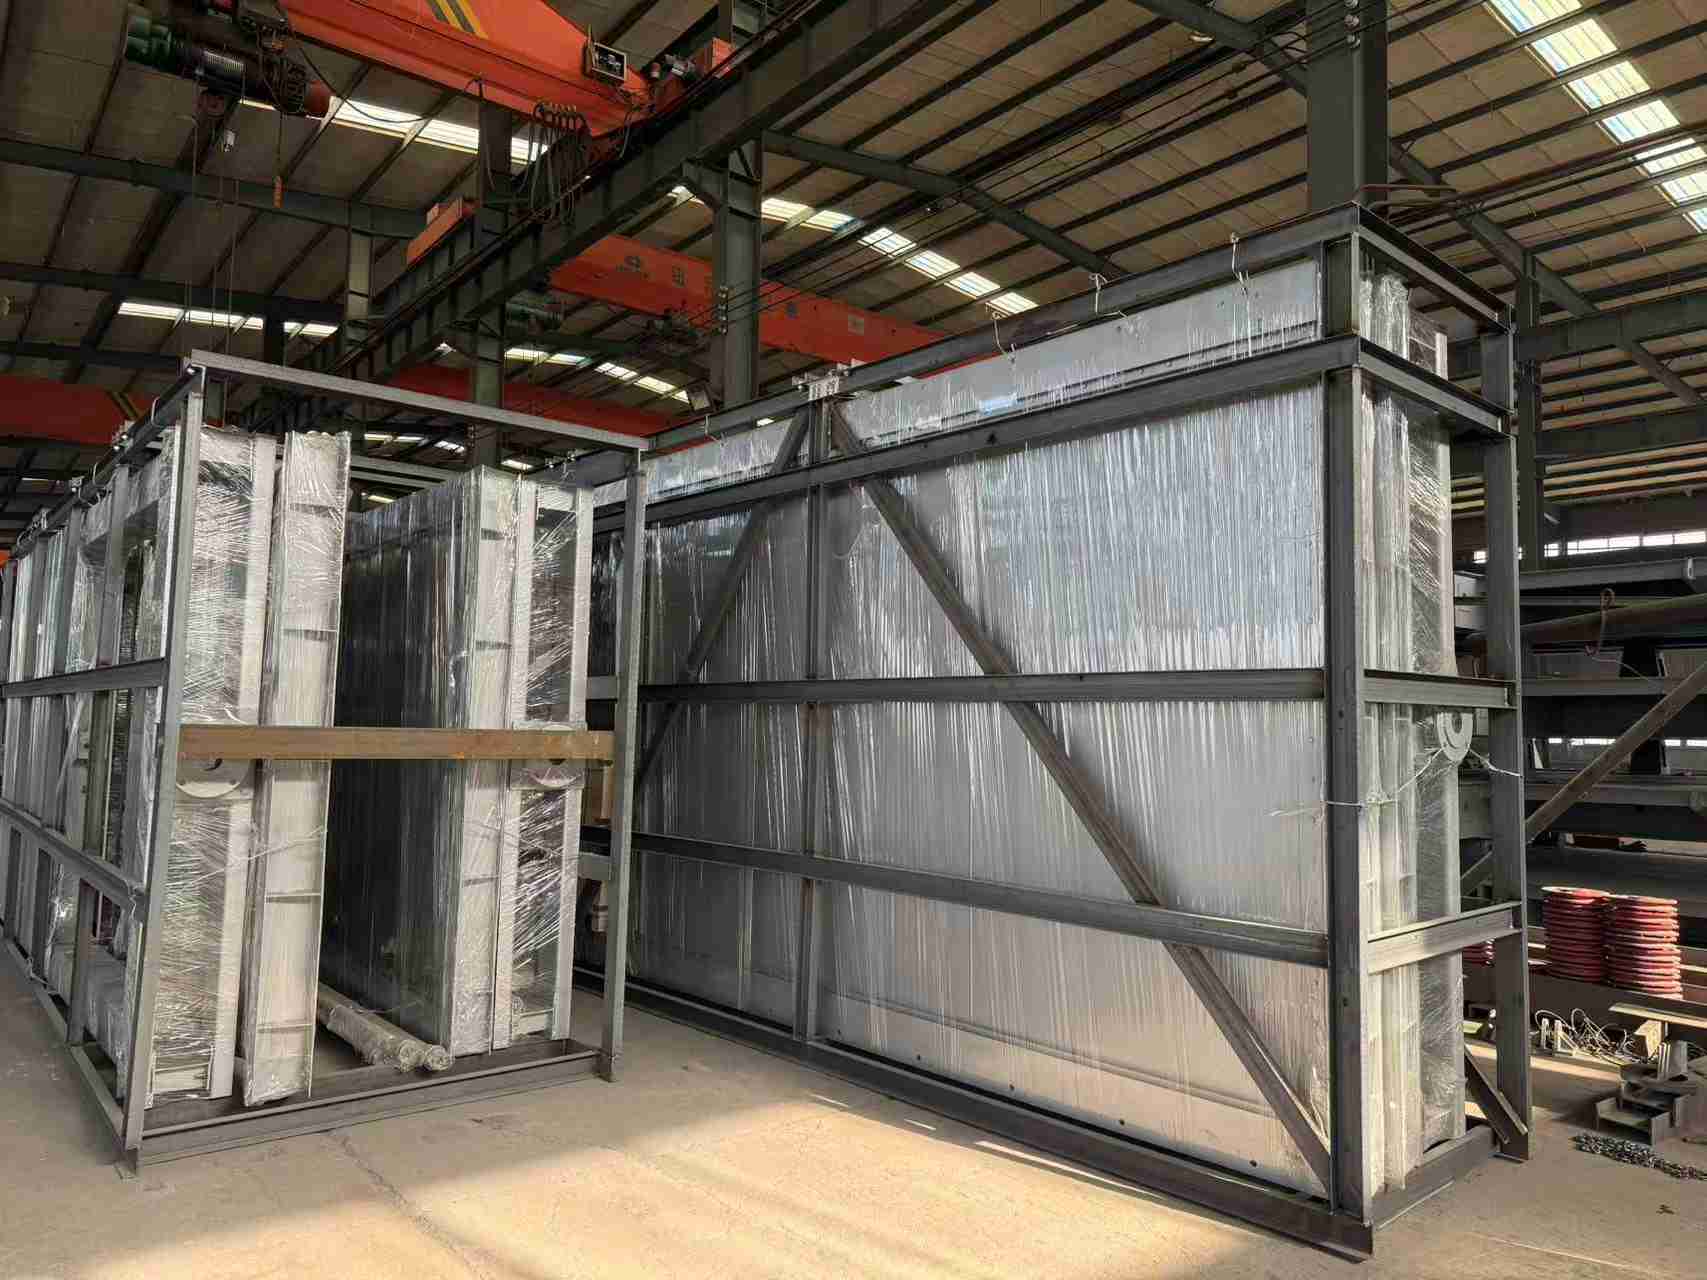
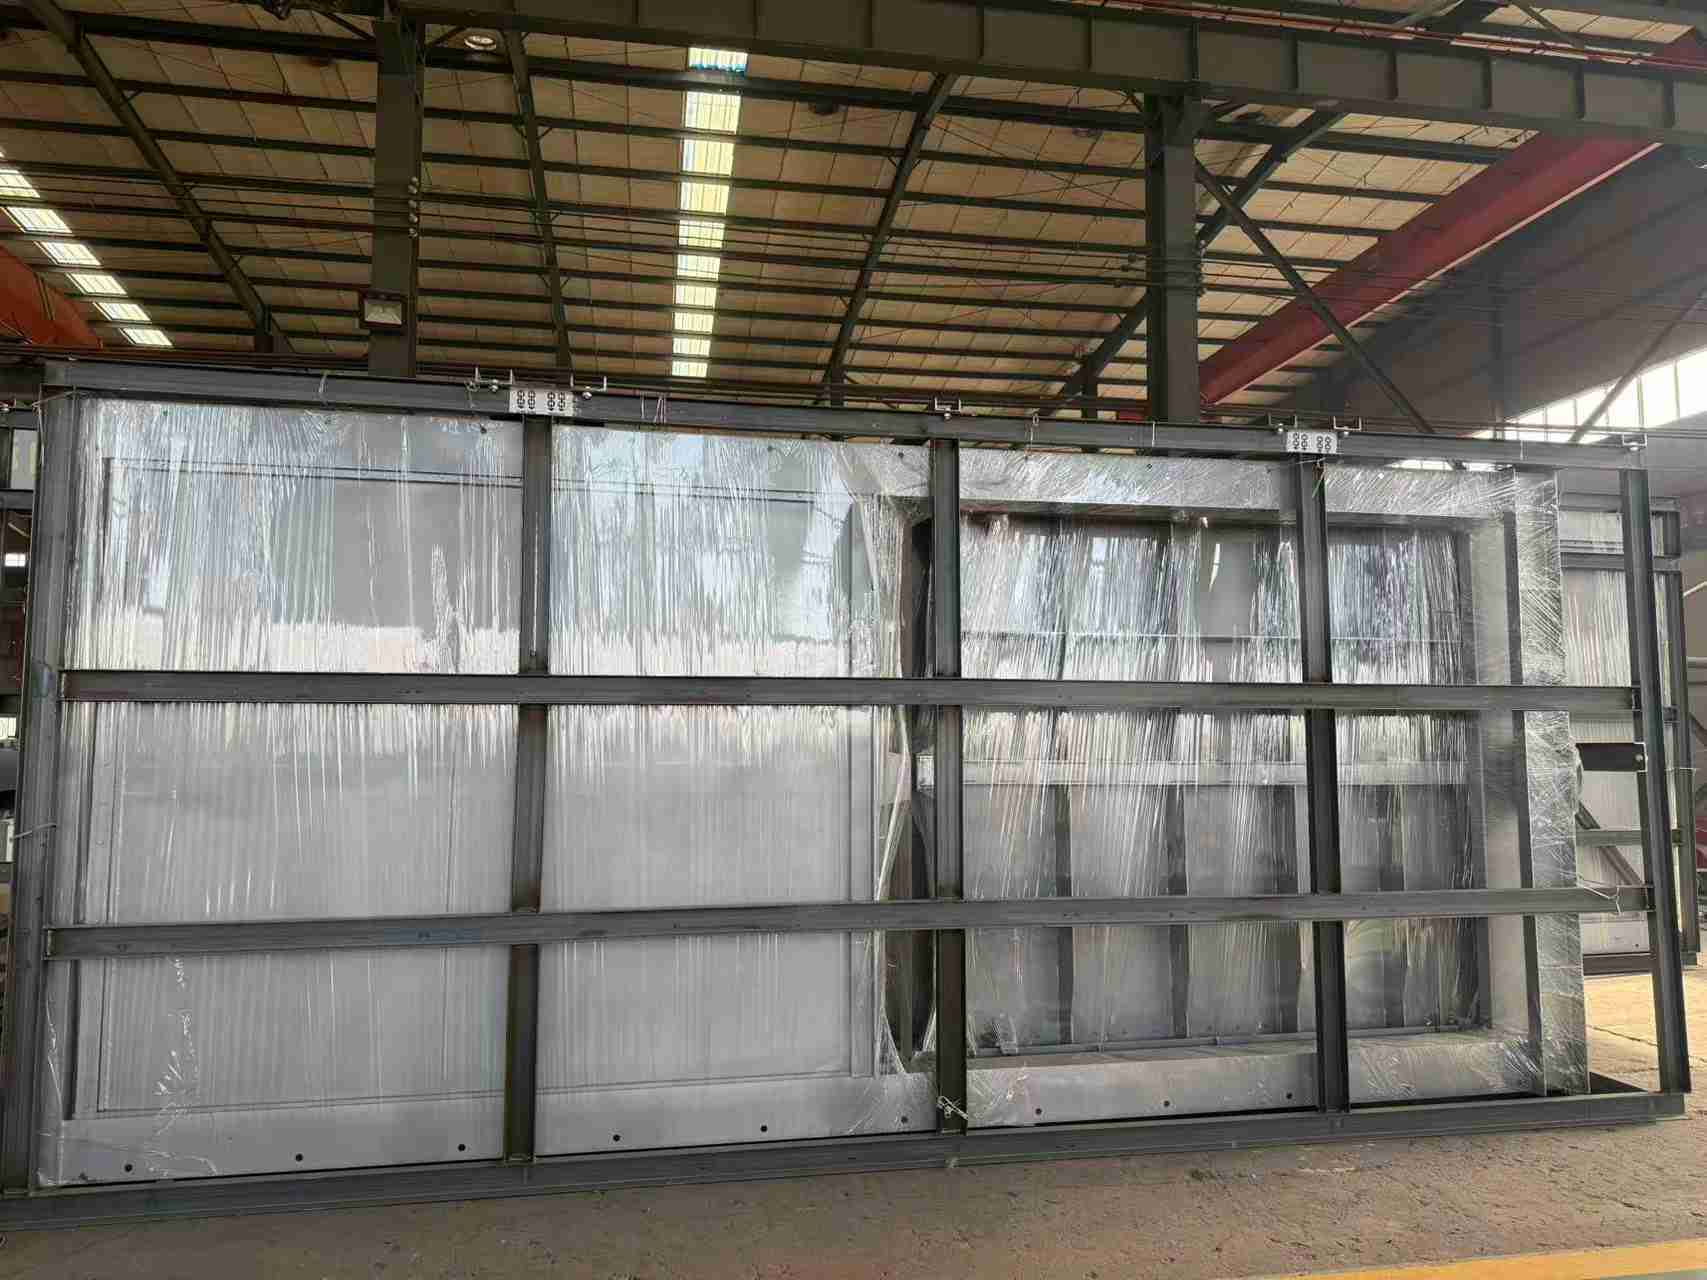


Ebaps Vila Velha
- Espirito Santo State, Brazil
Customer/Owner: “Estacǎo de Bombeamento de Áquas Pluviais
- Working conditions/Challenges:
This pumping station is a rainwater drainage pumping station. As part of the city ‘s large-scale drainage/flood control infrastructure, it is equipped with approximately 12 kilometers of closed drainage pipe galleries + 7 kilometers of anti-seepage channels.
- The type of equipment adopted:
We provide three 900QZB-315KW submersible mixed-flow pumps with a diameter of φ1400mm for this project, along with three 2*4.7m automatic rotary screen cleaners, eleven electric gates and five flap valves.
Key indicators:This equipment is installed at the sewage inlet to control the flow direction of sewage and prevent backflow. It is one of the important devices in environmental protection projects.
Get Your Custom Quote
Our technical experts will analyze your requirements and provide a tailored solution with detailed specifications and competitive pricing.