
Smart Insight, Smart Control
Delivering Intelligent Solutions for Water and Industrial Systems
From deep wells to pipelines and wastewater treatment, Norite delivers efficiency, durability, and trust in every drop.
- 5-Year Warranty
- ISO 9001 Certified
- 24/7 Support


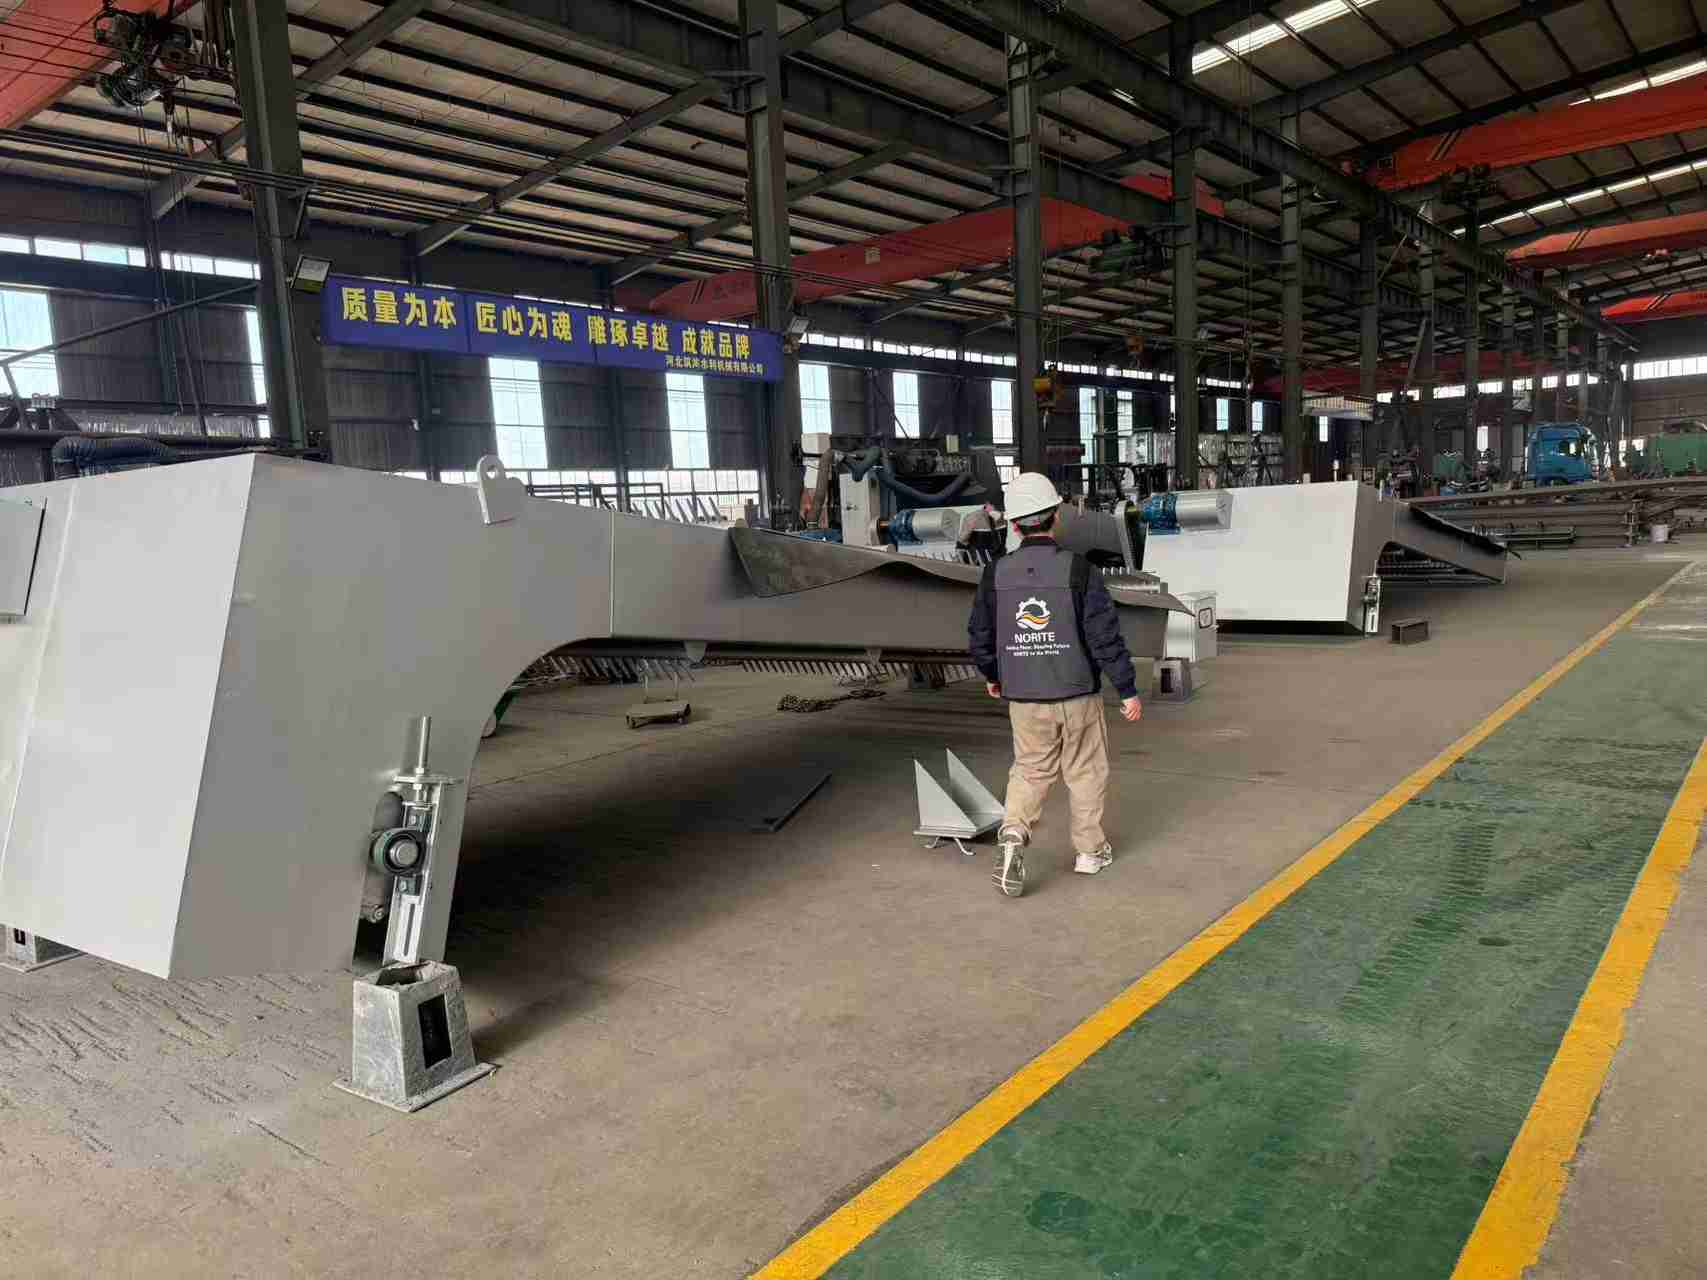
Automatic Rotary Bar Screen Cleaner
Anti-Jamming Design
The rake teeth are positioned at the center of the chain and operate in a reversed movement pattern, preventing hard debris from being forced to the bottom and jamming the chain or rake — ensuring more reliable continuous operation.
Overload Protection for Equipment Safety
An overload safety protection device installed on the sprocket at the reducer output shaft prevents damage caused by accidental overloads, enhancing system safety and longevity.
High-Efficiency Multi-Rake Cleaning
The rotary chain is equipped with multiple cleaning rakes, enabling rapid capture and removal of debris — resulting in thorough and highly efficient cleaning performance.
Simple Structure & Reliable Operation
The machine features a compact, well-engineered design for stable operation, easy installation and maintenance — significantly reducing lifecycle costs.
Intelligent Automated Control
Supports PLC interface and integration with other systems, enabling automated control such as timed operation, water level control and differential level control. In case of unexpected blockage, the device can automatically start without waiting for a service cycle.
Need custom specifications? Our engineers are ready to help.
Call: +86 15090163952 | Email: lisa@noritesolution.com
Proven Results That Drive Your Bottom Line
Real performance data from our Valve installations across critical industries worldwide

100% Pressure Tested
Tested under Class A sealing standard, across 10,000+ units.

20+ Years Lifespan
Proven performance in seawater, wastewater, and high-pressure pipelines.

8,000+ Valves Installed
Including power plants, municipal water systems, and industrial zones.

99.5% On-Time Delivery
Backed by lean production and strict QC.
Certifications & Standards


Technical Specifications
Engineered for optimal performance across a wide range of industrial applications
Types:
Width of the grid channel:
Flat grating, rotary grating, perforated plate type, wire rope traction type, hydraulic grab type
800-4000mm
Media:
Material:
Water and neutral liquids
Carbon steel, stainless steel
Rake tooth speed:
Slag discharge height:
4m/s
Installation Angle:
Motor power:
60°,65°,70°,75°,80°
1.1-4KW
Certifications:
ISO,CE Approved
- Application Conditions
Pretreatment at Wastewater Treatment Plant Inlet
Automatic rotary bar screens are typically installed at the headworks or inlet channel of wastewater treatment plants to intercept large suspended solids and floating debris, protecting downstream equipment such as pumps, grit chambers, and biological reactors from blockage or damage.
Pump Station Screening & Protection
At sewage lift stations (e.g., municipal or industrial wastewater pump stations), bar screens at the inlet prevent large debris from entering the pumps, reducing clogging frequency and ensuring continuous and reliable pump operation.
Combined Water Treatment System Pretreatment
In combined or separated sewer systems, automatic screens can be placed at junction points to capture solids and operate automatically during high flows, enhancing system resilience.
Industrial Wastewater Pretreatment
In industrial wastewater applications such as pulp & paper, food processing, textiles, and electroplating, screening removes larger solids before biological or chemical treatment units, reducing load and improving overall efficiency.
Rural/Small Town Sewage Collection Systems
Installing automatic rotary bar screens at small wastewater collection canal outlets or pump inlets reduces manual cleaning, saves labor, and increases automation reliability in decentralized systems.
- Valve structure diagram


- Product Data Sheet

Testing Process
From raw materials to finished products, NORITE maintains 100% testing coverage, ensuring that every valve and pump you receive is built to last — safe, stable, and globally certified.

Pressure Testing
Each valve undergoes rigorous pressure and hydrostatic testing prior to shipment to verify body strength, sealing integrity, and pressure stability—ensuring zero leakage and long-term reliability in field operation.

Torque and Functional Testing
Confirming operating performance and precision.

Cycle Life Testing
Simulating long-term use under real working conditions.

Coating & Corrosion Resistance Testing
Validating surface protection and durability.
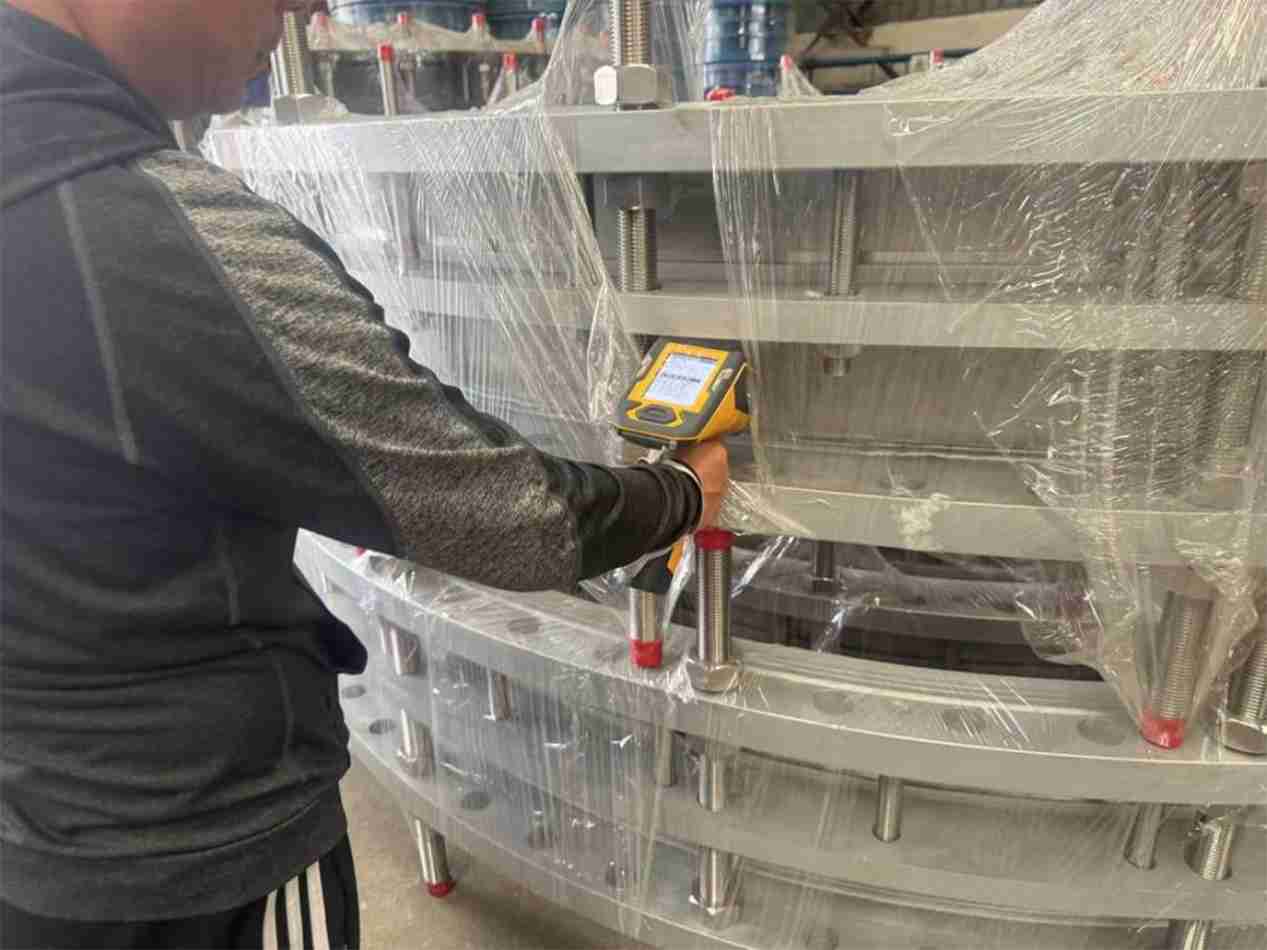
Dimensional & Material Analysis
Using spectrometers and coordinate measuring machines (CMM) for accuracy.
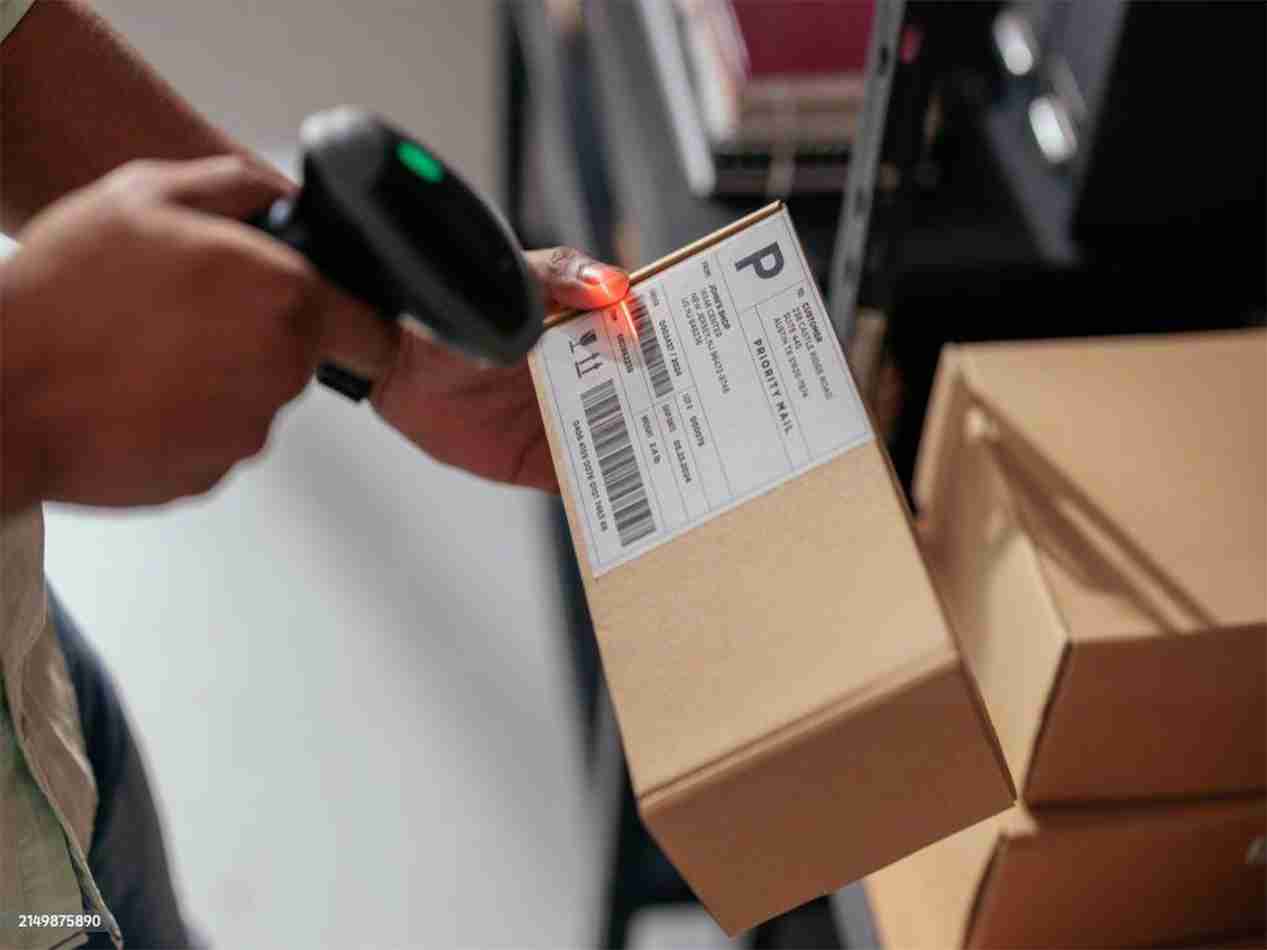
Traceability - Unique product code
Each product leaving our factory is accompanied by a full inspection report and a unique serial number, enabling full traceability and lifetime quality tracking.
Real Project Cases
Proven performance in critical applications worldwide – see our valves in action
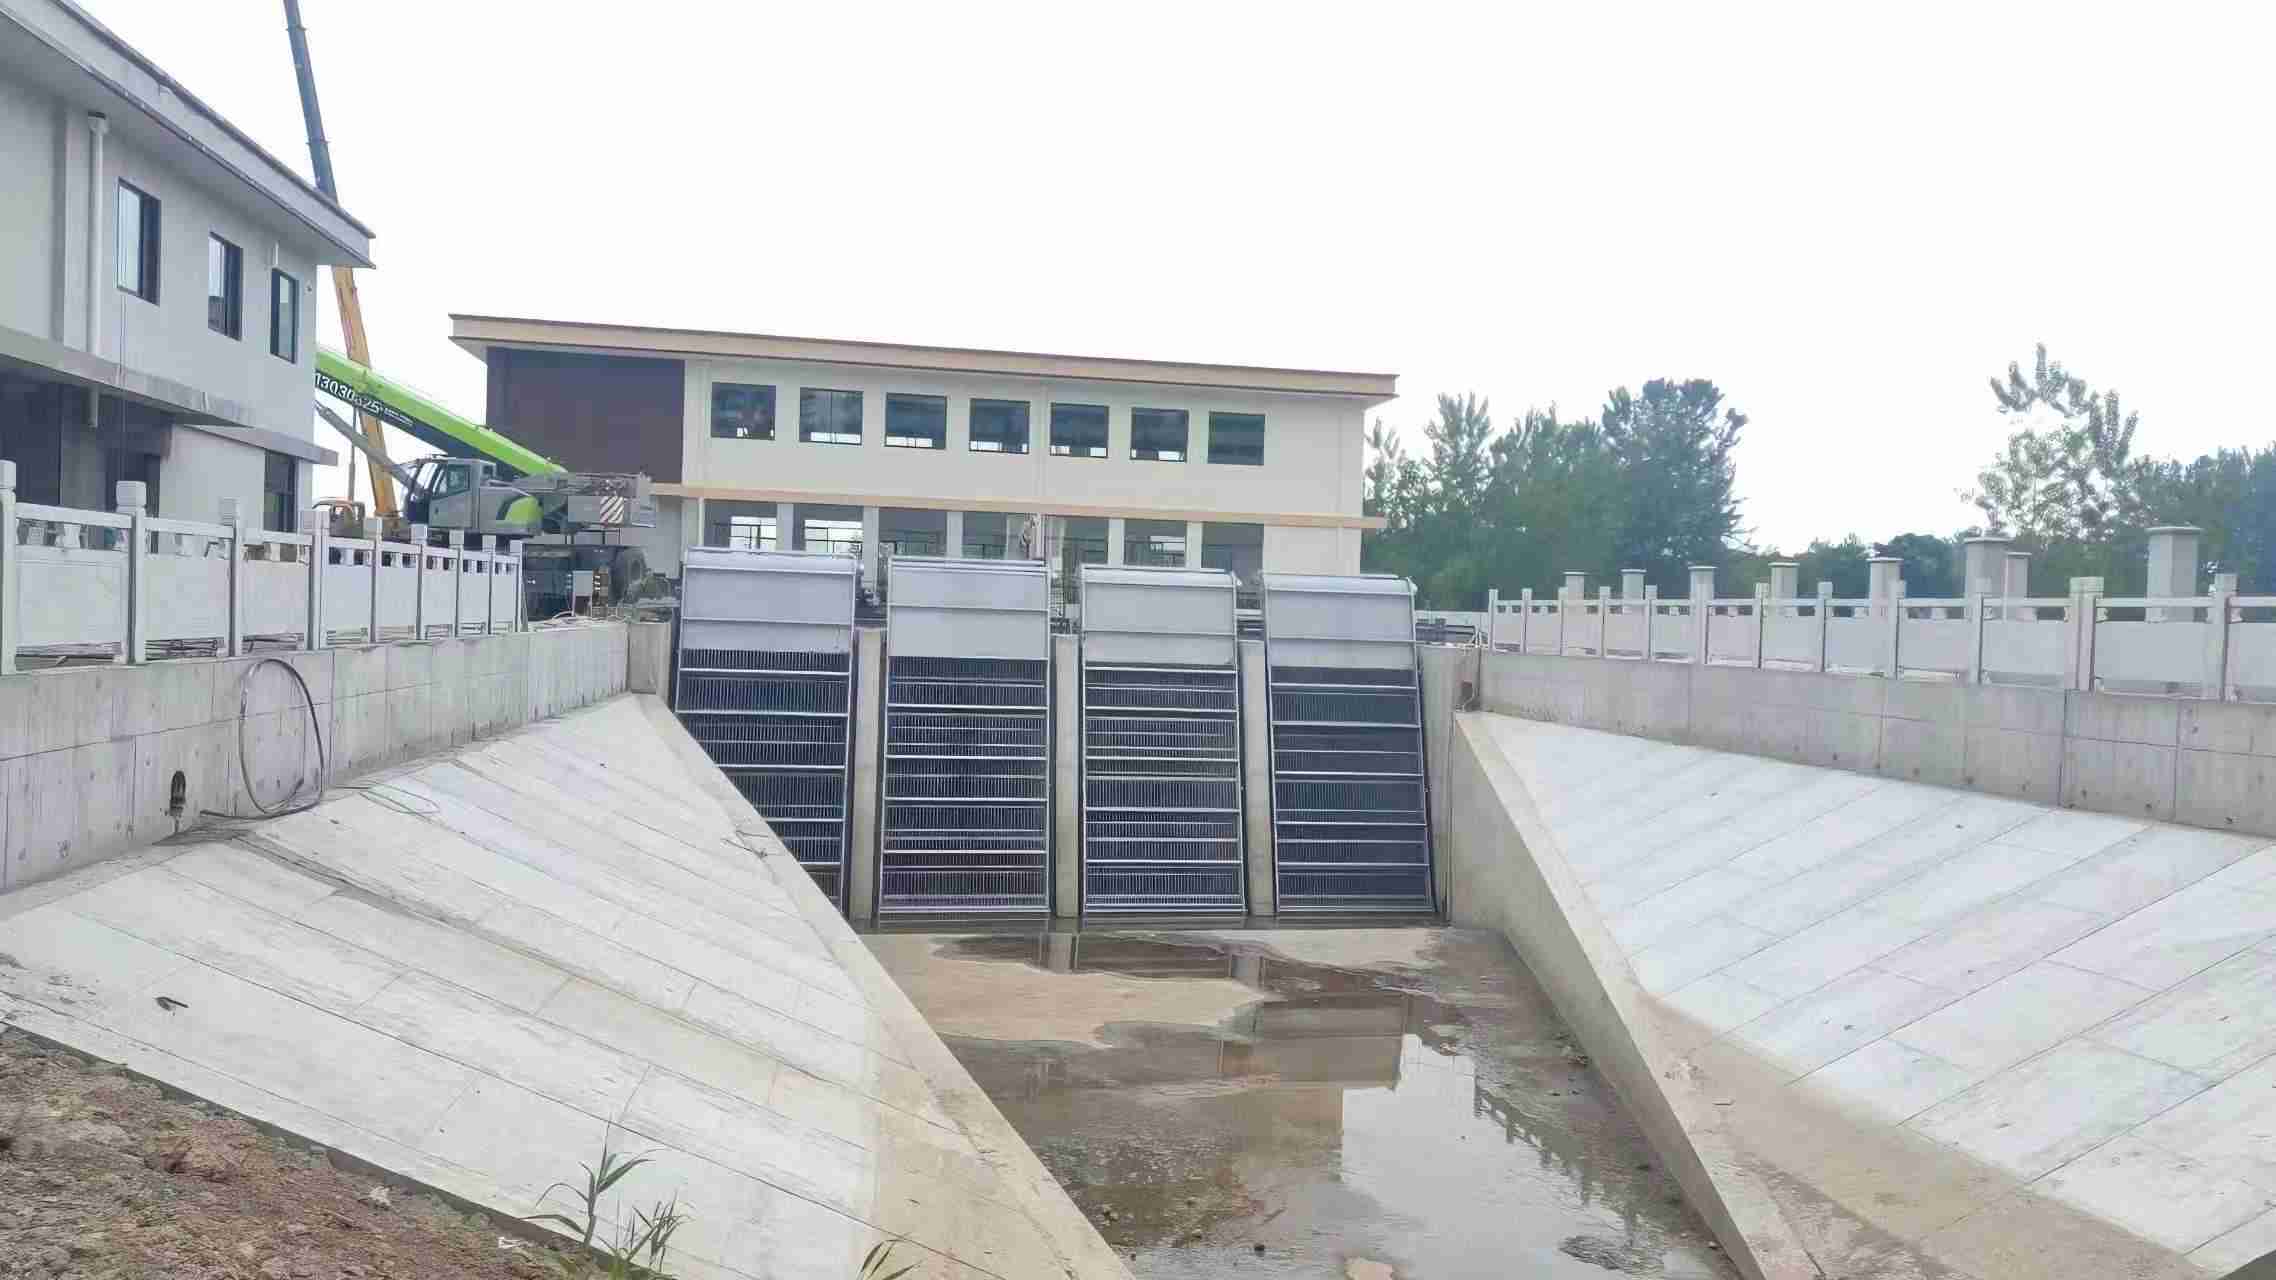
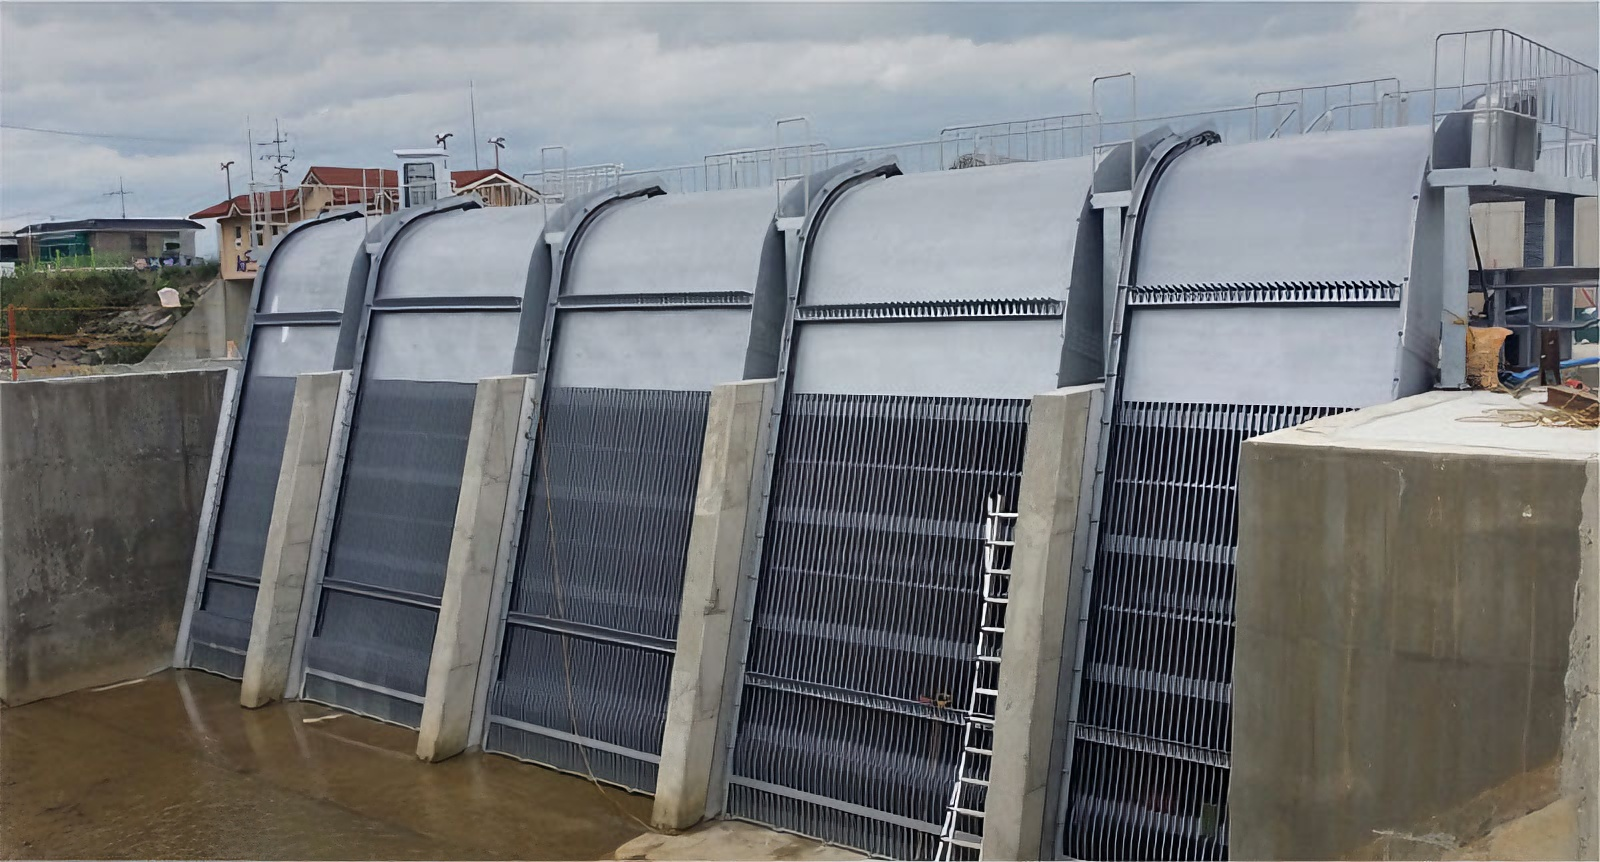
Ebaps Vila Velha
- Espirito Santo State, Brazil
Customer/Owner: “Estacǎo de Bombeamento de Áquas Pluviais
- Working conditions/Challenges:
This pumping station is a rainwater drainage pumping station. As part of the city ‘s large-scale drainage/flood control infrastructure, it is equipped with approximately 12 kilometers of closed drainage pipe galleries + 7 kilometers of anti-seepage channels.
- The type of equipment adopted:
We provide three 900QZB-315KW submersible mixed-flow pumps with a diameter of φ1400mm for this project, along with three 2*4.7m automatic rotary screen cleaners, eleven electric gates and five flap valves.
Key indicators: A grille screen is installed in the intake channel of the pumping station to intercept large particles of debris and floating garbage, reducing the frequency of pump inlet blockage, thereby lowering maintenance costs and enhancing the stability of the pumping station.
Get Your Custom Quote
Our technical experts will analyze your requirements and provide a tailored solution with detailed specifications and competitive pricing.