
Flow Control, Zero Compromise
From municipal water to industrial flow systems — total reliability starts here.
From deep wells to pipelines and wastewater treatment, Norite delivers efficiency, durability, and trust in every drop.
- 5-Year Warranty
- ISO 9001 Certified
- 24/7 Support


H41X Foot Check Valve
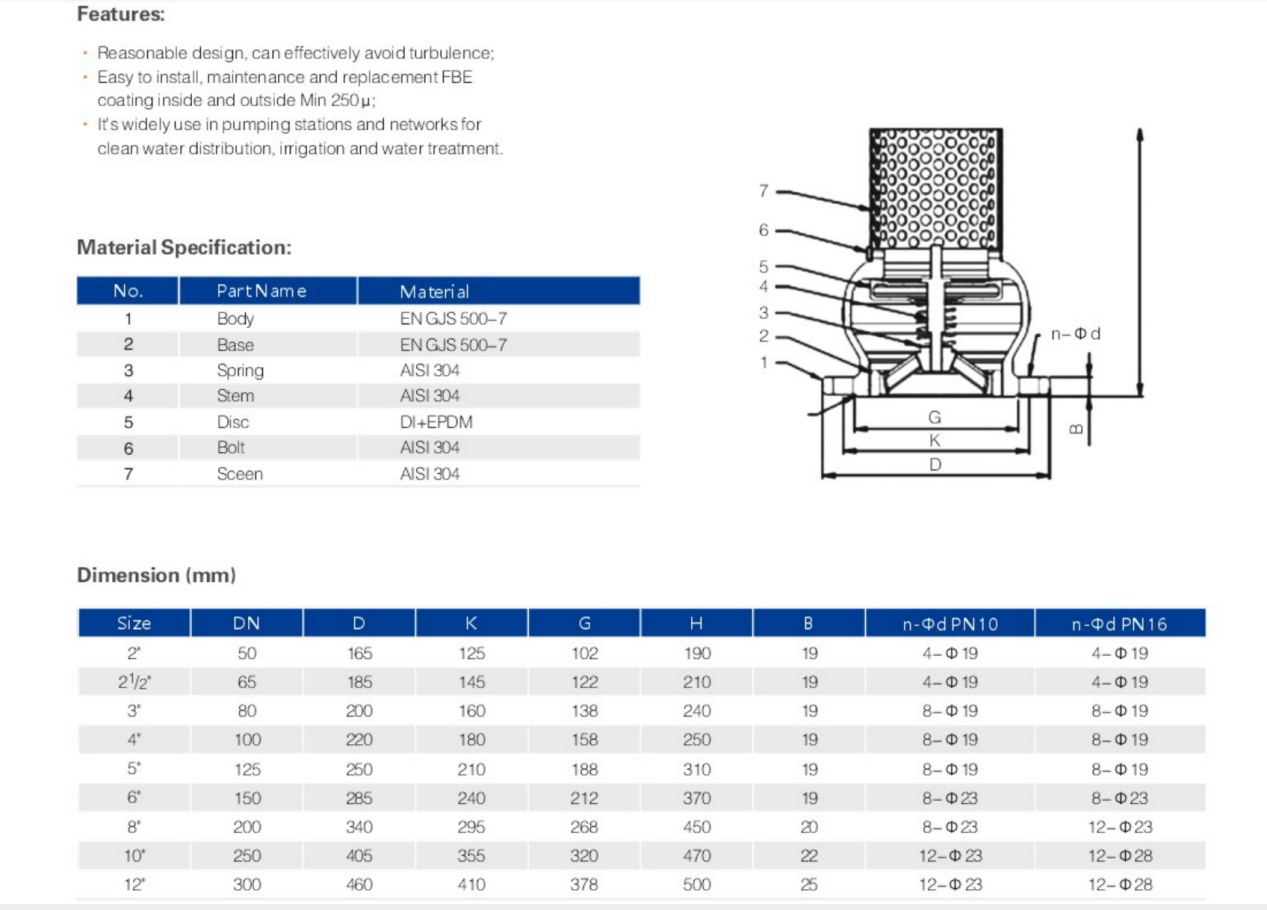
Integrated Strainer to Prevent Debris Entry into Pump Suction
Foot check valves are equipped with a builtin suctionend strainer to prevent large debris from entering the pump, reducing clogging and wear.
One-Way Flow Design to Maintain Pump Prime and Prevent Backflow
Installed at the suction line’s end, the foot valve allows upward flow into the pump but closes automatically if flow reverses, thereby preserving pump priming.
Suitable for Pump Inlets and Suction Lift Systems, Protecting Equipment
Ideal for well pumps, suction lift systems, pump station inlets and suction lines; protecting against dry-run, cavitation and reverse flow shock.
Robust Materials and Construction for Harsh Media Conditions
Available in stainless steel, galvanized steel, plastic or bronze bodies, with corrosion-resistant designs ideal for water with sand or wells.
Dedicated Suction-End Design, Compact Structure and Easy Maintenance
Designed specifically for pump suction ends, compact and usually installed vertically; screens are serviceable, and valve components can be replaced, simplifying maintenance.
Need custom specifications? Our engineers are ready to help.
Call: +86 15090163952 | Email: lisa@noritesolution.com
Proven Results That Drive Your Bottom Line
Real performance data from our Valve installations across critical industries worldwide

100% Pressure Tested
Tested under Class A sealing standard, across 10,000+ units.

20+ Years Lifespan
Proven performance in seawater, wastewater, and high-pressure pipelines.

8,000+ Valves Installed
Including power plants, municipal water systems, and industrial zones.

99.5% On-Time Delivery
Backed by lean production and strict QC.
Certifications & Standards


Technical Specifications
Engineered for optimal performance across a wide range of industrial applications
Model:
Size Range:
H41X
DN50– DN600, 2”-24”
Pressure Rating:
Standards:
EN 122334.EN1074
Media:
Max Temperature:
Water and neutral liquids
Body Material:
Filter screen:
Ductile Iron , WCB , Stainless Steel
Stainless steel
Stem Material:
Sealing:
Stainless steel
EPDM
Connection:
Certifications:
Flanged to EN1092-2,ANSI B16.5,BS4504
- Application Conditions
Pump Station Suction or Suction Lift Systems
Well Pumps / Shallow or Deep Well Extraction Systems
Water Supply / Irrigation Network Inlets
Water Sources with Solid Particulates
Pump House Inlets & Underground Suction Systems
- Installation Instructions


- Flow curve

- Valve size data sheet
Testing Process
From raw materials to finished products, NORITE maintains 100% testing coverage, ensuring that every valve and pump you receive is built to last — safe, stable, and globally certified.

Pressure Testing
Each valve undergoes rigorous pressure and hydrostatic testing prior to shipment to verify body strength, sealing integrity, and pressure stability—ensuring zero leakage and long-term reliability in field operation.

Torque and Functional Testing
Confirming operating performance and precision.

Cycle Life Testing
Simulating long-term use under real working conditions.

Coating & Corrosion Resistance Testing
Validating surface protection and durability.
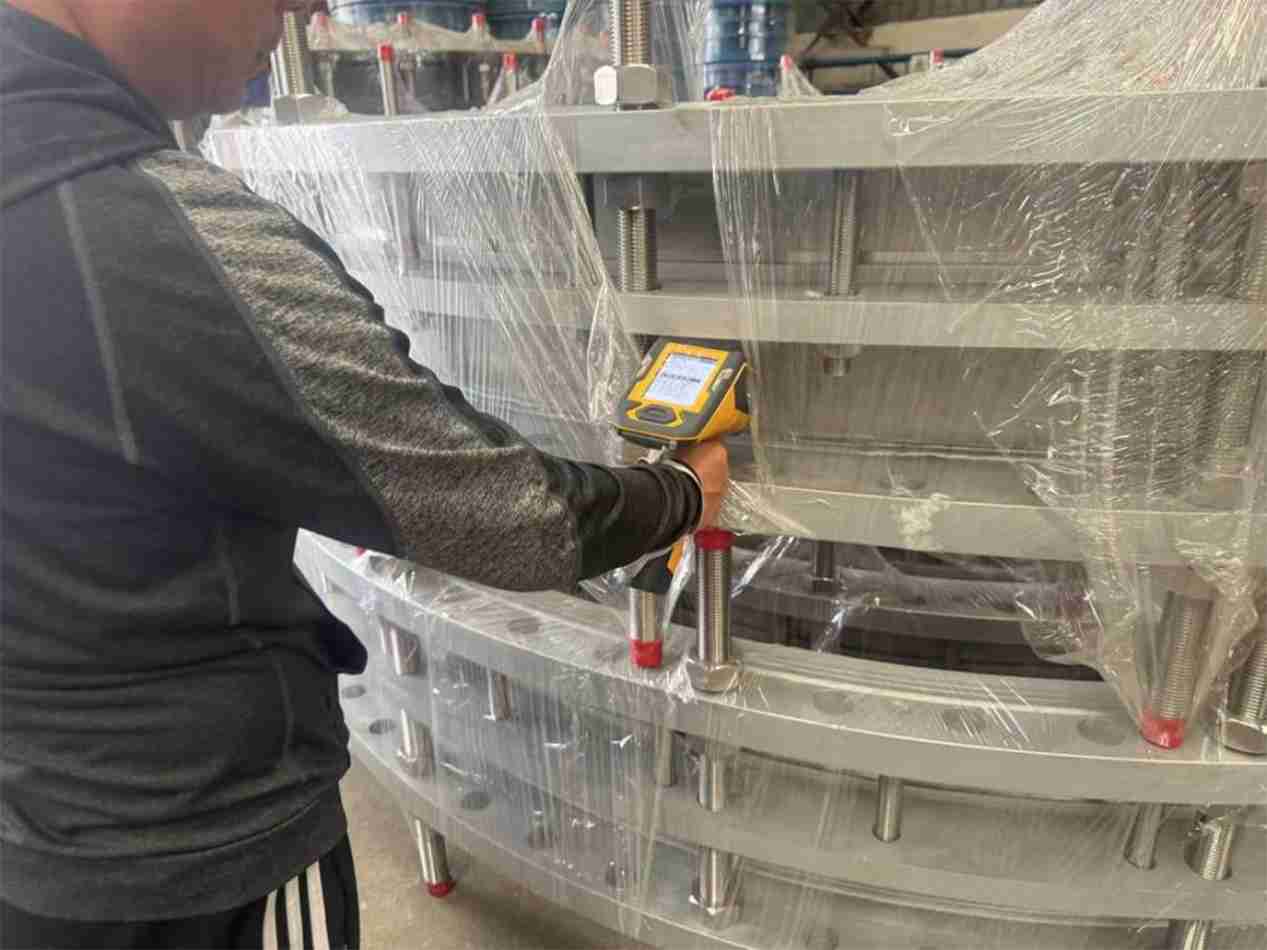
Dimensional & Material Analysis
Using spectrometers and coordinate measuring machines (CMM) for accuracy.
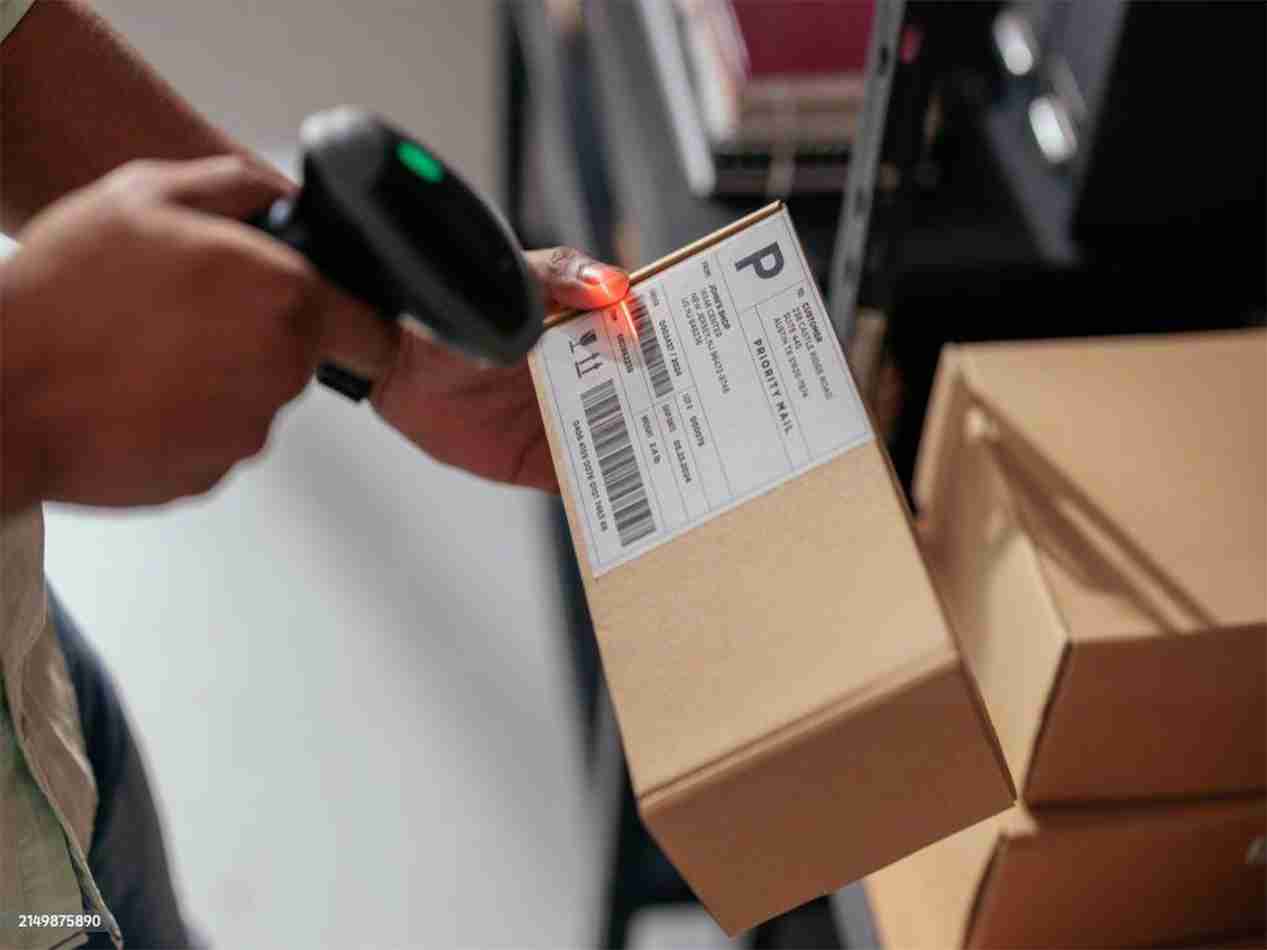
Traceability - Unique product code
Each product leaving our factory is accompanied by a full inspection report and a unique serial number, enabling full traceability and lifetime quality tracking.
Real Project Cases
Proven performance in critical applications worldwide – see our valves in action
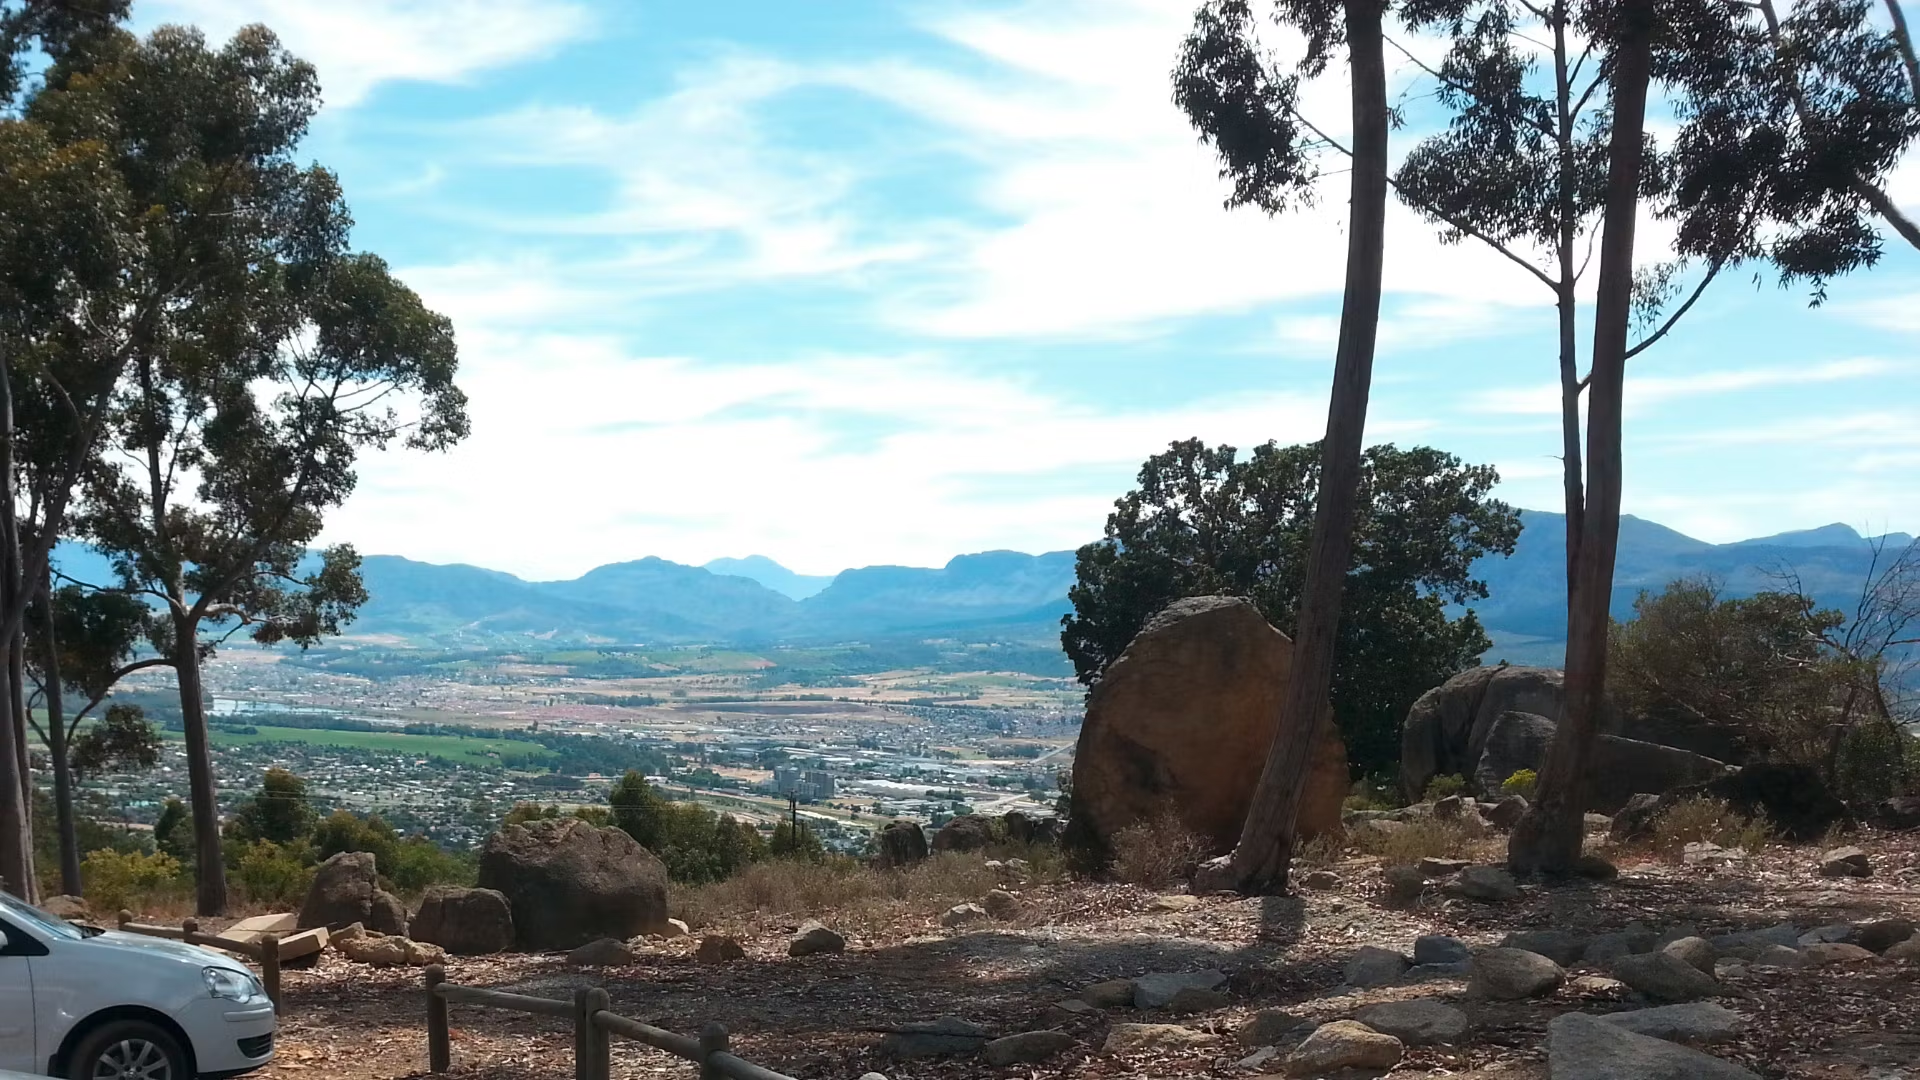
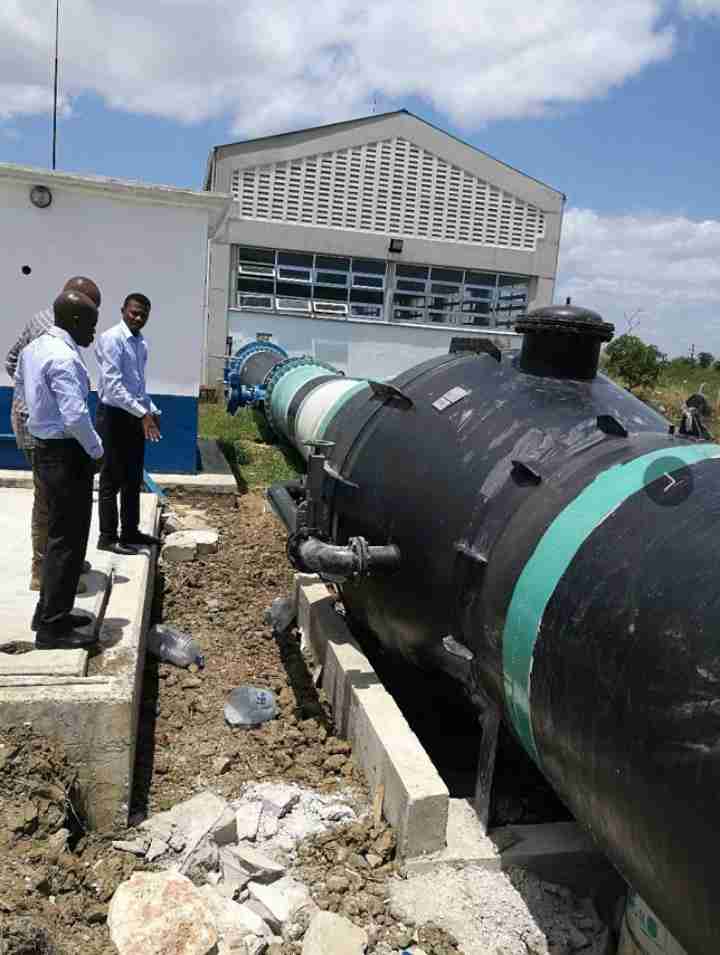
Drakenstein Meulwater Water Treatment Works
- South African
Customer/Owner: South African Water Company
- Working conditions/Challenges:
This project focuses on water plant monitoring, reducing leakage and improving the efficiency of the pipeline network
- The type of equipment adopted:
We provided a complete set of products including check valves, gate valves and joints for the upgrade of this pumping station system.
Key indicators: In water supply, sewage treatment and fire protection systems, Check Valve are important components for preventing backflow and protecting pumping stations
Get Your Custom Quote
Our technical experts will analyze your requirements and provide a tailored solution with detailed specifications and competitive pricing.