
Flow Control, Zero Compromise
From municipal water to industrial flow systems — total reliability starts here.
From deep wells to pipelines and wastewater treatment, Norite delivers efficiency, durability, and trust in every drop.
- 5-Year Warranty
- ISO 9001 Certified
- 24/7 Support


Q367F Welded Ball Valve
Fully Welded Body – Leak-Free Integrity
Integral welded body design with no flange or bolted joints, fundamentally eliminates leakage risks caused by aging gaskets or loose bolts.
Superior Sealing - Designed for Gas Pipeline Safety
Engineered for natural gas networks with high-performance sealing to prevent gas leakage and ensure safe, energy-efficient operations.
Pressure & Corrosion Resistance - For Harsh Environments
Built to withstand high pressure, underground burial, and corrosive conditions, ideal for urban and long-distance transmission lines.
Full Bore Design - Minimal Pressure Drop
Full bore passage ensures unimpeded flow with minimal pressure loss, maximizing pipeline transmission capacity.
Low Maintenance - Built for Longevity
Simplified construction reduces failure points and maintenance, ideal for long-term buried or remote installations in gas systems.
Need custom specifications? Our engineers are ready to help.
Call: +86 15090163952 | Email: lisa@noritesolution.com
Proven Results That Drive Your Bottom Line
Real performance data from our Valve installations across critical industries worldwide

100% Pressure Tested
Tested under Class A sealing standard, across 10,000+ units.

20+ Years Lifespan
Proven performance in seawater, wastewater, and high-pressure pipelines.

8,000+ Valves Installed
Including power plants, municipal water systems, and industrial zones.

99.5% On-Time Delivery
Backed by lean production and strict QC.
Certifications & Standards


Technical Specifications
Engineered for optimal performance across a wide range of industrial applications
Model:
Size Range:
Q367F
DN50 – DN1200,2”-48”
Pressure Rating:
Standards:
PN10 -PN160,150LB-900LB
API6D,ASME B16.34
Media:
Max Temperature:
Petroleum, Natural Gas
Body Material:
Ball Material:
A105,LF2,F304
A105+ENP,LF2+ENP,F304
Stem Material:
Sealing:
Stainless steel
PTFE/PEEK
Connection:
Certifications:
Flanged to EN1092-2,ANSI B16.5,BS4504
- Application Conditions
Municipal Water Supply & Drainage Systems
Soft-seal gate valves are widely used in municipal water supply networks, stormwater drainage and sewage treatment plant pipelines because of their excellent sealing performance and minimal flow resistance.
Buried Pipelines & Underground Infrastructure
In buried pipelines and underground infrastructure—such as rural water networks, sewage mains and sub-surface utilities—soft-seal gate valves provide reliable shut-off and sealing under constrained installation conditions.
Low-to-Moderate Temperature & Pressure Systems
Suitable for systems where the fluid temperature is typically below ~80 °C and pressure is moderate (e.g., PN10–PN25), soft-seal gate valves excel in tight shut-off and minimal leakage.
Clean or Slightly Particulate-Bearing Fluids
Due to elastic sealing materials and groove-free seat design, these valves are well suited for clean water, municipal sewage or general service pipelines—not ideal for heavy solids, high temperature or strongly corrosive fluids.
Heating, HVAC, Fire-Water Systems
In heating systems, HVAC loops or fire-protection mains, soft-seal gate valves serve as reliable cut-off valves where low opening torque and leak-tight shut-off are valued.
- Valve structure diagram
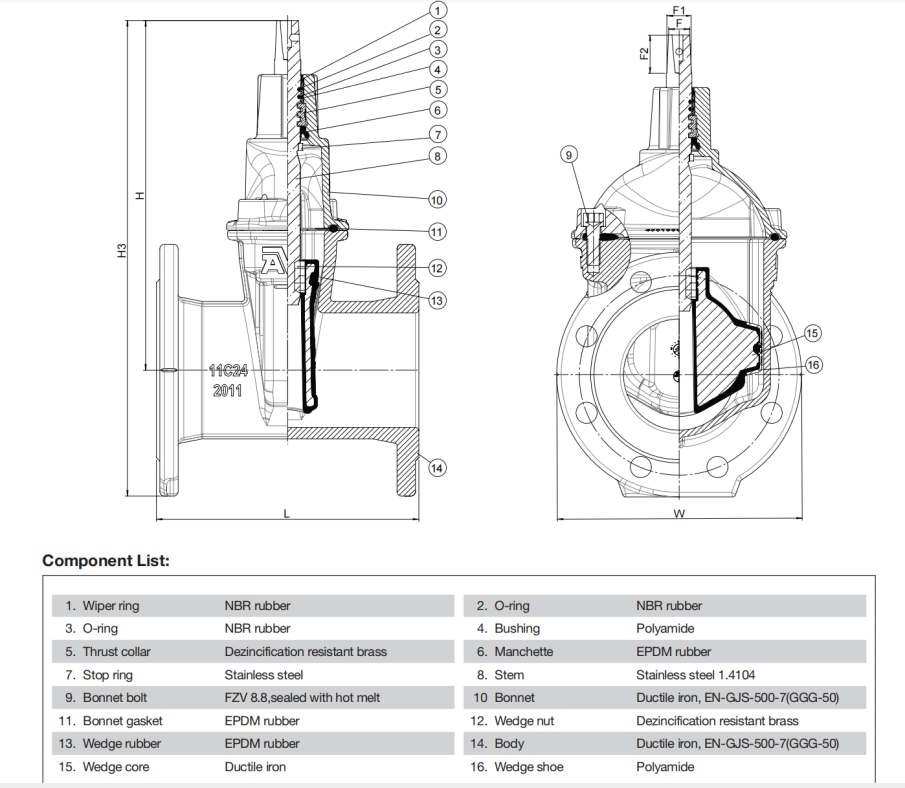
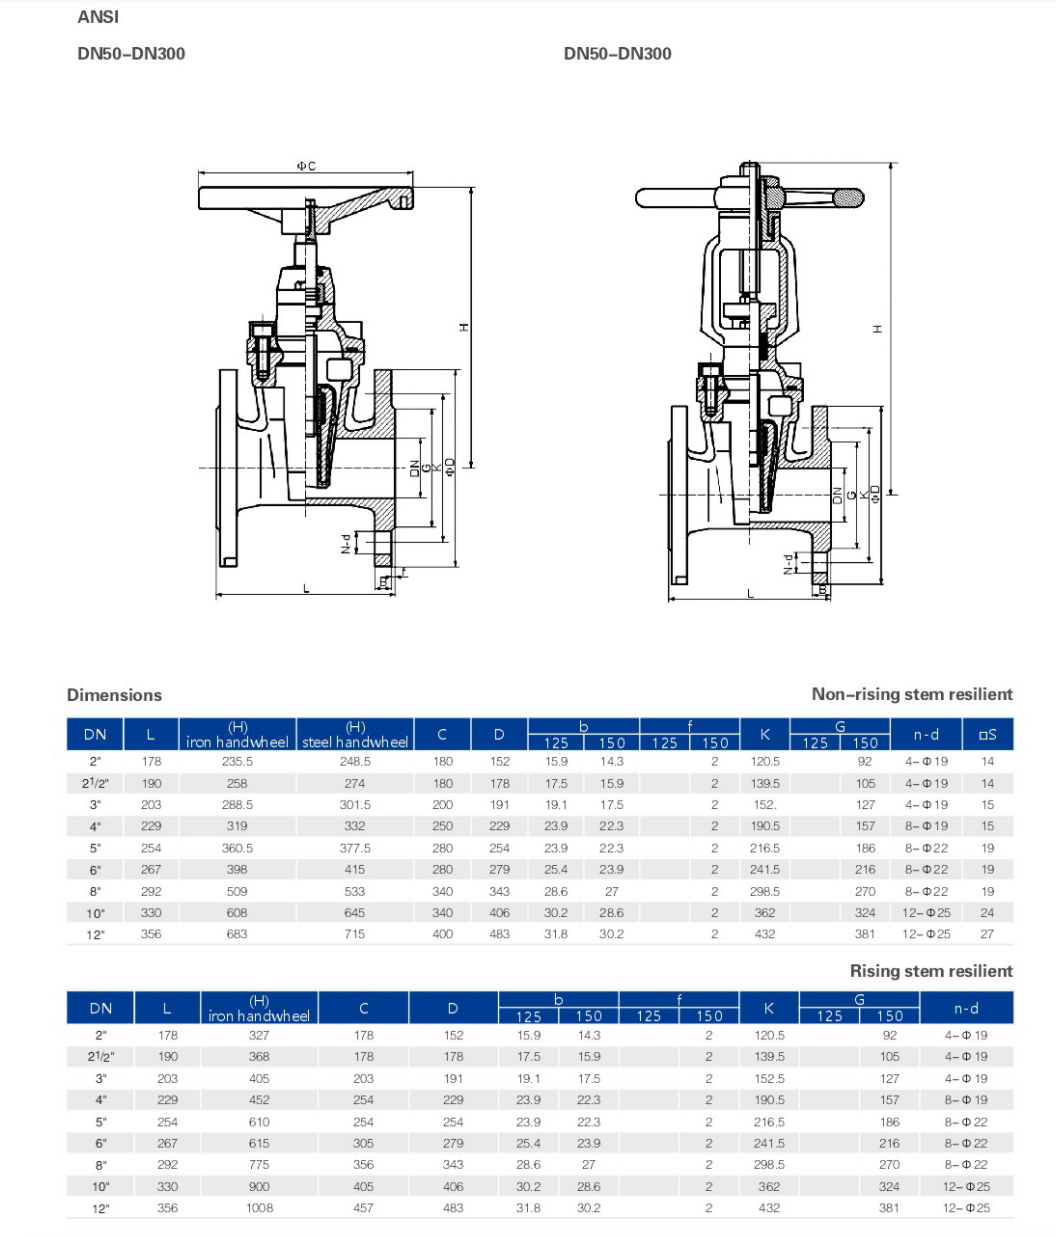
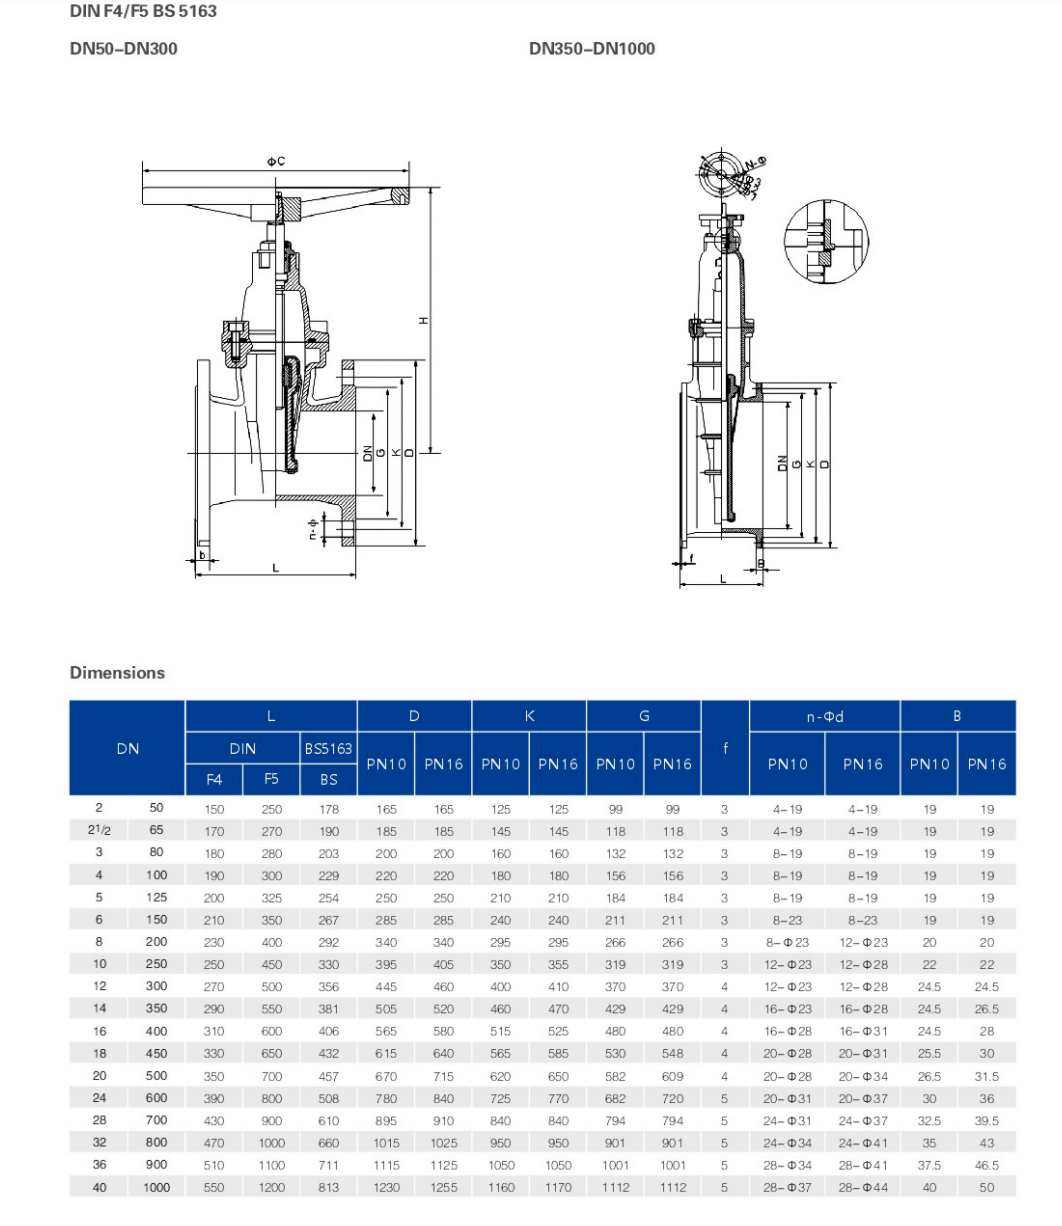
- Valve size data sheet
Testing Process
From raw materials to finished products, NORITE maintains 100% testing coverage, ensuring that every valve and pump you receive is built to last — safe, stable, and globally certified.

Pressure Testing
Each valve undergoes rigorous pressure and hydrostatic testing prior to shipment to verify body strength, sealing integrity, and pressure stability—ensuring zero leakage and long-term reliability in field operation.

Torque and Functional Testing
Confirming operating performance and precision.

Cycle Life Testing
Simulating long-term use under real working conditions.

Coating & Corrosion Resistance Testing
Validating surface protection and durability.
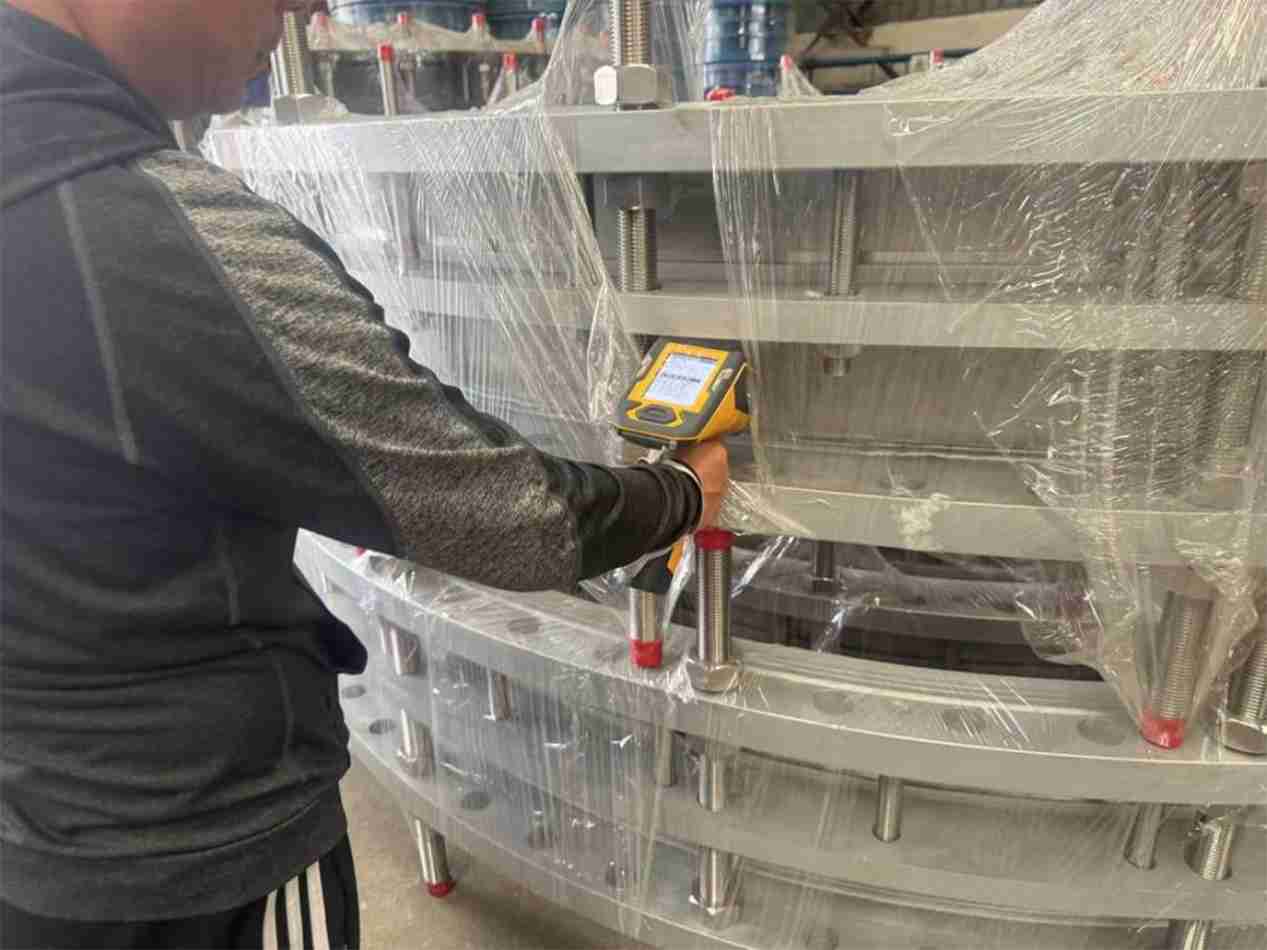
Dimensional & Material Analysis
Using spectrometers and coordinate measuring machines (CMM) for accuracy.
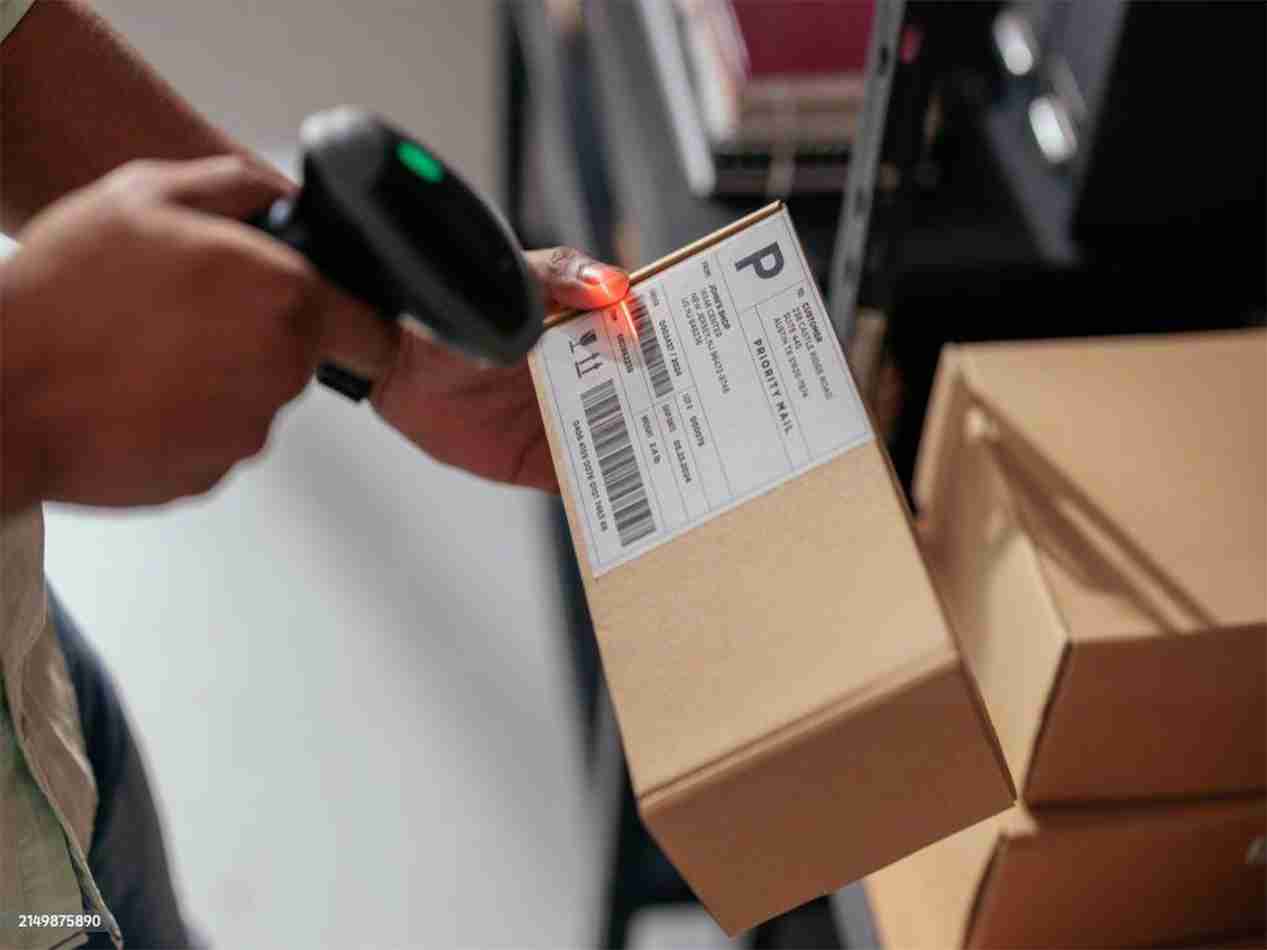
Traceability - Unique product code
Each product leaving our factory is accompanied by a full inspection report and a unique serial number, enabling full traceability and lifetime quality tracking.
Real Project Cases
Proven performance in critical applications worldwide – see our valves in action
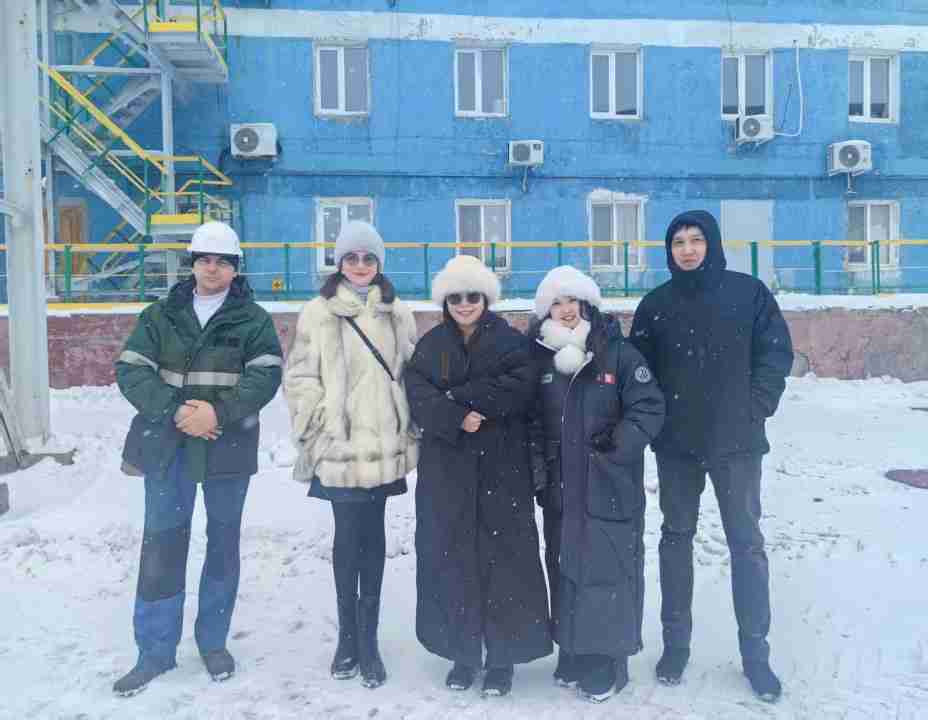

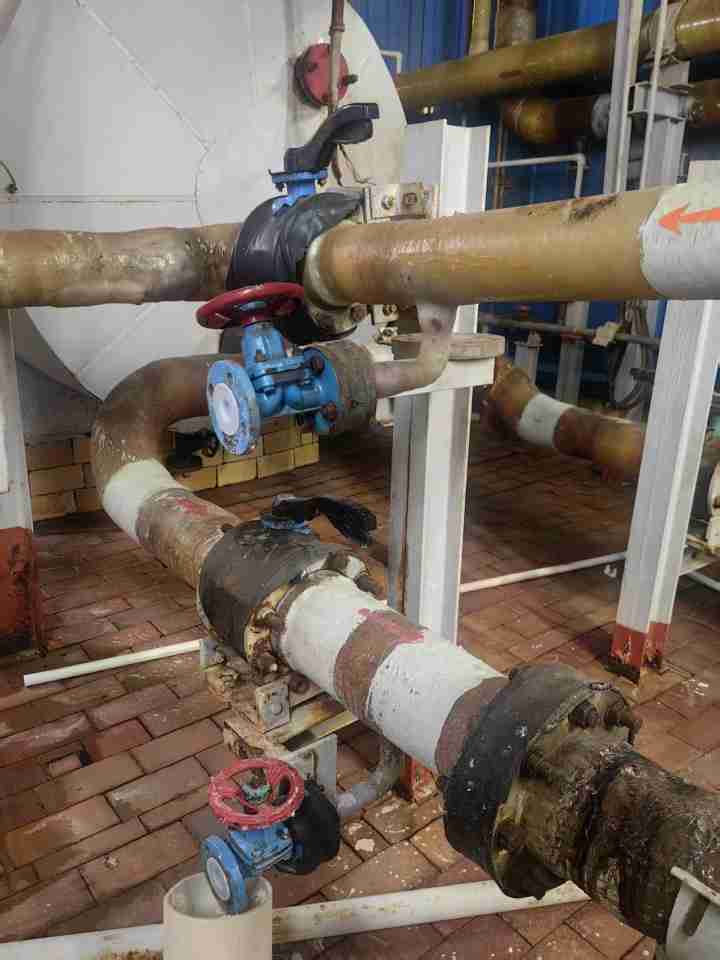
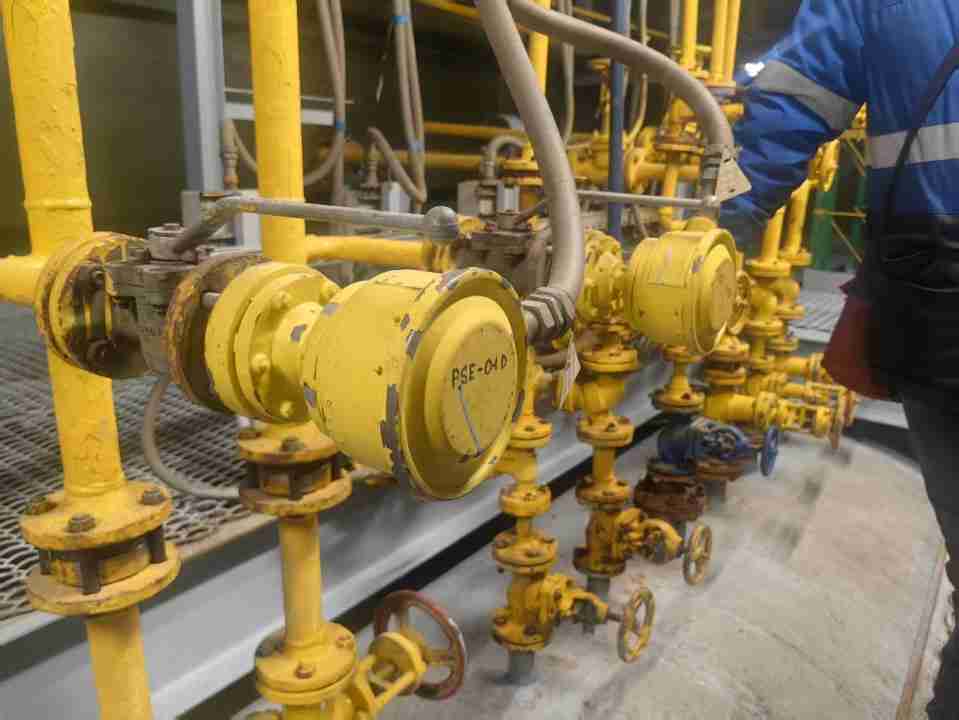
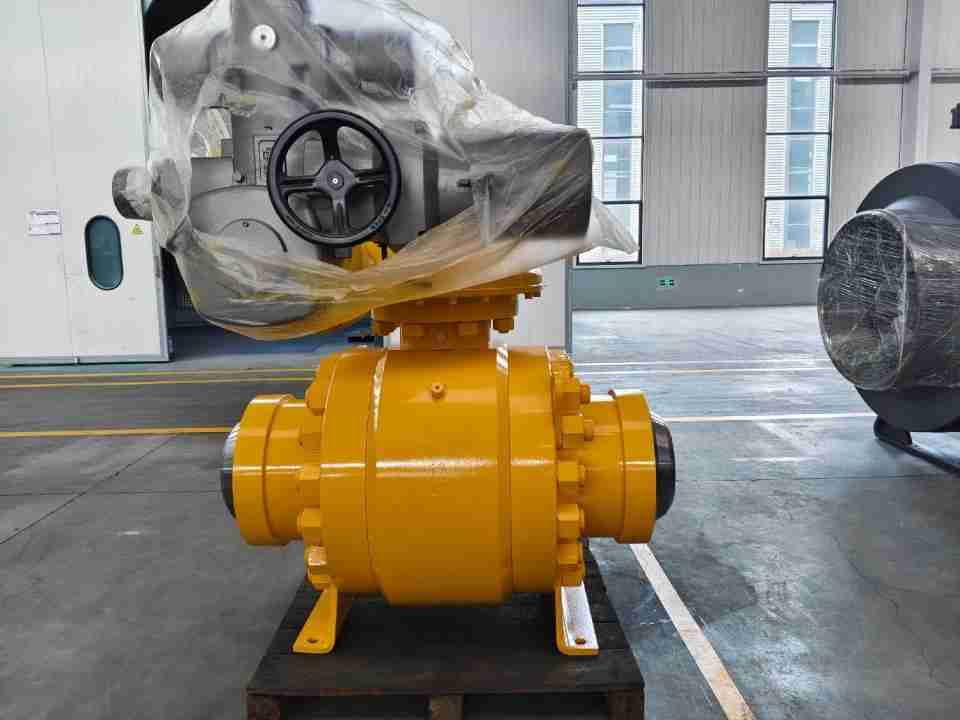
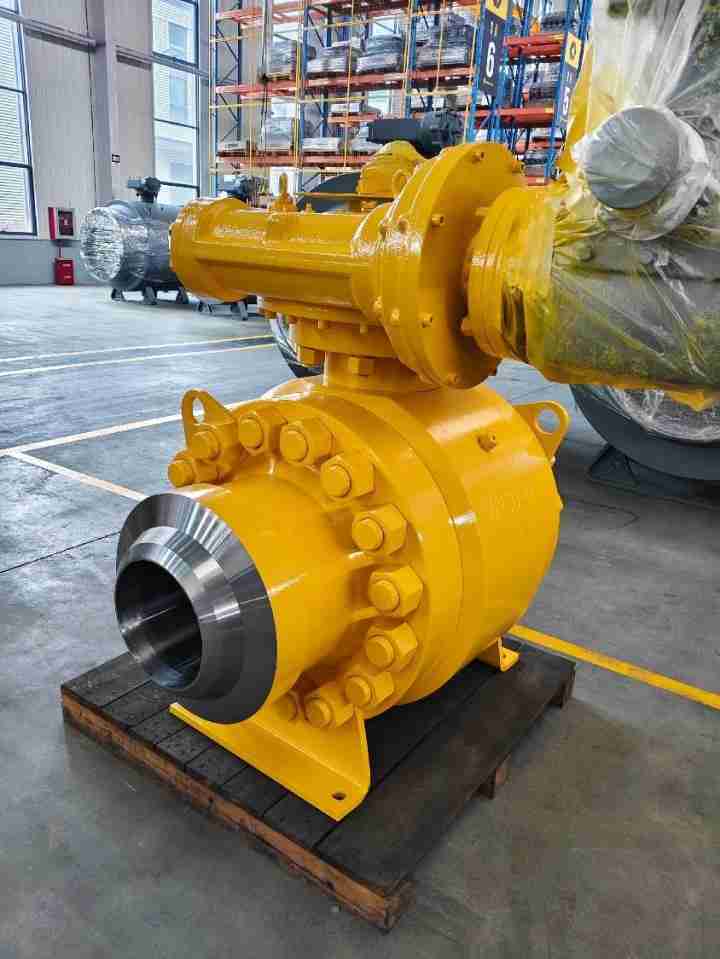
UZBEKISTAN Chemical Project
- North South Interconnector Pipeline
Customer/Owner: FARG’ONAAZOT chemical factory
- Working conditions/Challenges:
Farg’onaazot, the second largest chemical factory in UZ.Their oil and gas pipelines require a large number of high-pressure valves. Previously, the valves often malfunctioned, causing equipment to shut down, and the product lifespan was less than one year.
- The type of equipment adopted:
We have been cooperating since 2023, providing them with high-quality high-pressure valves, including high-pressure ball valves, fluorine-lined valves and other products.
Key indicators: After our products were installed in the pipeline, they operated smoothly. In 2024, we conducted an after-sales follow-up visit to the customer’s factory, and the customer company expressed high praise for our products.
Get Your Custom Quote
Our technical experts will analyze your requirements and provide a tailored solution with detailed specifications and competitive pricing.