
Z45X Resilient Seated Gate Valve
High-Performance Soft Seal Gate Valve for Municipal Water & Wastewater Systems
Engineered for zero-leakage performance, the Norite Z45X series features a GGG50 ductile iron body and EPDM fully vulcanized wedge. Designed to DIN 3352 / BS 5163 standards for long-term durability in industrial pipelines.
- 5-Year Warranty
- ISO 9001 Certified
- 24/7 Support


Core Advantages of Z45X Resilient Seated Gate Valves
Class A Zero-Leakage Sealing
The Z45X series achieves Class A sealing through a precision-engineered triple stem system and a fully vulcanized EPDM wedge. This ensures 100% airtight performance in high-pressure water networks.
In-Line Maintenance & Seal Replacement
Designed for efficiency, the resilient seated gate valve allows for sealing component replacement while fully open and under pressure. No need to dismantle from the pipeline, significantly reducing downtime.
Full Bore Design for Optimal Flow
Our Z45X valve features a smooth, full-bore passage with no hollow cavities. This prevents debris accumulation and minimizes pressure loss, ensuring a self-cleaning, hygienic flow.
GGG50 Ductile Iron & Epoxy Coating
The GGG50 ductile iron body is protected by a high-grade epoxy coating (min. 250μm). All internal parts are rubber-lined or stainless steel, making this soft seal gate valve ideal for harsh environments.
Flexible Actuation & Operation
Supports multiple operation modes including handwheel, gear box, electric actuator, or extension spindle. The Z45X is adaptable to various installation depths and remote control requirements.
Need custom specifications? Our engineers are ready to help.
Call: +86 15090163952 | Email: lisa@noritesolution.com
Certified Reliability: Z45X Resilient Seated Gate Valve Performance
Field-proven data from Norite valve installations in municipal water and industrial projects worldwide.

100% Pressure Tested
Every Z45X Resilient Seated Gate Valve undergoes rigorous factory hydrostatic testing to ensure reliable sealing performance before shipment.

20+ Years Lifespan
Our soft seal gate valves are built with high-grade materials and epoxy coating for maximum corrosion resistance in harsh wastewater environments.

8,000+ Valves Installed
The Norite Z45X series is a proven solution in 50+ countries, supporting critical infrastructure, irrigation, and industrial pipelines worldwide.

99.5% On-Time Delivery
We ensure timely fulfillment of your resilient seated gate valve orders through integrated manufacturing and strict quality control processes.
Certifications & Standards


Technical Specifications
Engineered for optimal performance across a wide range of industrial applications
Model:
Size Range:
Z45X
DN50 – DN1200,2”-48”
Pressure Rating:
Standards:
150LB;200PSI/250PSI
/300PSI
EN 1074-1/2,BS5163,AWWA C509/C515
Media:
Max Temperature:
Drinking water and neutral liquids
Body Material:
Wedge Material:
EN-GJS-500-7 (GGG-50)
Ductile iron core fully vulcanized with EPDM rubber
Stem Material:
Sealing:
EPDM / NBR
Connection:
Certifications:
Flanged to EN1092-2,ANSI B16.5,BS4504
- Application Conditions
Municipal Water Supply & Drainage Systems
Soft-seal gate valves are widely used in municipal water supply networks, stormwater drainage and sewage treatment plant pipelines because of their excellent sealing performance and minimal flow resistance.
Buried Pipelines & Underground Infrastructure
In buried pipelines and underground infrastructure—such as rural water networks, sewage mains and sub-surface utilities—soft-seal gate valves provide reliable shut-off and sealing under constrained installation conditions.
Low-to-Moderate Temperature & Pressure Systems
Suitable for systems where the fluid temperature is typically below ~80 °C and pressure is moderate (e.g., PN10–PN25), soft-seal gate valves excel in tight shut-off and minimal leakage.
Clean or Slightly Particulate-Bearing Fluids
Due to elastic sealing materials and groove-free seat design, these valves are well suited for clean water, municipal sewage or general service pipelines—not ideal for heavy solids, high temperature or strongly corrosive fluids.
Heating, HVAC, Fire-Water Systems
In heating systems, HVAC loops or fire-protection mains, soft-seal gate valves serve as reliable cut-off valves where low opening torque and leak-tight shut-off are valued.
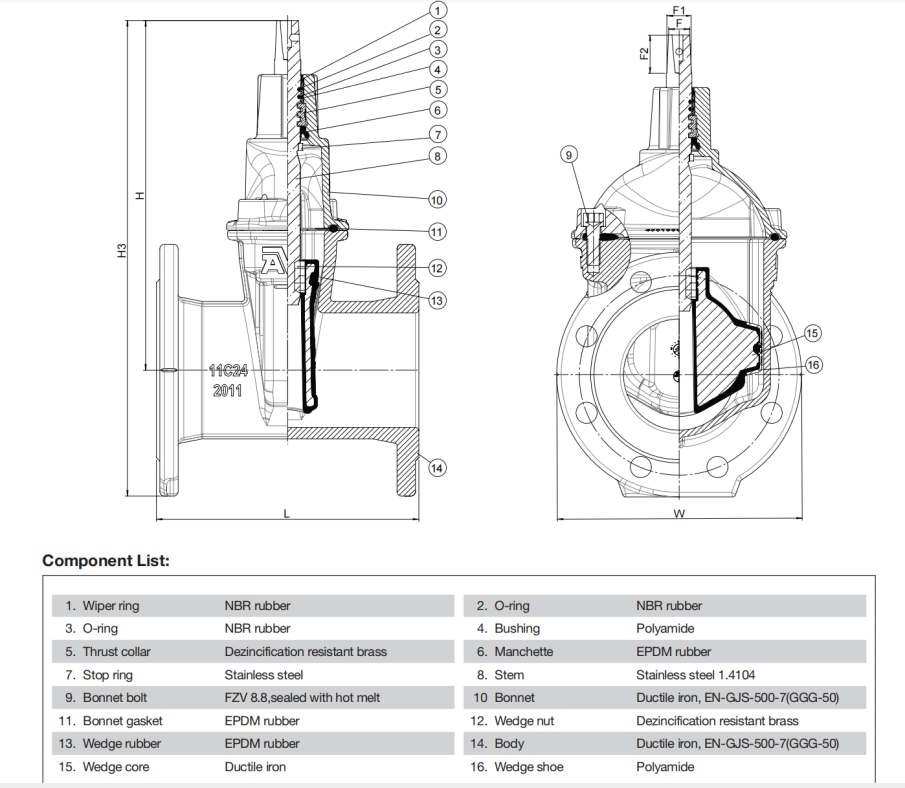
- Valve structure diagram
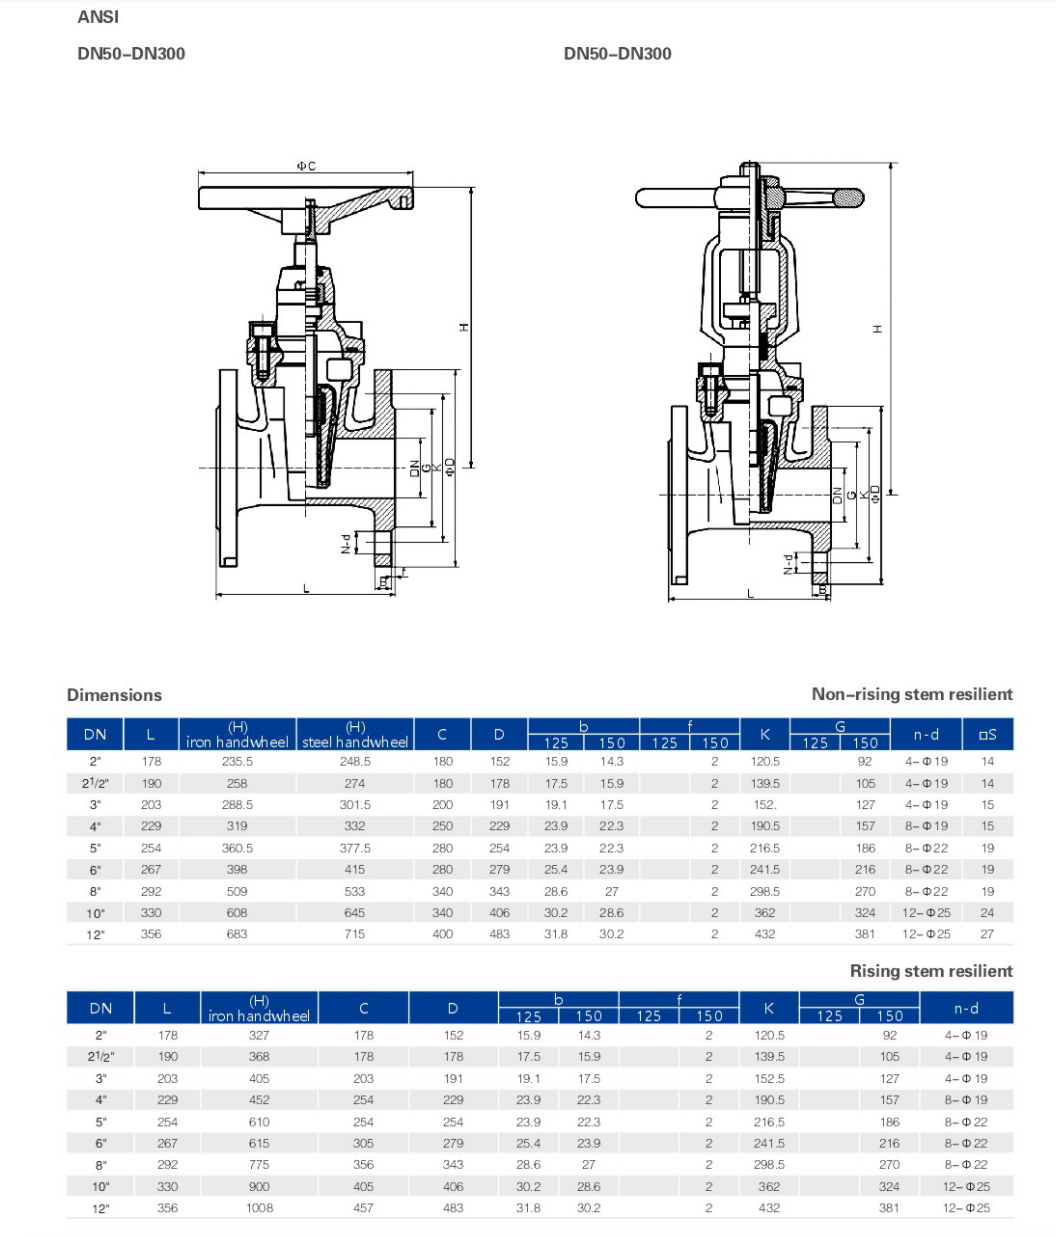
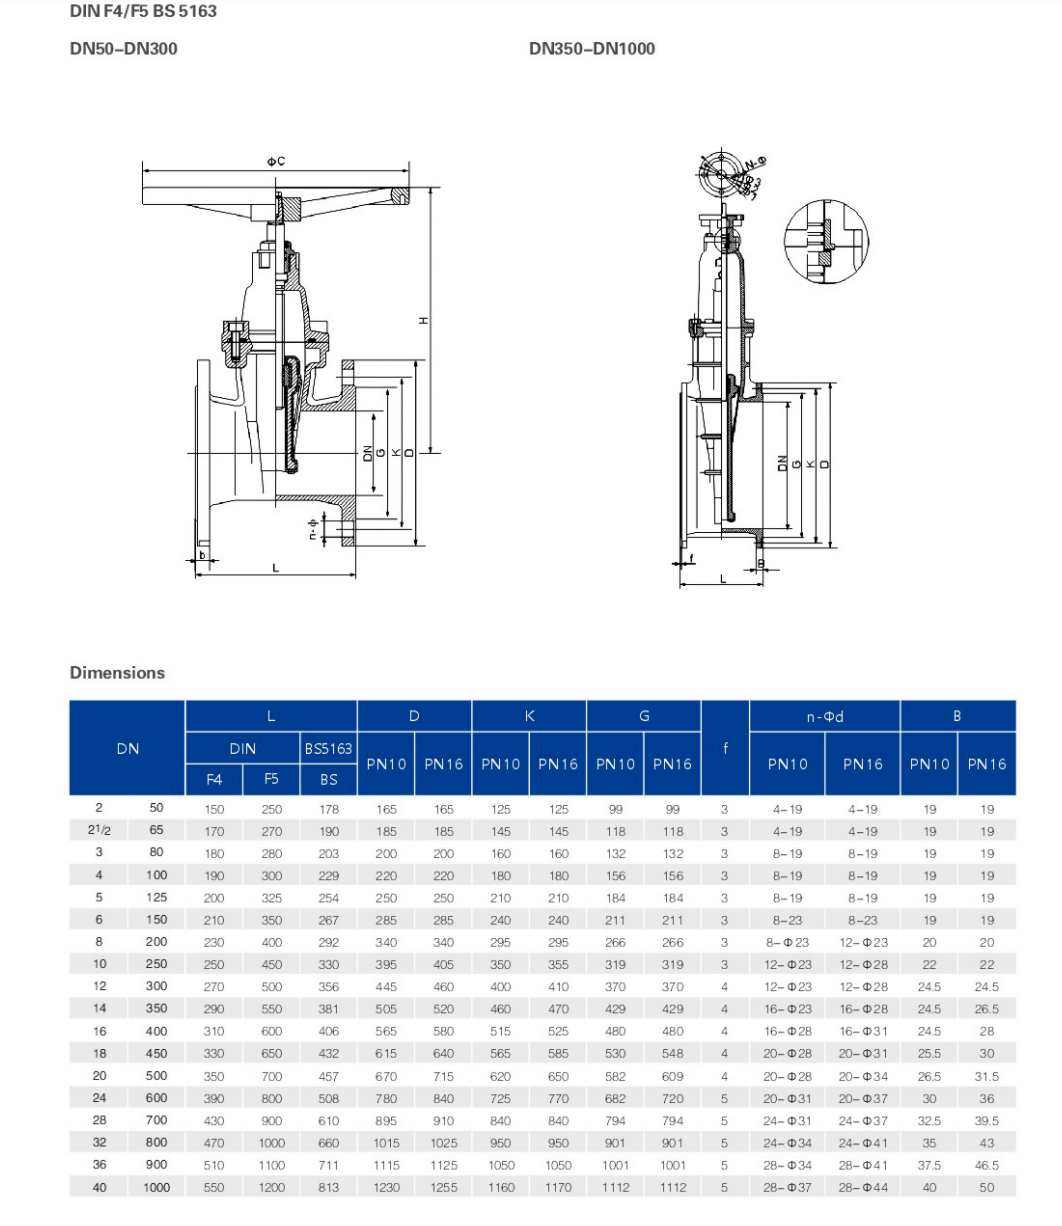
- Valve size data sheet
Rigorous Testing Process for Z45X Resilient Seated Gate Valves
From raw material selection to final hydraulic testing, NORITE ensures that every Z45X series valve meets international standards for safety and reliability.

Pressure Testing
Each Z45X Resilient Seated Gate Valve undergoes rigorous pressure testing to verify body strength and sealing integrity, ensuring 100% zero-leakage performance under high-pressure conditions.

Torque and Functional Testing
We verify the opening and closing torque of every Z45X valve to ensure smooth operation and precise flow control, even after long-term installation in water systems.

Cycle Life Testing
Our resilient seated gate valves are tested for thousands of cycles to simulate decades of real-world use, ensuring the EPDM wedge maintains its shape and sealing capability.

Coating & Corrosion Resistance Testing
We measure the epoxy resin coating (min. 250μm) on the Z45X body to guarantee superior corrosion resistance and compliance with drinking water safety standards (WRAS/ACS).
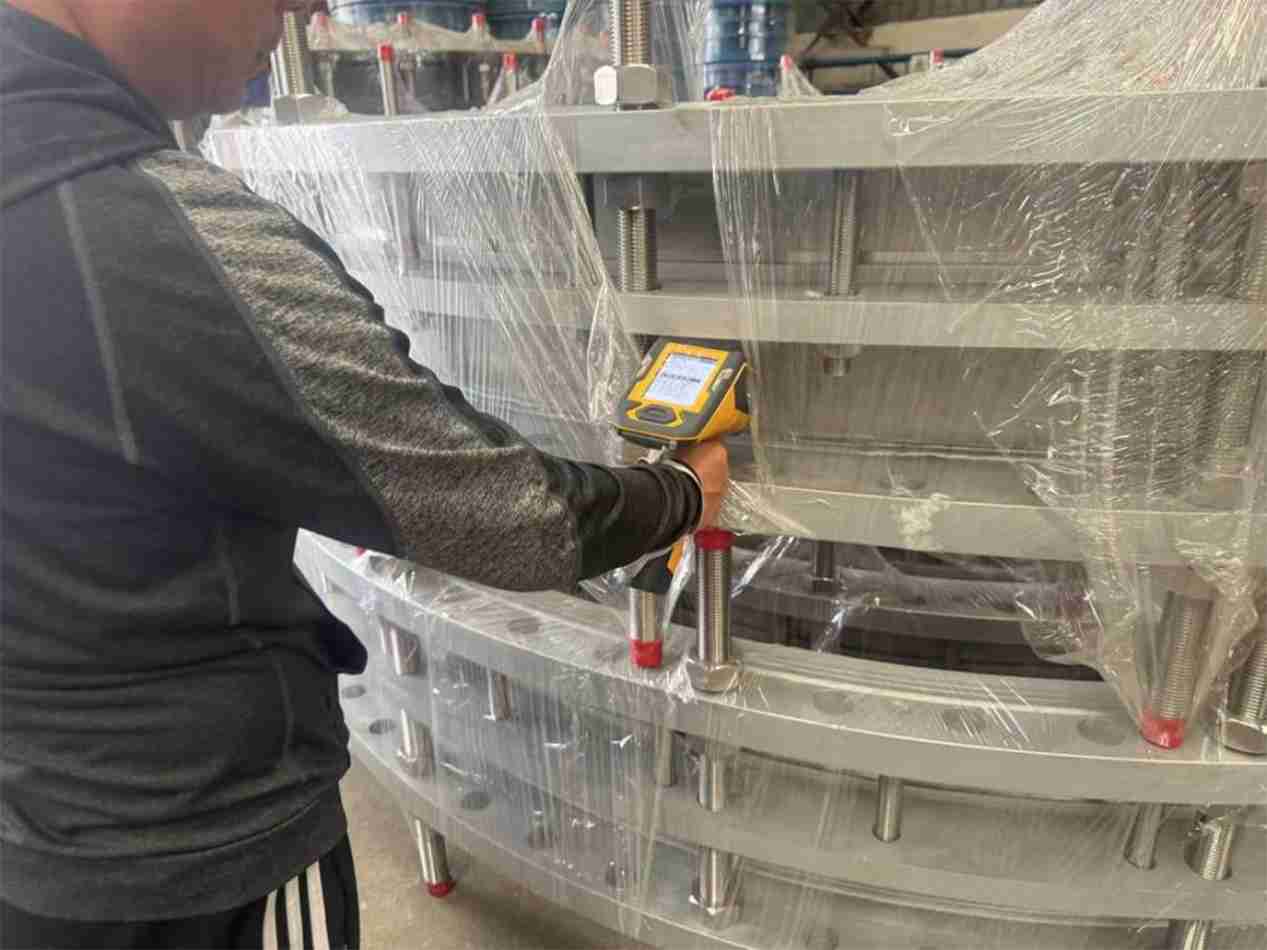
Dimensional & Material Analysis
Using advanced spectrometers, we verify the chemical composition of the GGG50 ductile iron to ensure the structural durability and impact resistance of every soft seal gate valve.
Traceability - Unique product code
Every Norite Z45X valve is assigned a unique tracking code and inspection report, allowing for full lifecycle quality tracking from raw material to final installation.
Global Success Cases
Proven Performance: Z45X Resilient Seated Gate Valves in the Field


The Mlooka Irrigation Project
- Mlooka, Malawi
Customer/Owner: Ministry of Agriculture, Malawi
- Working conditions/Challenges:
The Mlooka Irrigation Scheme is a flagship initiative led by the Government of Malawi to strengthen agricultural output and improve rural livelihoods. Covering a large farming area, the project aims to build a modern, efficient irrigation system that ensures water availability and sustainable usage.
- The type of equipment adopted:
We supplied all equipment required for the project’s pump stations and water transmission pipelines, including high-efficiency water pumps, valve systems, HDPE pipes, flanges, and fittings. Our products ensure that the entire irrigation network runs smoothly, reliably, and efficiently.
Key indicators: Backed by our strong experience in water infrastructure and well-coordinated supply chain, we customized the delivery schedule and configurations based on site requirements and contractor progress. This helped minimize installation risks and ensured timely project advancement.
Achievements/advantages: The project benefits hundreds of smallholder farmers by delivering reliable irrigation water, reducing dependence on seasonal rains, and increasing crop productivity. It enhances food security, raises income levels, and creates new job opportunities. Mlooka stands as a key milestone in Malawi’s rural infrastructure development and agricultural resilience.
Get Your Custom Quote
Our technical experts will analyze your requirements and provide a tailored solution with detailed specifications and competitive pricing.