
Empowering Global Water Solutions
To deliver high-quality, efficient, and sustainable fluid control solutions that empower industries and communities around the world.
Company Introduction
Since 1996, NORITE has focused on the research, development, manufacturing and sales of pumps, valves and intelligent fluid systems, providing cost-effective, stable and reliable system solutions for global water, municipal, energy and industrial projects.
With three modern manufacturing bases in China — located in Henan, Zhejiang, and Anhui — NORITE implements strict quality control processes.
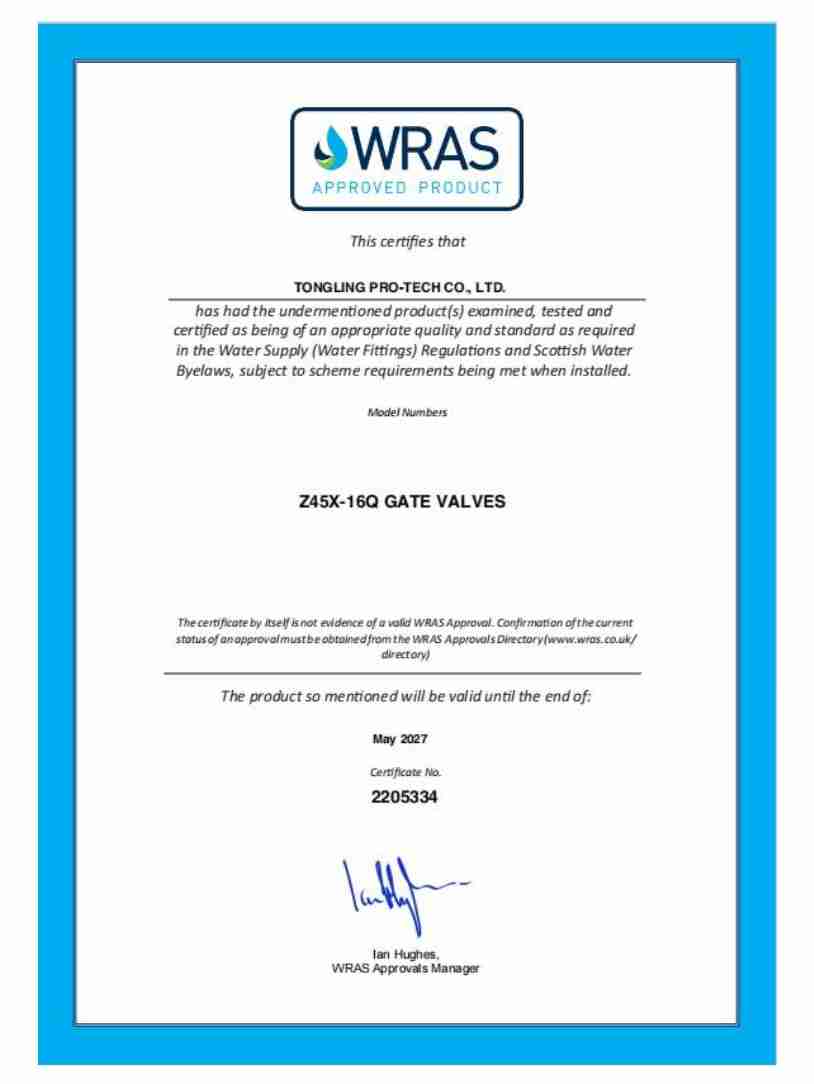
Every product undergoes over 20 rigorous testing procedures, from raw materials to final inspection, ensuring full compliance with GB, ASME, API, DIN, and ISO standards.
Today, our products are exported to more than 60 countries and regions, including Malaysia, Saudi Arabia, Morocco, Colombia, Brazil, and South Africa.
We have established regional offices and long-term partnerships worldwide to provide localized technical support and responsive service.
25+
Years Experience
300+
Projects Completed
10+
Quality Certifications

Our Brand Culture
Built on a foundation of integrity, innovation, and excellence, our culture drives everything we do.

Innovation
We continue to invest in research and development, collaborating with universities and laboratories around the world to achieve technological breakthroughs.

Integrity
Transparent business mechanisms, open cooperation processes, and strict adherence to compliance rules.

Excellence
With customers as the center, all products pass strict testing and factory inspection.
Research & Development Center
Our R&D Center brings together specialists in fluid dynamics, materials science, corrosion resistance, and energy efficiency optimization, ensuring that each product not only meets but exceeds international performance standards.
Our testing laboratory is equipped with state-of-the-art instruments, including:
Spectrometer for material composition analysis
Fatigue testing machine to evaluate product durability under extreme conditions
Flow test bench for hydraulic and performance testing
High-pressure endurance rig for valve pressure verification
Salt spray corrosion chamber for surface protection testing
Every innovation at NORITE is guided by our mission — to deliver smarter, safer, and more sustainable fluid control systems for the world.

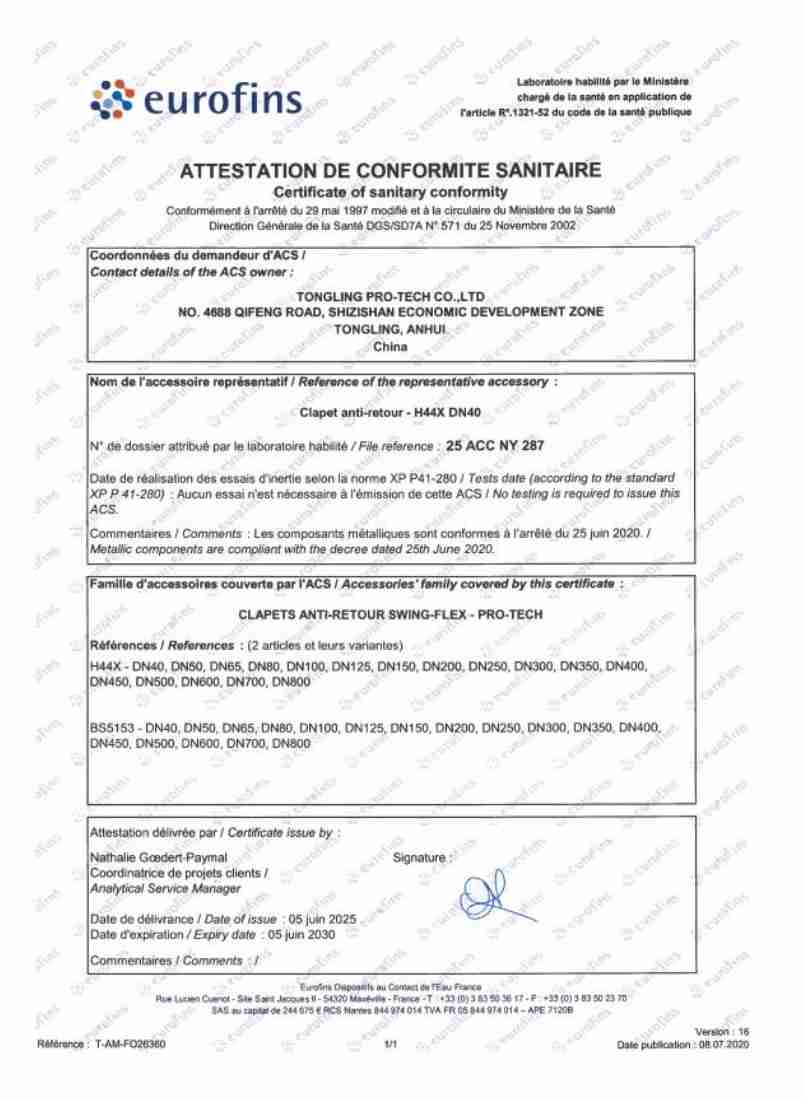
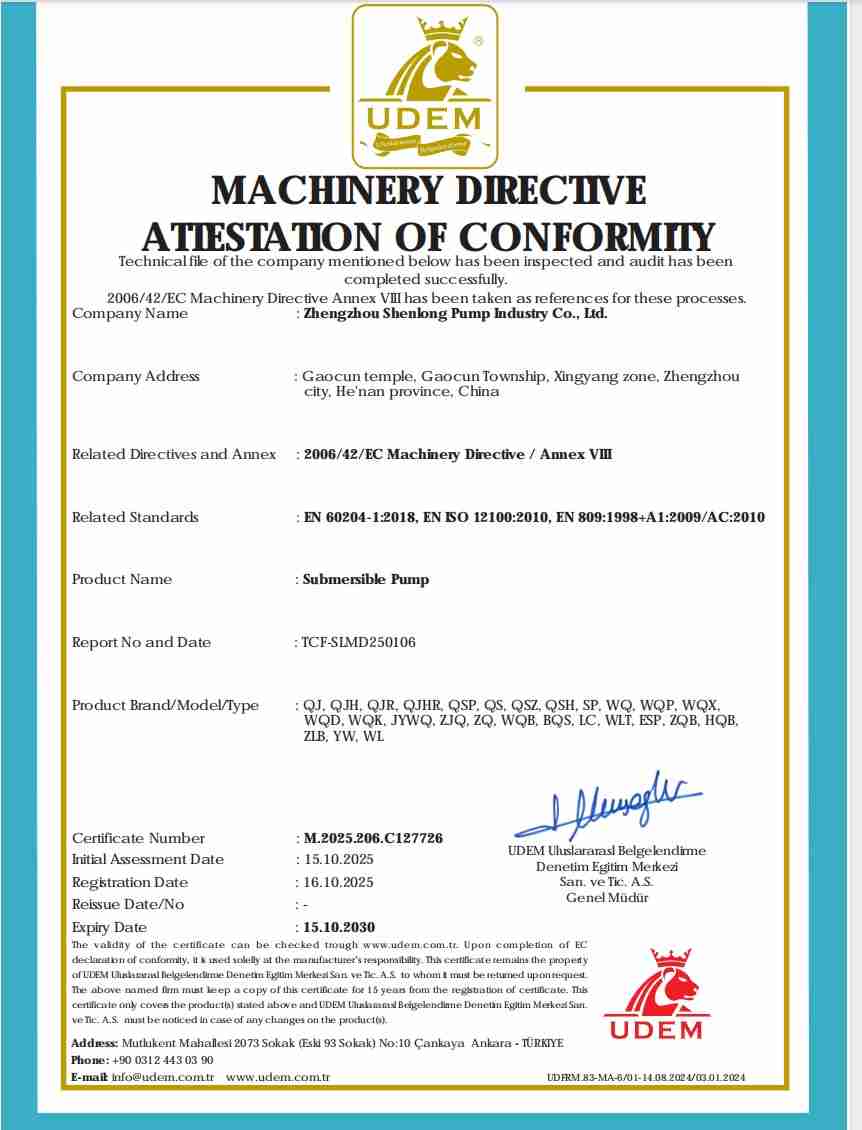
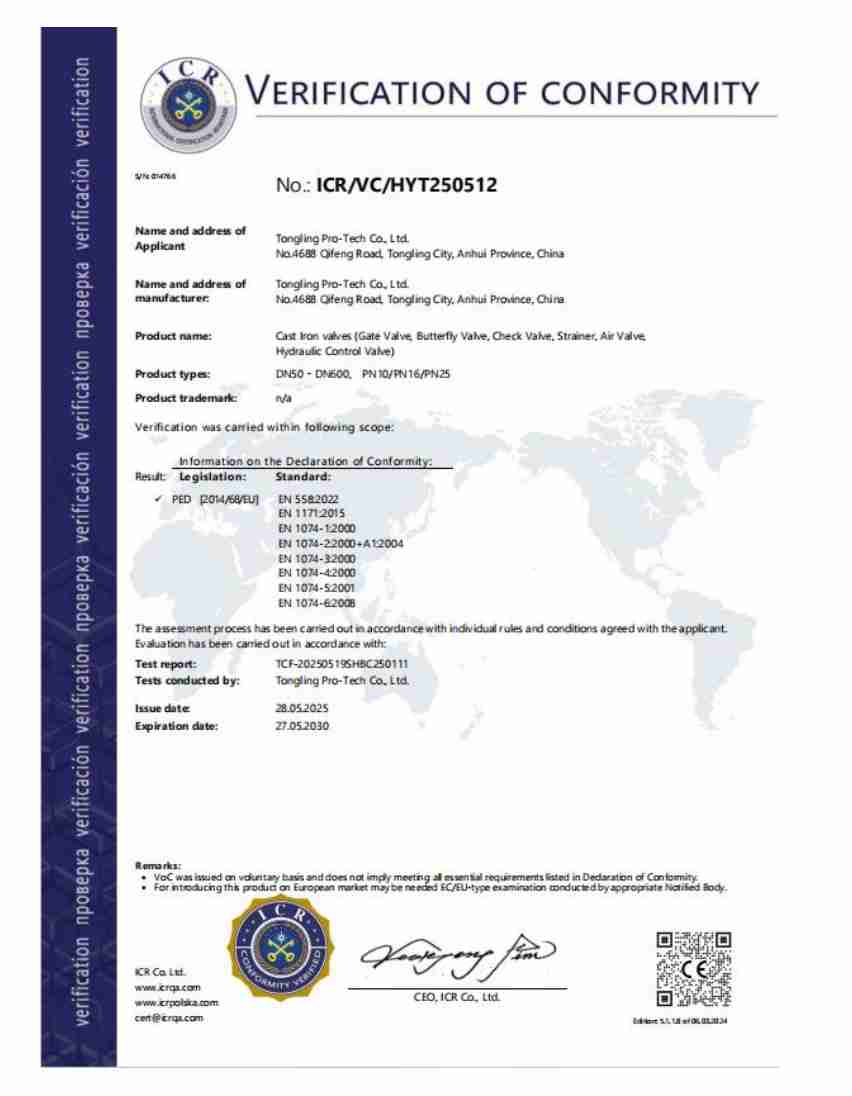
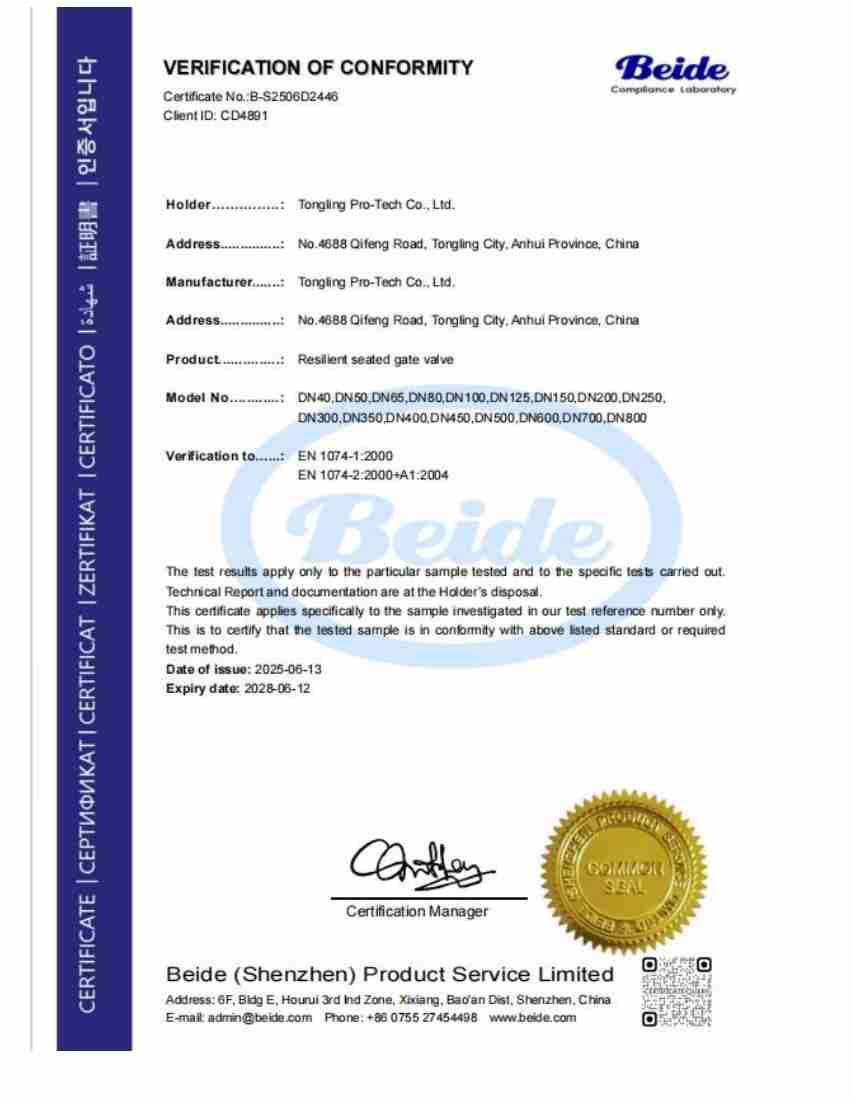
Quality You Can Trust
Every Product. Every Process. Every Test.
Certification



Production Workshop
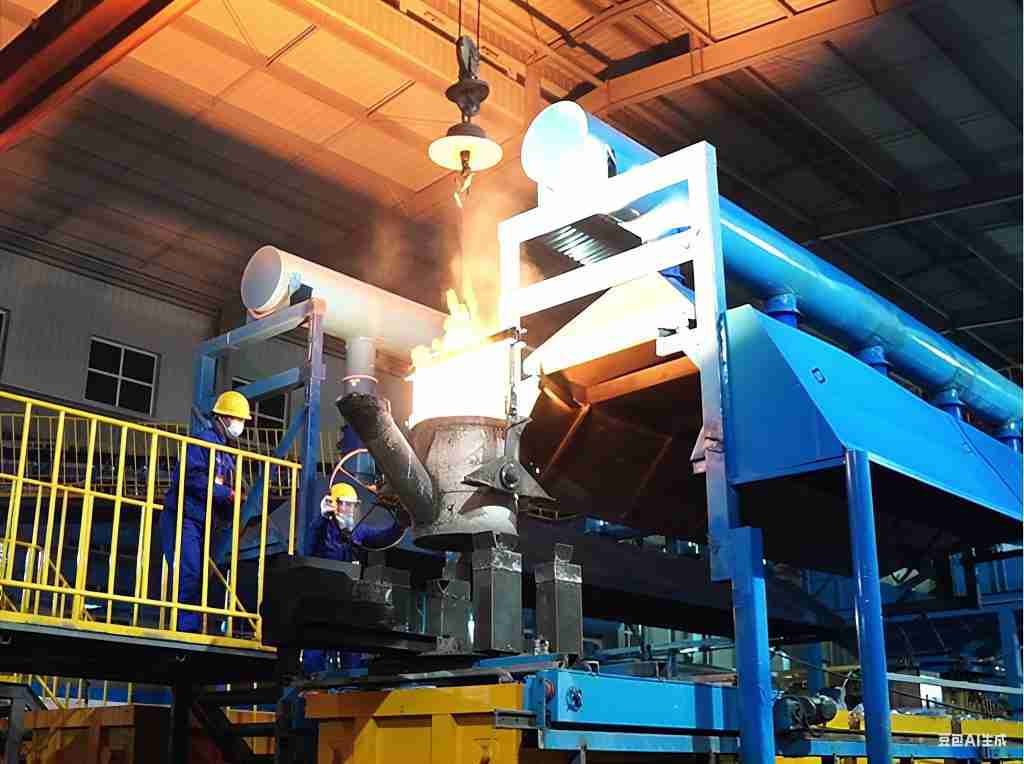
Our modern manufacturing facilities combine advanced automation with skilled craftsmanship.


Efficient Manufacturing · Lean Production · Global Standards
NORITE operates three modern manufacturing bases covering a total area of over 30,000 m², equipped with 8 automated assembly lines and 60+ high-precision CNC machines.
The daily production capacity reaches 1,500 sets of valves and 800 pump units, ensuring a stable supply for large-scale engineering projects and OEM partners worldwide.
We adopt the principles of Lean Manufacturing, integrating digital quality monitoring systems and a MES production management platform to achieve full-process visualization — from raw material inspection, machining, and testing to final assembly and delivery.
Every production step follows the 5S management system, guaranteeing efficiency, safety, and consistency.

Key Manufacturing Capabilities:
- • High-precision CNC machining and automated assembly lines
- • Comprehensive pressure, hydraulic, flow, and corrosion-resistance testing
- • Integrated casting, machining, coating, and final assembly processes
- • Flexible Manufacturing System (FMS) for rapid customization and production response

Sustainability & Safety Culture
- • NORITE adheres to the philosophy of green manufacturing.
- • All factories have passed environmental assessment and certification.
- • We utilize a recycled water system and low-carbon emission processes.
- • We prioritize employee development, establish a comprehensive training system, and establish safe operating standards.
- • We strive for a harmonious coexistence among people, the environment, and our equipment.
Our Services
NORITE products and partners span across Asia, the Middle East, Africa, and Latin America.
Through our global supply chain and technical support teams, we provide seamless communication, localized service, and quick response for every project.

Custom Engineering
Tailored valve and pump solutions designed to meet your specific application requirements.
- • Application analysis
- • Custom design services
- • Prototype development
- • Performance optimization

Manufacturing
High-quality production services with flexible capacity to meet your volume requirements.
- • Small to large batch production
- • Quality assurance
- • Just-in-time delivery
- • Supply chain management

Technical Support
Expert technical assistance and maintenance services to ensure optimal performance.
- • Installation guidance
- • Maintenance programs
- • Troubleshooting support
- • Training services

Global Distribution
Worldwide shipping and logistics support to deliver products wherever you need them.
- • International shipping
- • Customs documentation
- • Local distributor network
- • Inventory management

Testing & Validation
Comprehensive testing services to ensure products meet all specifications and standards.
- • Performance testing
- • Material certification
- • Compliance verification
- • Third-party validation

Consulting Services
Expert consultation to help optimize your fluid handling systems and processes.
- • System optimization
- • Energy efficiency analysis
- • Upgrade recommendations
- • Cost reduction strategies
Our Commitment
Behind every project stands the dedication and expertise of the NORITE team.
We work closely with clients, resolve challenges efficiently, and provide full-cycle technical support.
Our goal is not only to deliver products but to build long-term partnerships based on trust and shared success.